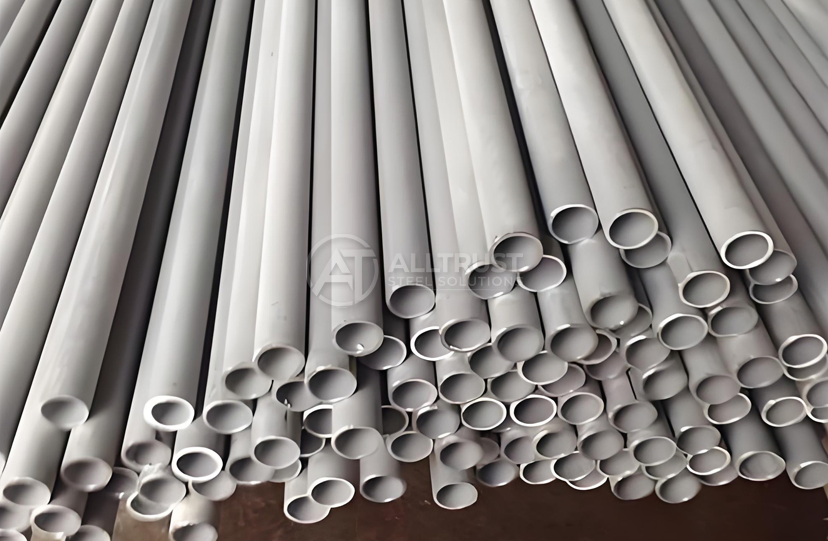
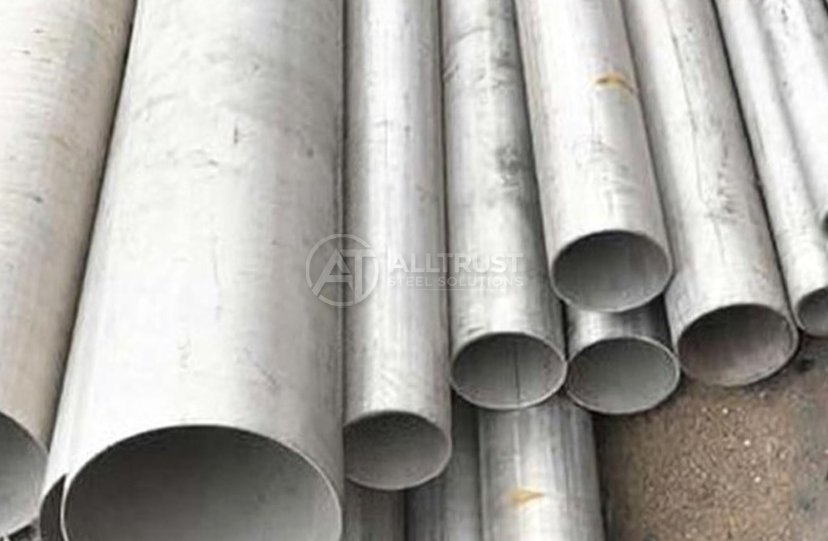
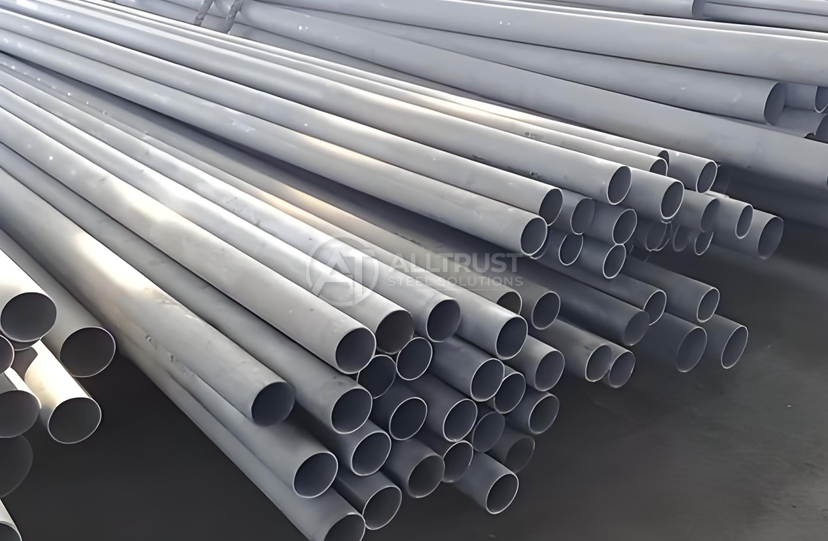
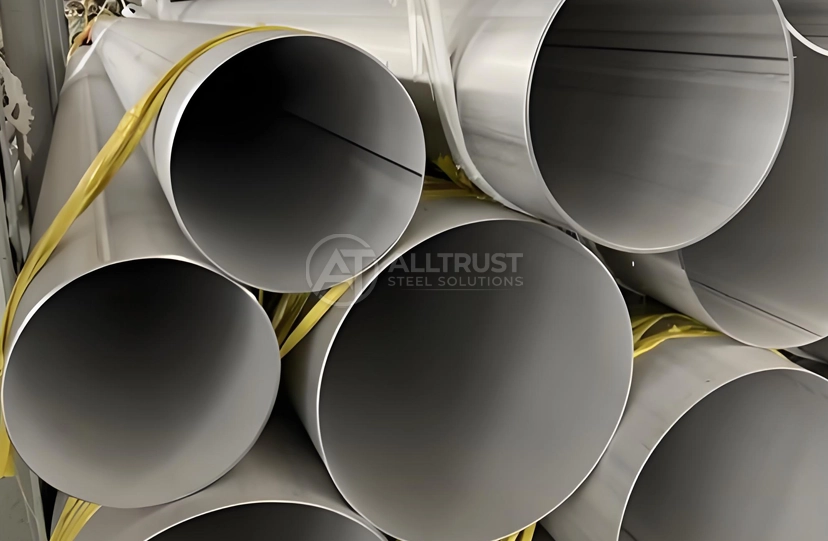
astm a213 boiler tube
2. Standard: ASTM A213 / ASME SA213, specific standard for high-reliability boiler and superheater tubes
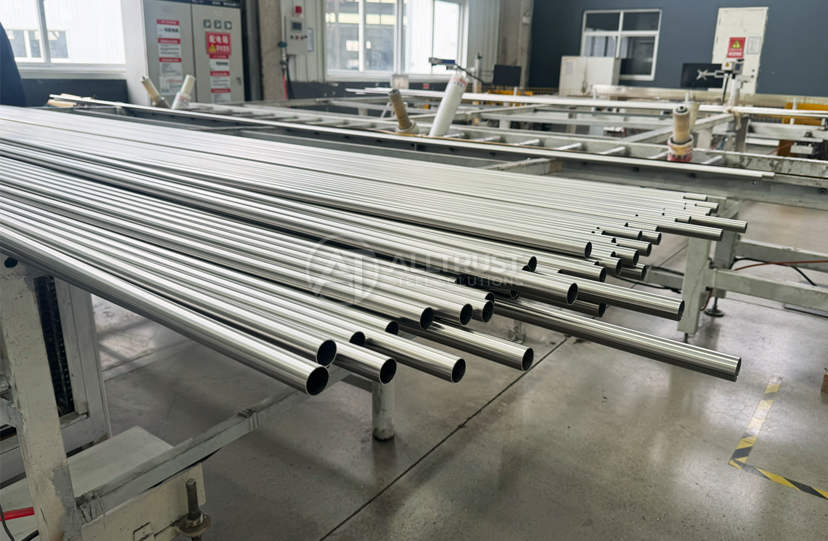
3. Process: 100% solid-billet hot extrusion or cold drawing, ensuring a single-piece structure free of weld lines
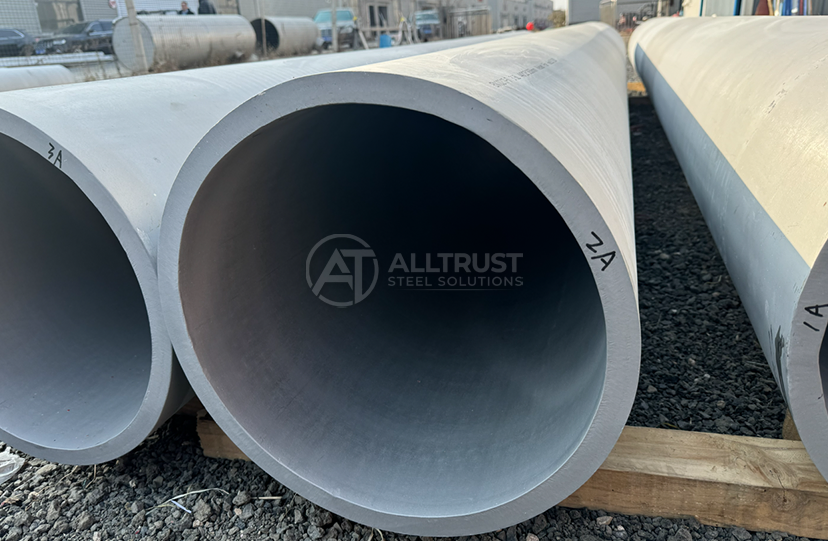
4. Size Range: Custom outer diameters and wall thicknesses matching precise furnace and boiler engineering layouts
5. Heat Treatment: Regulated high-temperature solution annealing to secure optimized grain size for thermal endurance
6. Surface Finish: Thoroughly descaled, acid-pickled, and passivated to maximize heat transfer efficiency inside the furnace
7. Application: Power plant boilers, industrial superheaters, reheater loops, and critical high-pressure steam headers
8. Service Advantage: 100% Hydrostatic and Eddy Current tested, full mill test certificate (MTC EN10204 3.1) provided
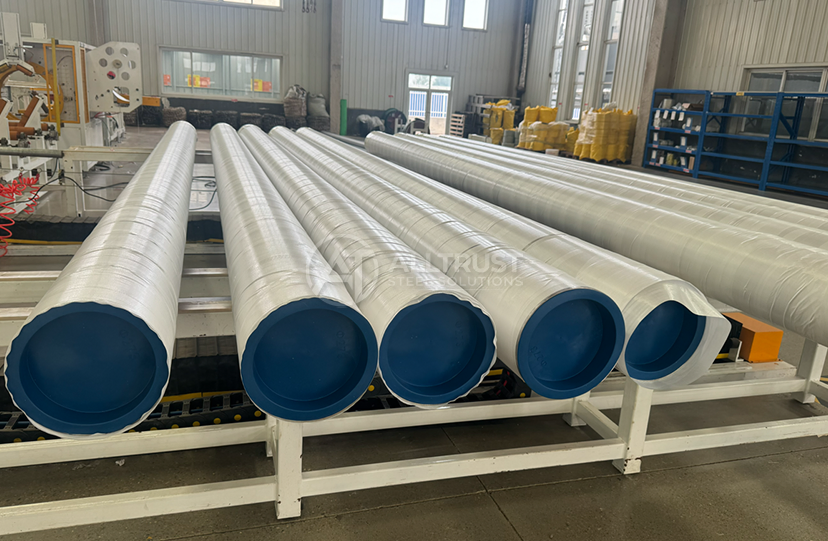
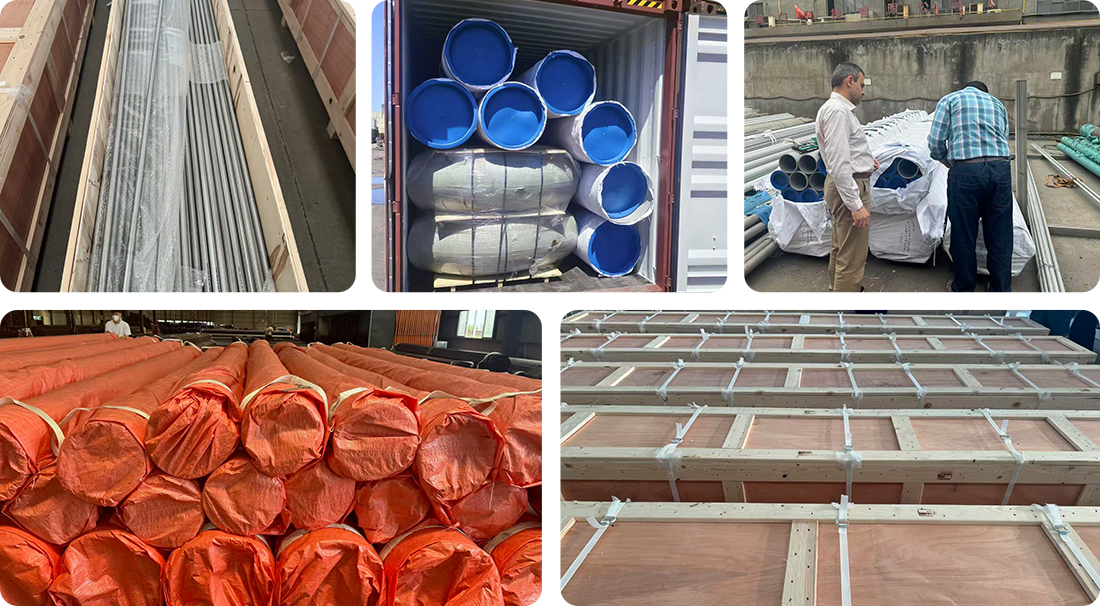
9. Packaging: Securely bundled with strong metal strapping and heavy-duty protective end plugs for ocean transit
10. Key Advantage: Exceptional creep-rupture strength and anti-oxidation performance under continuous high-pressure heating
ASTM A213 Boiler Tube | Seamless Superheater & Heat Exchanger Solution for High-Pressure Steam Systems
Hebei All Trust Steel Co., Ltd manufactures premium astm a213 boiler tube solutions engineered for extreme thermal and mechanical stress environments. We have more than 15,000 tons of yearly manufacturing capacity, and all of our seamless boiler tubes are tested 100% hydraulically. All of our seamless boiler tubes conform to strict ASTM A213/ASME SA213 criteria. Each tube is 100% eddy current tested and mill test certified (EN 10204 3.1/3.2) for proven dependability in power generation, petrochemical processing and industrial heat recovery applications where system integrity is non-negotiable.
Why Choose Our ASTM A213 Boiler Tube for Critical High-Temperature Applications
Power plant operators and process engineers permanently have to deal with thermal stress absorption, steam-side oxidation and lengthy creep deformation. Our seamless tube production minimises the possibility of weld-line failures that might threaten pressure containment.
Hot solid-billet extrusion method yields consistent cross sections of cylinders. This structural uniformity guaranties uniform thermal expansion across the whole boiler network. You save the expense of downtime from premature tube failure.
Each batch of manufacture undergoes a solution annealing procedure at controlled temperatures. This metallurgical procedure optimises the grain size distribution for long-term mechanical performance. Your superheater parts retain dimensional stability over long-term exposure to subcritical and supercritical steam conditions.
Our acid-pickled and passivated surface treatment ensures maximum heat transfer efficiency. Clean interior surfaces avoid the accumulation of scale which lowers heat conductivity and increases localised corrosion.
Complete ASTM A213 Boiler Tube Specifications
| Parameter | Details |
|---|---|
| Standard | ASTM A213 / ASME SA213 / EN 10216-5 |
| Product Type | Seamless Boiler Tube / Superheater Tube / Pressure Tubing |
| Material Grades | TP304 / TP304H / TP304L / TP316 / TP316H / TP316L / TP321 / TP321H / TP347 / TP347H / TP310S |
| Manufacturing Process | Cold Drawn / Cold Rolled / Solution Annealed |
| Outer Diameter (OD) | 1/8" - 5" (3.18 mm - 127 mm) |
| Wall Thickness (WT) | 0.015" - 0.500" (0.38 mm - 12.7 mm) |
| Length | 5.8 m / 6 m / 11.8 m / 12 m / Custom Cut |
| Surface Finish | Solution Annealed & Pickled / Bright Annealed (BA) / Mechanical Polished |
| End Type | Plain End / Square Cut / Burr-Free Cleaned |
| Testing Methods | Eddy Current Test / Ultrasonic Test / Hydrostatic Test / Air Under Water Test |
| Mechanical Testing | Flaring Test / Flattening Test / Flange Test / Hardness Test / Tensile Test / PMI Analysis |
| Third-Party Inspection | SGS / BV / TUV / DNV / ABS Accepted |
| Quality Certificates | EN 10204 3.1 & 3.2 MTC / ISO 9001:2015 |
| Packaging | Plywood Cases / Fumigated Wooden Boxes / Hexagonal Bundles / Waterproof Wrapping |
High-Performance Material Grades for Demanding Steam Environments
Austenitic Stainless Steel Grades
Grades TP304H / TP316H / TP321H / TP347H are highly carbonised for better creep-rupture strength. These ‘H’ grades are significantly superior than the ordinary or low carbon grades in resisting thermal stress deformation if your boiler runs continuously at temperatures over 525°C.
TP304 is a dependable choice for oxidation resistance in moderate temperature superheater areas. This grade is a compromise between economy and sufficient corrosion protection for steam pressures up to 10 MPa.
Molybdenum is added to TP316 to improve pitting resistance in brackish water condensers and coastal power facilities. The alloying element added gives protection against stress corrosion cracking by chlorides.
TP321 and TP347 have titanium or niobium stabilisers. These properties help to avoid intergranular corrosion in heat affected zones after welding and are hence appropriate for manufactured boiler assemblies.
Low-Alloy Ferritic Steel Options
Though our primary focus is austenitic grades, we coordinate supply of T11, T22, and T91 ferritic grades for specific high-temperature applications requiring different thermal expansion characteristics.
Critical Applications Where Reliability Cannot Be Compromised
Supercritical Power Plants
Your superheater and reheater sections demand materials that maintain mechanical integrity under continuous steam temperatures reaching 620°C. Our astm a213 boiler tube solutions in Grade TP347H deliver the creep resistance necessary for these extreme operating parameters.
The seamless structure prevents longitudinal stress concentration points. This manufacturing advantage translates directly into extended service intervals and reduced maintenance costs.
Petrochemical Refineries
Tubes for heat exchanger bundles treating volatile hydrocarbons must have resistance to hydrogen attack and sulfidation concurrently. TP316L grades provide you the corrosion barrier you require, without sacrificing thermal conductivity.
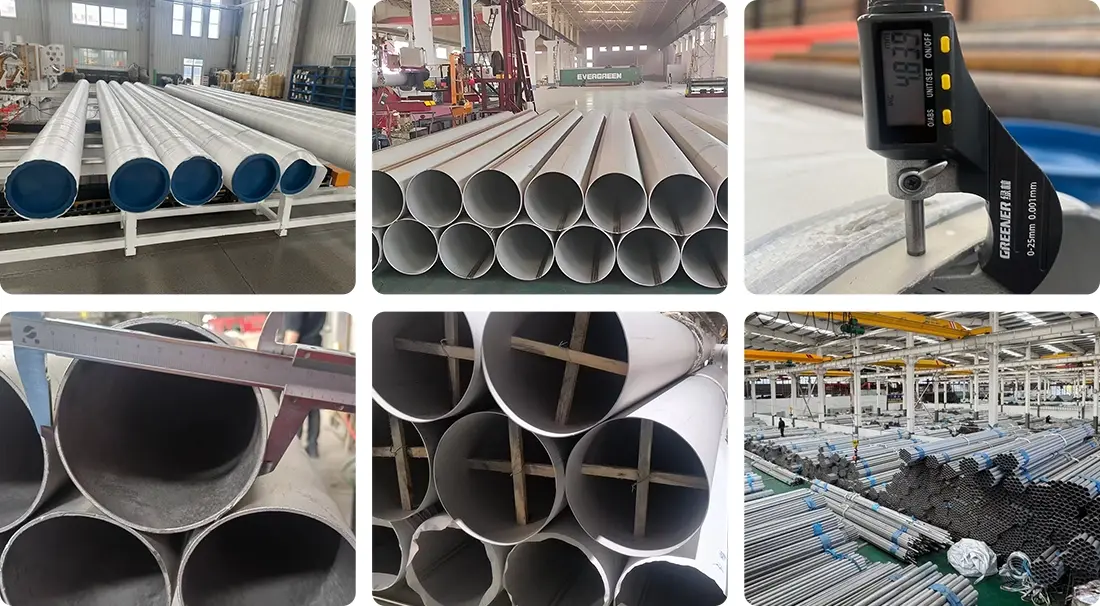
We cold-draw to a precision that yields wall thickness tolerances of ±0.05 mm. This dimensional precision provides for correct tube-to-tubesheet rolling and leak-free junctions throughout your heat recovery network.
Industrial Heat Recovery Steam Generators
HRSG installations face thermal cycling that accelerates fatigue failures in inferior materials. The regulated solution annealing treatment we apply creates a stable microstructure that absorbs repeated thermal shock.
You benefit from predictable performance across thousands of heating-cooling cycles. Your waste heat recovery system maintains efficiency targets without unplanned shutdowns.
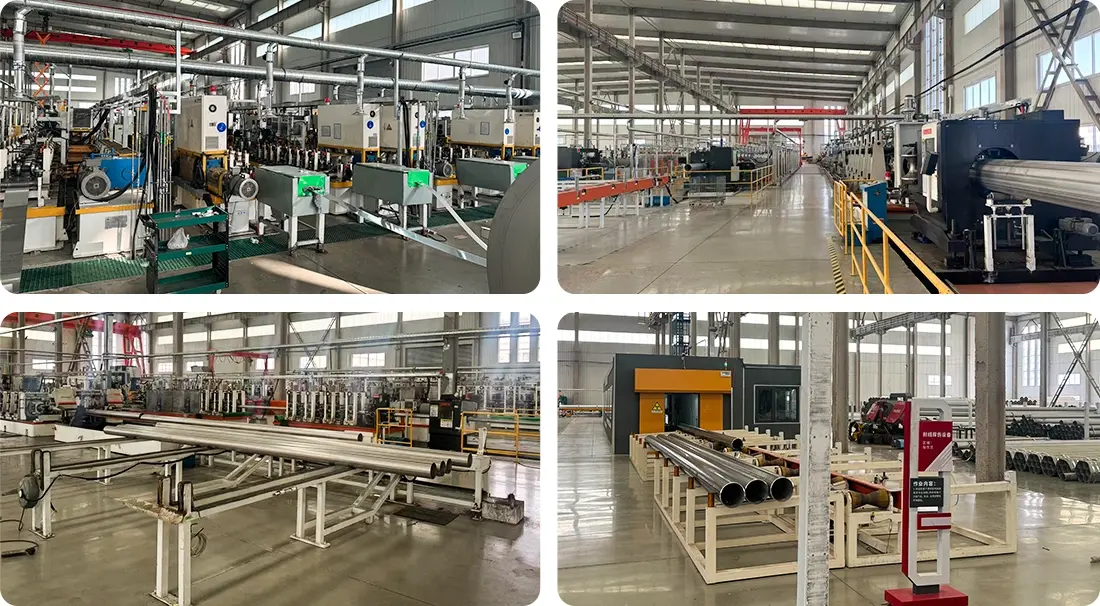
Comprehensive Testing Protocols Guarantee Zero-Defect Performance
Non-Destructive Examination
Eddy Current Testing finds longitudinal and transverse surface defects of 0.3 mm. This automated inspection system performs at production speeds while maintaining the sensitivity requirements of the ASME regulations.
Ultrasonic Testing identifies internal discontinuities that could propagate under cyclic stress. Every tube above 25 mm outer diameter receives full-body UT examination before shipment.
Hydrostatic Testing proves pressure containment capability at 1.5 times your design working pressure. This destructive pressure proof test eliminates weak specimens before installation.
Mechanical Property Verification
Flaring Tests expand tube ends to specified diameters, confirming ductility and freedom from concealed cracks. This validation is particularly critical for tubes destined for roller expansion joints.
Flattening Tests compress tube sections between parallel plates, demonstrating adequate plasticity without splitting. You receive material capable of withstanding installation stresses without brittle failure.
Hardness Testing (Rockwell or Brinell) verifies proper heat treatment completion. Results within specified ranges indicate correct grain structure formation for long-term creep resistance.
Customization Capabilities Tailored to Your Engineering Requirements
Dimensional Flexibility
We manufacture tubes matching your exact furnace and boiler layouts. Custom outer diameters, wall thicknesses, and fixed-length cutting eliminate field modifications that compromise material integrity.
Standard nominal sizes stock immediately for quick turnaround. Specialized dimensions enter production within 15-20 days through our priority scheduling system.
Surface Finish Options
Bright Annealed (BA) finishes provide mirror-smooth internal surfaces for applications where flow resistance must be minimized. The reduced surface roughness improves steam velocity distribution.
Mechanical Polishing achieves specified Ra values for critical heat transfer zones. Controlled surface texture enhances nucleate boiling efficiency in evaporator sections.
End Preparation Services
The multi-pass welded joints are precisely bevelled as per ASME B16.25. Our CNC machining centres can hold compound angles to ±0.5°, simplifying your manufacturing process.
Square-cut plain ends receive thorough deburring and cleaning. You avoid contamination issues during installation and commission hydrostatic testing.
Secure Global Logistics and Professional Technical Support
Our export packing solution is designed to preserve your investment throughout international transportation. Heavy quality waterproof wrapping and plastic end protectors prevent surface damage and moisture penetration, while fumigation-free timber containers are used.
Flexible logistics routeing is possible via strategic shipping from the ports of Shanghai, Ningbo, Tianjin and Qingdao. We can provide FOB, CFR, CIF and DDP terms according on your purchase desire.
Technical support extends throughout your project lifecycle. Our engineering team provides material selection guidance, corrosion resistance analysis, and container loading optimization to maximize shipping efficiency.
FAQ
Q:What core thermal capabilities make this product critical for steam generation infrastructure?
A:This tube carries specialized high-temperature credentials, yielding outstanding mechanical creep rupture strength and reliable thermal stress absorption inside extreme subcritical and supercritical boiler environments.
Q:Why is a seamless structure mandated for this severe utility pressure line?
A:The seamless piercing process provides a completely uniform cylinder cross-section free of weld vulnerabilities, ensuring uniform thermal expansion and preventing sudden mechanical rupture under intensive heat loops.
Q:What destructive quality verification benchmarks must this boiler tube batch successfully pass?
A:Representative production coupons are subjected to severe mechanical flattening trials, cross-sectional flare expansions, and precise Positive Material Identification (PMI) chemical grade verification.
Q:Can this boiler tube series be customized with specialized edge configurations for multi-pass joints?
A:Yes, we support extensive custom fabrication options, offering precision compound angles and beveled endings according to ASME B16.25 codes alongside fixed random length structures.
Q:What material documentation is provided to verify the precise material traceability of this grade?
A:Each batch is accompanied by an EN 10204 3.1 Mill Test Certificate (MTC) detailing the exact chemical ladle heat numbers, grain size configurations, and physical load values.
Contact Us
Ready to enhance your boiler reliability with proven astm a213 boiler tube performance? Contact our technical sales team at info@hballtrust.com for customized specifications, competitive quotations, and rapid delivery scheduling.