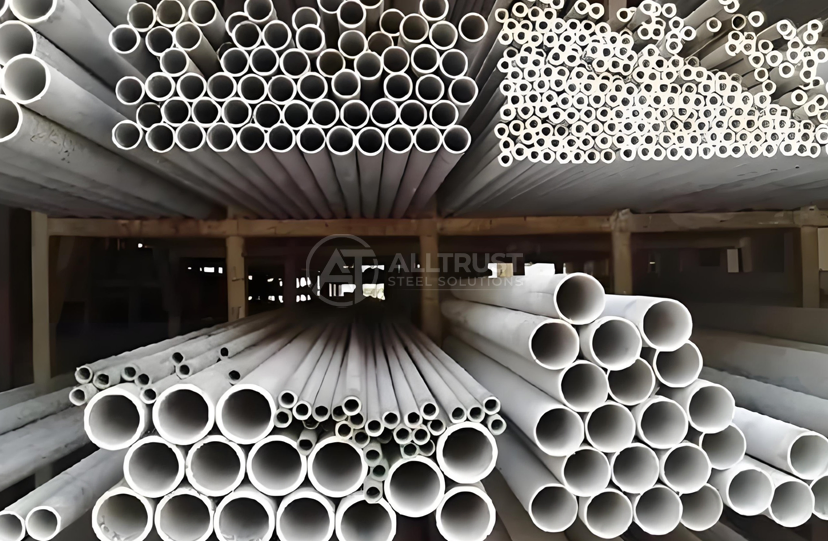
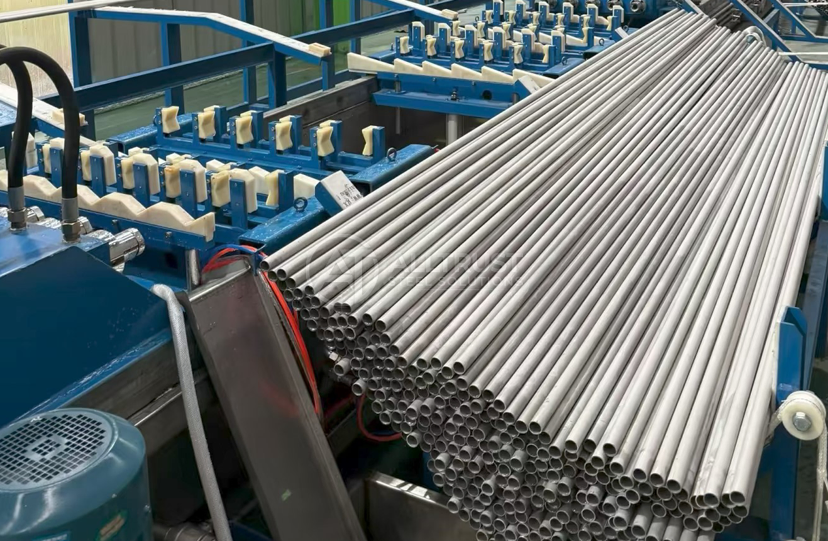
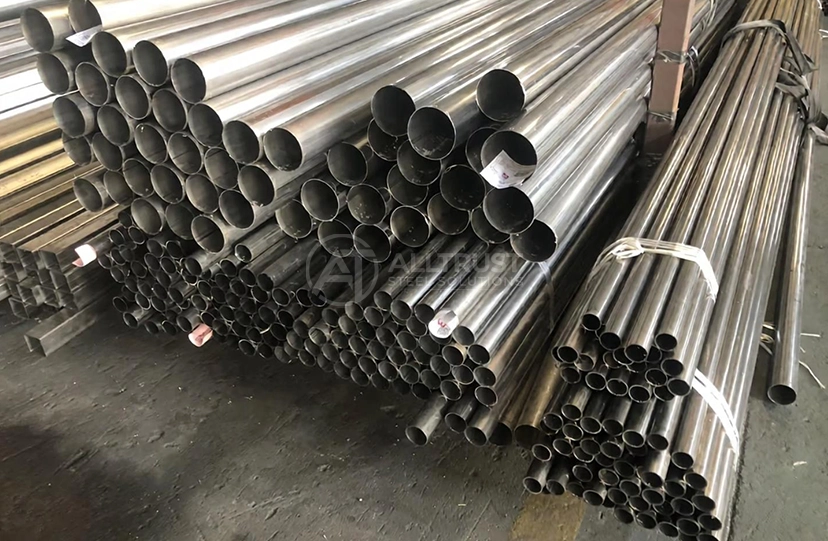
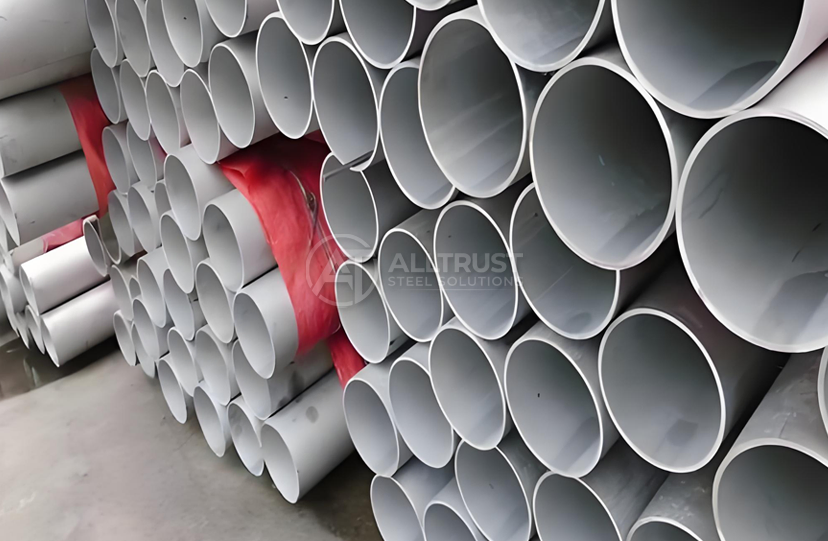
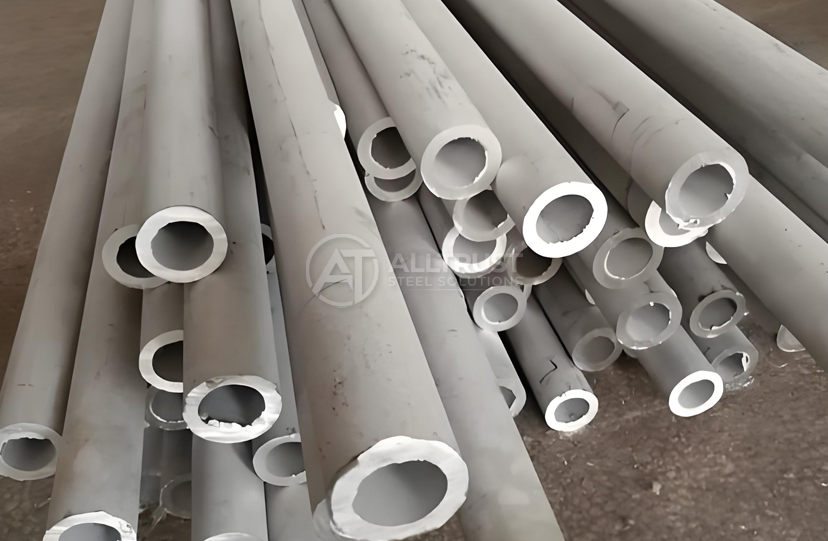
astm a358 efw pipe
2. Standard: ASTM A358 / ASME SA358, the definitive international standard for heavy-duty electric-fusion-welded piping
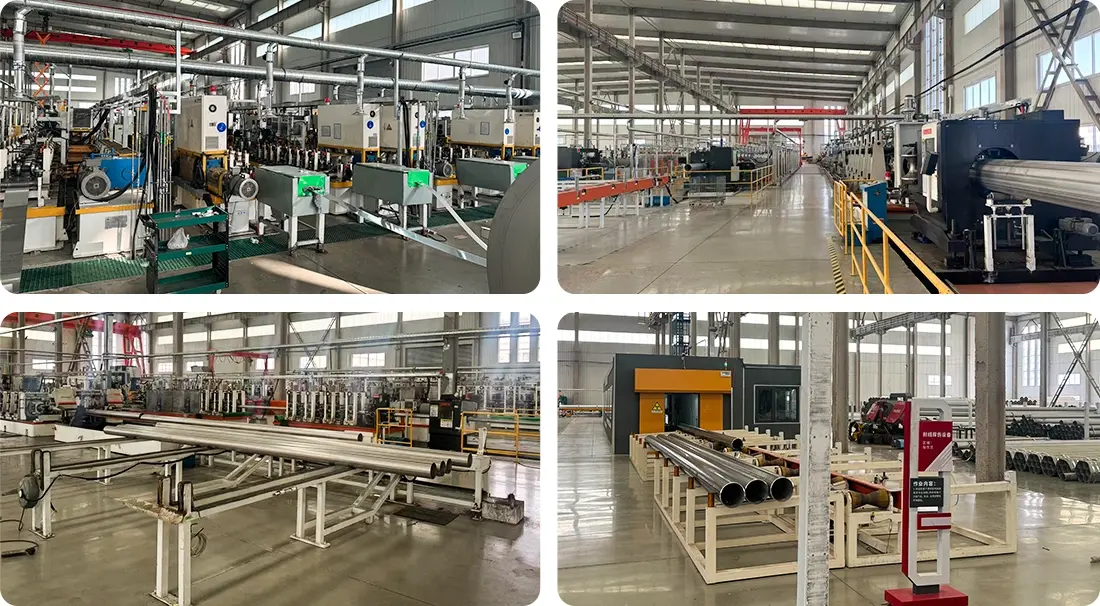
3. Process: 100% automated Electric Fusion Welded (EFW) utilizing premium calibrated plates and double-sided multi-pass joints
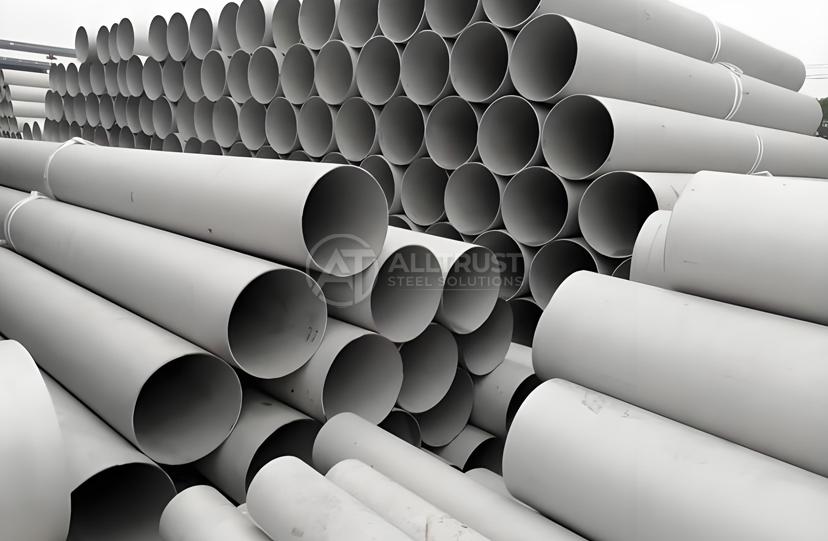
4. Size Range: Large scale sizes from 8" up to 60" Outside Diameter with fully customizable wall thickness schedules
5. Heat Treatment: Post-weld global solution annealing in a continuous furnace to achieve complete microstructure normalization
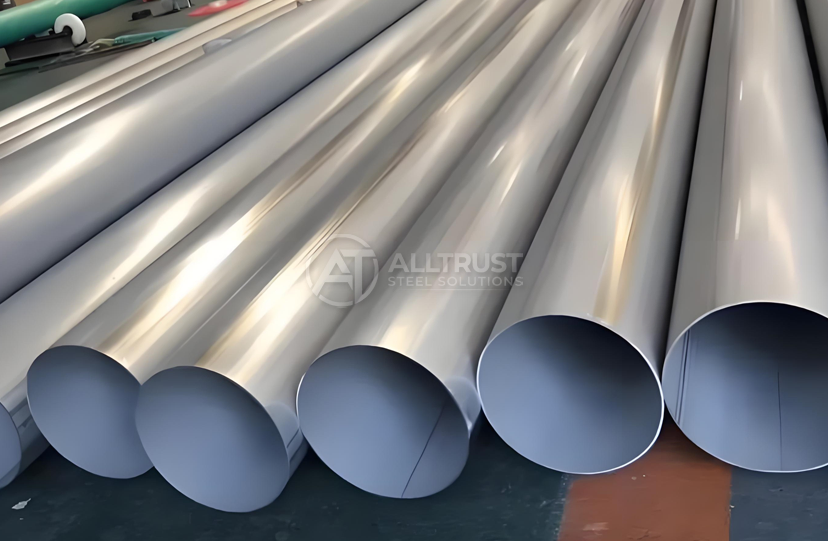
6. Surface Finish: Clean solution annealed and pickled (SA&P), descaled industrial matte, or passivated clean profile
7. Application: High-capacity chemical process lines, industrial fluid transit mains, cooling water loops, and refinery networks
8. Service Advantage: Radiographic examination (RT) compliant with ASME Section VIII Class 1 to Class 5, full traceability provided
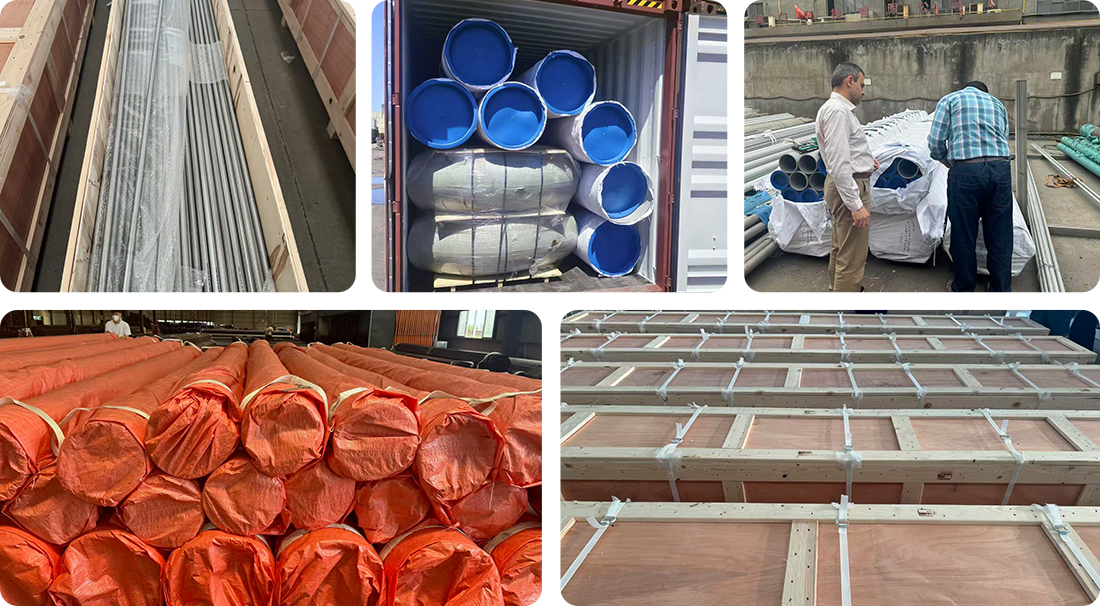
9. Packaging: Bulk loaded with protective bulkheads, heavy-duty nylon lifting slings, or sturdy steel cradle frameworks
10. Key Advantage: Offers outstanding dimensional roundness and exact tolerances, serving as a highly trusted project-saver for mega pipelines
ASTM A358 EFW Pipe | Heavy-Duty Electric Fusion Welded Stainless Steel Pipe for High-Pressure Industrial Applications
Hebei All Trust Steel Co., Ltd specializes in manufacturing astm a358 efw pipe designed for demanding industrial environments requiring superior corrosion resistance and pressure integrity. We provide big diameter pipe systems from 8" to 60"OD with a yearly capacity of over 15,000 tons, all with 100% radiographic testing compliance and complete ASME Section VIII traceability. Each pipe is solution annealed at regulated temperatures post-welding and is thoroughly hydrostatically tested to assure zero-leakage performance. Our electric fusion welded systems are certified to EN 10204 3.1/3.2 standards and have precise wall thickness tolerances of ±0.05 mm. They provide dependable solutions for petrochemical refineries, power generating plants and water treatment facilities across the globe.
Understanding ASTM A358 EFW Pipe Technology
Electric fusion welding is a state-of-the-art production process particularly developed for big diameter stainless steel pressure pipes. Unlike simple welded tubes, automated filler metal is added along the longitudinal seams providing joints that are equal to or stronger than the base metal.
The product specification is tackling the essential difficulties of industry. Beyond 12-inch diameters, seamless pipes become prohibitively costly and technically challenging to fabricate. Standard ERW tube does not have the structural integrity needed for high pressure applications.
This standard is a wonderful fit for that gap. It has 5 separate classes starting from Class 1 which demands 100% radiography inspection to Class 5 for typical applications. This enables engineers to optimise the cost vs performance dependent on the particular project.
Uniform wall thickness distribution throughout the whole circumference is an advantage to your facility. Electric fusion welding allows control of heat input to minimise distortion and retain the metallurgical characteristics necessary for corrosive service conditions.
Core Technical Specifications
| Parameter | Specification Details |
|---|---|
| Manufacturing Standard | ASTM A358 / ASME SA358 / EN 10217-7 |
| Pipe Type | Electric-Fusion-Welded (EFW) Longitudinal Seam |
| Material Grades | TP304, TP304L, TP316, TP316L, TP321, TP347, TP310S |
| Outer Diameter Range | 8" – 60" (219.1 mm – 1524 mm) |
| Wall Thickness | SCH 5S to SCH 80S (2.0 mm – 50 mm) |
| Standard Lengths | 5.8 m / 6 m / 11.8 m / 12 m / Custom Cut |
| Welding Process | Automatic Multi-Pass EFW with Filler Metal |
| Heat Treatment | Solution Annealing (1900°F) + Rapid Quench |
| Surface Finish | Solution Annealed & Pickled / Passivated / As-Welded |
| End Configuration | Plain End / Beveled End / Flanged / Threaded |
| Testing Methods | 100% RT / Hydrostatic / UT / Guided-Bend / PMI |
| Quality Certificates | EN 10204 3.1 & 3.2 MTC / ISO 9001:2015 |
| Joint Efficiency | Class 1: 1.0 / Class 2: 0.85 |
| Tensile Strength | ≥515 MPa (Grade 304) |
| Yield Strength | ≥205 MPa (Grade 304) |
Why Choose Our ASTM A358 EFW Piping Solutions
Superior Metallurgical Integrity
Your operations demand absolute reliability. Our astm a358 efw pipe delivers through precision-controlled welding parameters that produce consistent penetration depth and fusion quality. The automated process eliminates human error while maintaining optimal heat input zones.
Each weld joint receives filler metal addition—a critical distinction from standard welded pipe. This reinforcement ensures the seam achieves mechanical properties equal to or exceeding the parent material. You gain peace of mind knowing failure won't originate at the weld line.
Comprehensive Quality Validation
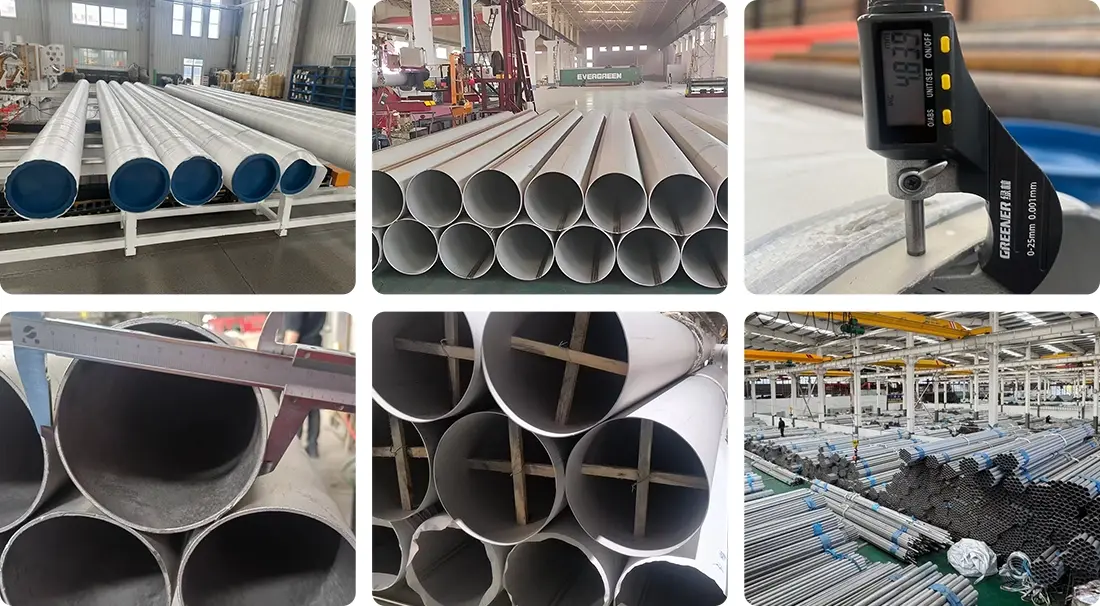
We implement four-stage inspection protocols that exceed standard industry practices. Every production batch undergoes continuous eddy current monitoring during fabrication to detect subsurface anomalies in real-time.
Post-production verification includes macro-etched structural analysis and transverse guided-bend testing. These destructive examinations confirm ductility across the heat-affected zone and weld metal interface.
Radiographic examination follows ASME Section V standards. Our Class 1 pipes receive 100% RT coverage, providing documented proof of internal soundness. You receive detailed RT film records with each shipment for your permanent quality archives.
Advanced Surface Treatment
Corrosion resistance depends heavily on surface condition. Our solution annealing and pickling process removes all heat tint and oxidation scale, exposing fresh chromium-rich surfaces.
The controlled acid bath treatment creates uniform passive film development. This dense chromium-oxide layer actively resists chloride attack, pitting corrosion, and crevice corrosion in marine environments.
For enhanced protection, we offer additional passivation treatments using citric acid or nitric acid solutions. This extra step maximizes the chromium enrichment ratio at the surface boundary.
Flexible Customization Capabilities
Standard catalog sizes don't always align with your engineering drawings. We provide complete dimensional customization including non-standard wall thickness schedules and precise cut lengths matching your installation requirements.
End preparation options include ANSI-standard bevels for butt-welding, precision taper threading (NPT/BSPT), or roll-grooving for mechanical coupling systems. We can incorporate specialized features like laser-cut branch outlets or welded attachment lugs.
Our technical staff will analyse your CAD specifications to optimise material use and minimise field changes. This team approach decreases project cost and saves installation time.
Key Applications of Industrial
Petrochemical Processing Systems
Refineries use astm a358 efw pipe for essential process lines carrying corrosive hydrocarbons, sulfuric acid streams and high temperature catalytic systems. The large diameter capacity meets high-volume throughput needs while preserving pressure integrity.
A smaller diameter option means a higher joint count for your facility. Less connections means less possible places of leakage and less maintenance.
Systems for Seawater Desalination
Desalination facilities are exposed to high chloride concentrations in the intake and brine discharge systems. Our pipe in 316L grade offers excellent resistance to localised pitting and stress corrosion cracking under marine conditions.
This makes effective big scale flow control possible by being able to produce portions of 48 inch and 60 inch in diameter. You get the best hydraulic performance with the least pumping energy cost.
Power Gen Cooling Networks
Both types of power plants use these pipes for circulating cooling water and for the transfer of low pressure steam. The EFW weld has resistance to sustained temperature cycling and vibration exposure typical of turbine applications.
Solution annealed material retains its toughness even at cryogenic settings and is suitable for liquefied gas applications. Your system is reliable in harsh temperature ranges.
Comparing EFW Classes: Finding Your Optimal Solution
The ASTM A358 classification system offers targeted performance levels matched to your application severity:
Class 1 provides maximum assurance through 100% radiography and 1.0 joint efficiency. Choose this for critical high-pressure services where failure consequences are severe.
Class 2 eliminates RT requirements, reducing cost by approximately 15-20% while accepting 0.85 joint efficiency. This works well for moderate-pressure applications with manageable risk profiles.
Class 3 combines selective RT (spot examination) with intermediate joint efficiency. You gain partial quality verification at reduced inspection cost.
Understanding these distinctions helps optimize your procurement budget without compromising safety margins. Our technical team assists with class selection based on your design codes and operating parameters.
Quality Assurance and Testing Protocols
Non-Destructive Examination
In addition to X-ray testing, we also use ultrasonic testing for thick-wall pipelines where RT penetration is restricted. UT scanning finds laminar flaws and determines accurate wall thickness at several locations around the circle.
Dye penetrant testing checks for surface integrity, finding micro-cracks or porosity not seen by eye examination. This is particularly the case with polished finish pipes where surface treatment may hide faults.
Mechanical Property Verification
Transverse tension specimens machined from actual production pipes undergo destructive testing to confirm yield strength, tensile strength, and elongation values. The test coupon includes base metal, weld metal, and heat-affected zones.
Guided-bend testing validates ductility by wrapping specimens around mandrels without cracking. This confirms the weld fusion quality and proper heat treatment effectiveness.
Hardness traverses across the weld zone ensure no localized hard spots that could initiate stress corrosion cracking. We maintain hardness uniformity within specified ranges.
Chemical Composition Analysis
Positive Material Identification (PMI) using X-ray fluorescence analyzers verifies each heat's chemical composition matches specified grade requirements. This prevents material mix-ups that could compromise corrosion resistance.
For L-grade materials, carbon content verification ensures levels stay below 0.030% maximum. This prevents chromium carbide precipitation during welding and subsequent intergranular corrosion susceptibility.
Proper Installation and Handling Considerations
Your piping investment deserves protection during transportation and storage. We package large-diameter sections in heavy-duty steel cradle frameworks that prevent deformation and support the weight distribution.
Plastic end caps seal pipe openings against moisture ingress and debris contamination. Waterproof fiber wrapping protects external surfaces from scratches during handling and loading operations.
Before welding installation, verify matching material grades and perform preheat when required by welding procedures. Maintain interpass temperatures within specified ranges to prevent excessive grain growth.
Post-weld heat treatment requirements vary by grade and wall thickness. Our technical documentation provides specific PWHT guidance aligned with ASME Section VIII and B31.3 code requirements.
FAQ
Q:Why does this electric-fusion welded product yield definitive mechanical advantage over basic welded pipes?
A:This pipe is engineered strictly under heavy pressure vessel codes that integrate continuous automated longitudinal filler-metal added jointing. The process ensures elite structural load ratings and superior pressure containment safety margins. Unlike standard welded tubing, the multiple-pass welding technique with filler reinforcement produces joints that match base metal strength, eliminating the weld seam as a weak point in your system.
Q:What chemical pickling operations are integrated to maximize the service life of this EFW line?
A:The completed pipe body undergoes extensive acid descaling pickling and surface passivation baths. This treatment forms a dense, uniform chromium-oxide protective film that actively thwarts environmental corrosion. The controlled immersion process removes all heat tint and mill scale, exposing fresh stainless steel surfaces with maximized chromium enrichment ratios for optimal corrosion resistance.
Q:What precise inspection procedures verify the structural consistency and safety lines of this EFW batch?
A:Every production batch is verified through continuous online eddy current tracking during fabrication. Additional validation includes laser-micrometer dimensional tracking, high-pressure hydrostatic leak diagnostic testing, and transverse weld tension tests. For Class 1 pipes, 100% radiographic examination documents internal weld quality, providing permanent records of structural integrity.
Q:Can this standard EFW pipe series be customized with specialized end configurations for swift field connection?
A:Yes, we offer flexible machining selections including ANSI-standard tapered bevels for butt-welding applications. Additional options include precision NPT/BSPT taper threading for threaded connections, or specialized roll-grooved structures compatible with mechanical coupling rings. Our fabrication capabilities accommodate flange welding, socket welding ends, and custom branch outlet integration.
Q:Are your astm a358 efw piping lots approved by independent international pressure equipment auditing bodies?
A:Our entire large-diameter line fully adheres to ISO 9001:2015 quality management frameworks and carries CE compliance marking. We welcome independent witness inspections from certified third-party bureaus including SGS, TÜV, BV, DNV, and ABS. Each shipment includes complete EN 10204 3.1 or 3.2 Mill Test Certificates with full material traceability documentation.
Contact Us
Ready to specify high-performance piping for your next project with the astm a358 efw pipe? Contact us at info@hballtrust.com to discuss your specific application needs and receive a comprehensive quotation within 8 hours.