EN 10216-5 1.4404 Tube: Avoiding Grade and Tolerance Mismatches
When purchasing a seamless stainless steel pressure tube for high-pressure or corrosive use, the difference between 1.4404 and a grade that looks the same but is chemically worse can mean the difference between a system lasting decades or failing within months. The EN 10216-5 1.4404 tube, also known as X2CrNiMo17-12-2 or just "316L," is a low-carbon, molybdenum-containing austenitic grade that is controlled by the European standard for pressure-sealed tubes. Not only is it important to get the grade and size tolerances right, but it's also necessary for safe and legal industrial operation.
Understanding EN 10216-5 1.4404 Tube Standards and Specifications
What EN 10216-5 Governs?
The law that says how seamless stainless steel tubes for pressure service must be made is EN 10216-5. It talks about things like the chemicals that make it up, technical tests, size limits, tests that don't damage the object, and how to get qualified. Tubes need to have mill test certificates (MTC) that meet EN 10204 3.1 or 3.2 and be able to be fully traced back to their original heat number. The European Pressure Equipment Directive (PED 2014/68/EU) says that this level should be used as a guide.
Chemical Composition and Mechanical Properties of 1.4404
Grade 1.4404 has no more than 0.03% carbon, 16.5% to 18.5% chromium, 11.0% to 13.0% nickel, 2.0% to 2.5% molybdenum, and no more than 16.5% chromium. This low-carbon ceiling means that carbide can't form at the edges of the grains when the normal 1.4401 version (max 0.07% C) is welded. It's at least 190 MPa (Rp0.2) strong and can stretch at least 45%. It can also be pulled apart at 490–690 MPa.
Dimensional Tolerances and Size Range
Follow the sizes that EN ISO 1127 tells you to. The D3/T3 tolerance class is enough for most situations. The D4/T4 tolerance class is usually what fluid systems that need to be very accurate need. The outside diameter (OD) is between 6 mm and 609.6 mm, and the wall thickness (WT) is between 0.5 mm and 40.0 mm. You can choose from rolls that are 6.0 m or 12.0 m long, or you can have them cut to any length you need. ASTM A312 and EN 10216-5 say that walls shouldn't vary in thickness too much in a negative way. Buyers who are replacing generic drugs made in the United States don't like this.

Common Causes and Risks of Grade and Tolerance Mismatches
Grade Misidentification in the Supply Chain
It looks like 1.4404 is sent more often than 1.4301 (304) or 1.4401 (316). All of these grades look and feel the same, so you don't need to do anyone else's PMI checks on them. The main difference is the amount of carbon and, in the case of 304, the lack of molybdenum. When something is used for one to two years, this change speeds up pitting and intergranular rust in chloride-rich places like desalination plants, offshore bases, and municipal utilities.
Dimensional Tolerance Deviations and Their Consequences
It's hard to join en 10216-5 1.4404 tube welded or flanged joints if the wall thickness changes more than the allowed range. This is because it changes the pressure values. People bought a tube that wasn't up to the D3/T3 standard but only the less strict D2/T2 standard. Due to uneven heat input, this tube has gaps at the sealing faces and weld flaws. It may not pass the hydrostatic test limits. It's important for clean utilities for food and drugs that the internal hole concentricity is good. If it's not, even small out-of-roundness can leave spots where germs can stay.
Real-World Cost of Specification Errors
Remember to check the grade of the thing you buy for the chemical reactor project. If you do not, you might have to fix all the pipes, pay to shut down the process, and file claims against third parties. Problems with materials cause about 25% of unplanned downtime in the industry, according to data from the field. As soon as someone buys something without an EN 10204 3.1 license and independent PMI proof, they will only have a paper record to thank them for it.--- Always ask for an EN 10204 3.1 MTC if you want to ship something. The certificate should have the heat analysis, not just a range. It should also have the heat number that is stamped on each tube. If you want to know the grade standards for carbon, nickel, chromium, and molybdenum, look at EN 10216-5. Things that are being sent to other countries are checked using PMI analysis (optical emission spectroscopy) on a sample from each lot. This gives chemical proof that is different from the other proof.
Best Practices to Avoid Grade and Tolerance Mismatches During Procurement
Verify Chemistry Before Accepting Delivery
Before shipping is approved, you should always ask for an EN 10204 3.1 MTC. The certificate needs to show the real heat analysis, not just a range, and list the heat number that is stamped on each tube. Compare the amounts of chromium, nickel, molybdenum, and carbon to the grade levels in EN 10216-5. For orders going to other countries, PMI analysis (optical emission spectroscopy) on a sample from each lot gives scientific proof that is separate from the others.
Before letting someone get paid, the buying team should do the following main checks:
- Please send me the full MTC (EN 10204 3.1 or 3.2): Make sure that the heat number, chemical analysis, mechanical test results, and hydrostatic test data are all there and can be linked to the correct production lot.
- In the purchase order, be clear about the tolerance class. Write "EN ISO 1127, D3/T3" or "D4/T4" in words. Suppliers can ship to the biggest margin possible and still be officially legal when they use vague measurement wording.
- Need 100% NDT documentation: Eddy current testing finds flaws on the surface and below the surface, and ultrasonic testing (UT) makes sure that the wall thickness is the same along the whole length of the tube.
All of these steps get rid of the main reasons why disputes happen after the goods have been delivered. They also protect the engineering design and the safety case of the end client.
Select Suppliers with Auditable Quality Systems
If a supplier is certified, they should have ISO 9001:2015 and offer free third-party inspection by SGS, BV, TÜV, DNV, or ABS. Ask for proof that intergranular corrosion testing was done according to EN ISO 3651-2 (Method A or C) on every production lot, not just samples taken every so often. A big buying risk comes from suppliers who don't want to share raw NDT records or heat-traceable certificates.
Write Precise Specifications into Every Purchase Order
A big reason for tolerance conflicts is unclear words used for orders. If you want to buy en 10216-5 1.4404 tube, you should be clear about the following: the standard (EN 10216-5), the grade (1.4404 / X2CrNiMo17-12-2), the OD and WT in millimetres, the tolerance class (EN ISO 1127 D4/T4), the surface condition (solution annealed and pickled / CFA, or electro-polished), the end type (plain end or bevelled end), and the certificates you need (EN 10204 3.1, PED compliance).

Comparing 1.4404 with Similar Grades for Correct Selection
1.4404 vs. 1.4401 (316 Standard Carbon)
Chrome, nickel, and molybdenum are all the same amounts in both grades. The only thing that can change is that 1.4401 can have up to 0.07% carbon. As long as it's only used for mechanical things, this difference doesn't matter. It does, though, when parts are welded together. When the carbon level is above 0.03%, the heat from welding makes chromium carbide form around the edges of the grains. That spot is more likely to rust because of this. The word for this is sensitivity. 14.404 is the best metal for welding ducts that are used in government or chemical plants.
1.4404 vs. 1.4435 (Higher Nickel 316L)
One grade, 1.4435, has at least 12.5% nickel, and another grade, 1.4404, has at least 10% nickel. This higher nickel floor makes it less likely that stress corrosion cracks will form in some acidic places. It's also often required by German drug plant rules, such as the EHEDG standards. Both 1.4435 and 1.4404 are "316L," but if you send 1.4404 to someone who wants 1.4435, it might not pass a check by a third-party mill certificate.
1.4404 vs. ASTM 316L (Cross-Standard Equivalence)
You can use 1.4404 instead of UNS S31603 (316L) if you need to follow ASTM A312 or ASTM A269 for a foreign sale. But there are different ranges of sizes. These are the OD/WT schedules that are used by EN 10216-5. The ASTM NPS schedules are based on inches. Everything must be checked in both systems before a buy order is sent. This is very important for projects going to the Middle East or Southeast Asia. If it's not, a lot of extra work that costs a lot of money has to be done.
Technical Support and Maintenance Guidelines for 1.4404 Tubes
Handling and Storage to Prevent Surface Damage
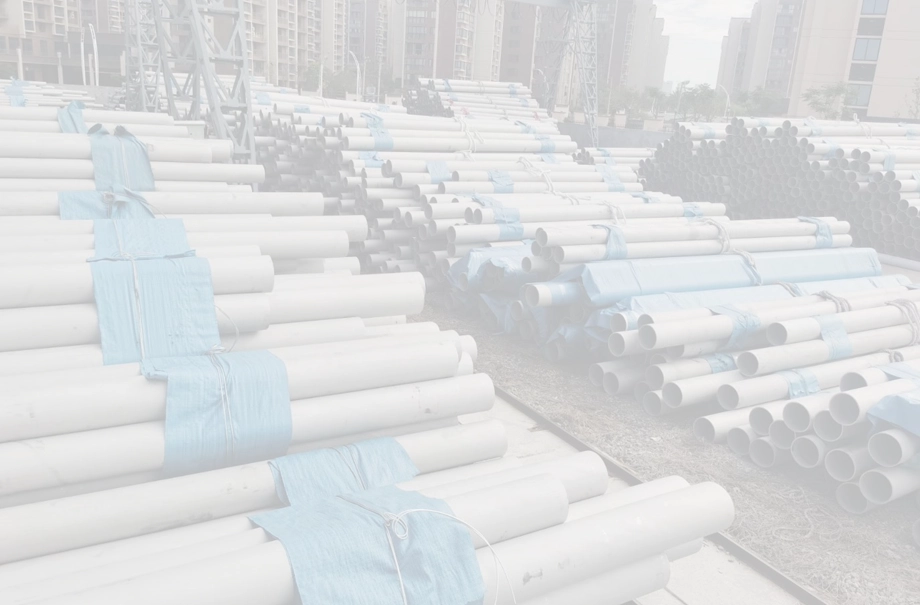
Instead of carbon steel racks, store 1.4404 tubes on rubber-lined racks or saddles that are not made of metal. This will keep the outside from rusting. Any hexagonal ocean bundle will have plastic end caps that need to stay in place until the bundle is put together. You need to pickle the surface again or use a targeted passivation process to fix a scratch that goes below the passive oxide layer. Afterward, it can be used in media that are acidic.
Welding and Heat Treatment Protocols
Because 1.4404 has almost no carbon (less than 0.03%), it's easy to weld in the field. After the join, you usually don't need to heat treat it. Keep the temperature below 150°C between rounds and use 316L filler metal (AWS A5.9 ER316L). Things that are heated to 450°C to 850°C shouldn't be left there for a long time. After tubes are bent or hot-formed, they need to be heated in a kiln to 1,040–1,120°C and then cooled in water. This evens out the microstructure once more, and the tubes will never rust again.
Post-Delivery Inspection and Ongoing Maintenance
Once the tubes have been delivered, check the sizes of 10% of them in each lot against the tolerance class called for in the buy order. Check out what's written on the tubes. Each one needs to have the brand name, the grade (1.4404), the heat number, the standard number (EN 10216-5), and the test type (TC1 or TC2). Look for pits in the tube surfaces in chloride-filled areas once a year with dye-penetrant or eddy current before they turn into through-wall rust.
Conclusion
Avoiding grade and tolerance mismatches when sourcing an en 10216-5 1.4404 tube starts with understanding what EN 10216-5 actually requires — and then building those requirements directly into every purchase order, certificate checklist, and inspection protocol. The chemical gap between 1.4404 and a nominally similar grade is measurable in parts-per-thousand carbon or percentage points of nickel, but the operational gap in corrosive service is the difference between a 20-year asset and a 2-year failure. Rigorous documentation, clear dimensional specifications, and third-party inspection acceptance are the three controls that close this risk entirely.
FAQ
What is the main difference between 1.4401 and 1.4404?
Both grades contain molybdenum, but 1.4404 caps carbon at 0.03% versus 0.07% for 1.4401. This prevents sensitization in welded joints, making 1.4404 the correct choice for welded pipelines in chemical or offshore service.
How do I verify the authenticity of an EN 10216-5 1.4404 tube?
Check the tube marking for the manufacturer's logo, standard reference (EN 10216-5), grade designation (1.4404), heat number, and test category (TC1 or TC2). Cross-reference these against the EN 10204 3.1 MTC. Request PMI analysis if any detail is inconsistent.
What tolerance class should I specify for precision fluid systems?
Specify D4/T4 per EN ISO 1127 for tight outside diameter and wall thickness control. Standard pressure applications typically use D3/T3 as a minimum.
Does EN 10216-5 require impact testing?
For cryogenic service or specific design codes, impact tests at -196°C or -46°C can be specified. The standard itself does not mandate impact testing for all applications; it depends on the design temperature and applicable pressure equipment code.
Can 1.4404 tubes meet both EN 10216-5 and ASTM A312 requirements simultaneously?
Yes, but only if both the chemical composition and dimensional requirements of each standard are explicitly stated in the purchase order. Chemical equivalence exists (UNS S31603), but dimensional systems differ between metric EN and inch-based ASTM.
Get Certified EN 10216-5 1.4404 Tube from All Trust Steel— Request a Quote Today
Molybdenum is in both grades, but 1.4401 has a carbon cap of 0.07% and en 10216-5 1.4404 tube has a carbon cap of 0.03%. For chemical or offshore service, 1.4404 is the best metal for welded pipelines because it keeps the joints from becoming weak. Contact our technical team at info@hballtrust.com or visit hballtrust.com to request a quote or download our specification guide today.
References
1. European Committee for Standardization. EN 10216-5: Seamless Steel Tubes for Pressure Purposes — Technical Delivery Conditions — Part 5: Stainless Steel Tubes. CEN, 2021.
2. European Committee for Standardization. EN 10204: Metallic Products — Types of Inspection Documents. CEN, 2004.
3. ASTM International. ASTM A312/A312M: Standard Specification for Seamless, Welded, and Heavily Cold Worked Austenitic stainless steel pipes. ASTM, 2022.
4. International Organization for Standardization. EN ISO 1127: Stainless Steel Tubes — Dimensions, Tolerances and Conventional Masses per Unit Length. ISO, 1996.
5. International Organization for Standardization. ISO 3651-2: Determination of Resistance to Intergranular Corrosion of Stainless Steels — Part 2: Ferritic, Austenitic and Ferritic-Austenitic (Duplex) Stainless Steels. ISO, 1998.
6. European Parliament and Council. Directive 2014/68/EU on the Harmonisation of the Laws of the Member States Relating to the Making Available on the Market of Pressure Equipment (PED). Official Journal of the European Union, 2014.