TP316L Stainless Steel Pipe Manufacturer for Pharmaceutical and Hygienic Fluid Systems
When a pharmaceutical plant specifies piping for a high-purity water loop or a sterile product transfer line, the margin for error is essentially zero. A single contaminated weld or an incorrectly graded alloy can trigger a product recall, a regulatory shutdown, or worse. That is why procurement engineers across the chemical, biotech, and food processing sectors consistently specify TP316L stainless steel pipe — and why choosing the right manufacturer matters just as much as choosing the right material.
Understanding TP316L Stainless Steel Pipes for Pharmaceutical Applications
What Makes TP316L Distinct at the Molecular Level?
TP316L (UNS S31603 / 1.4404) is a chromium-nickel-molybdenum metal with very little carbon. Its unique feature is its carbon ceiling of 0.03% max. This stops carbide precipitation at grain boundaries during welding, which gets rid of sensitization and post-weld intergranular corrosion without the need for solution annealing after fabrication. Adding 2–3% molybdenum makes the material much more resistant to chloride-induced pitting, which is very important in Clean-In-Place (CIP) and Steam-In-Place (SIP) pharmaceutical environments.
Mechanical Properties That Support Pressure-Bearing Service
An ASTM A312 or ASME SA312 pipe must have a tensile strength of at least 485 MPa (70 ksi) and a yield strength of at least 170 MPa (25 ksi). These numbers stay the same for all sizes, from NPS 1/8" thin-wall tubing to NPS 48" heavy-schedule pipe, as long as the material has been solution-annealed correctly at 1040°C–1150°C and quickly quenched to lock the alloy structure.
Regulatory Compliance Standards Procurement Teams Must Verify
Pharmaceutical piping has to meet a lot of different requirements. Any reliable manufacturer should give you EN 10204 3.1 Mill Test Certificates (MTC) that show the chemical composition and mechanical properties that have been tracked over time using heat. The quality management system is governed by ISO 9001:2015 approval. Pressure-bearing parts sold in controlled markets are covered by the Pressure Equipment Directive (PED) and CE marking. FDA material traceability and GMP process documents give projects that will be seen in the U.S. the audit record that quality assurance teams need.


Comparing TP316L with Other Stainless Steel Grades for Hygienic Fluid Systems
TP316L vs. TP304 and TP304L
TP304 and TP304L don't have any molybdenum in them, so they are cheap for general-purpose uses but can't be used in places with a lot of chloride, like salty process streams or coastal utility water. When chloride levels are above 50 parts per million, TP316L always does better than TP304L in accelerated pitting corrosion tests. The molybdenum content in TP316L is a must for pharmaceutical bulk fluid transfer and WFI (water for injection) distribution loops; it's not an optional extra.
TP316L vs. Standard TP316
The standard TP316 grade and tp316l stainless steel pipe have almost the same corrosion resistance in service, but TP316 has up to 0.08% carbon in it. When welded parts are heated several times between 425°C and 815°C (the sensitization range), TP316 can form chromium carbide along the edges of the grains. This makes the area less resistant to corrosion. Because TP316L has very little carbon, this risk is completely eliminated, making it the best grade for any system that uses orbital welding or multiple-pass field welds.
Seamless vs. Welded: Choosing the Right Product Form
TP316L pipes that are seamless (hot-pierced or cold-drawn) and welded (automatic longitudinal seam) both meet ASTM A312, but they are more or less the same in terms of cost and performance. Seamless pipes don't have any weld seams, so they have the most uniform structure for use in high-pressure or vibration-heavy situations. Welded pipes made with 100% eddy current testing are a cheaper way to make sure that lower-pressure sewage lines are properly sealed. When engineers design pharmaceutical pipes, they usually choose seamless pipes for important process lines and welded pipes for utility and waste systems.

How to Choose the Right TP316L Stainless Steel Pipe Manufacturer?
Certifications and Documentation That Cannot Be Waived
Before you approve a supplier, you must check four documents that are not up for discussion: EN 10204 3.1 MTC with full heat traceability; ISO 9001:2015 scope certification; PMI (Positive Material Identification) reports that confirm the Mo and Ni content; and ASTM A262 Practice E (Strauss Test) results that confirm the intergranular corrosion resistance. When these documents are asked for by a pharmaceutical qualification program, suppliers who can't provide them pose an unquantifiable risk.
Production Capabilities and Quality Control Infrastructure
The OD should be between 1/4" and 24" (13.7 mm to 609.6 mm), and the wall thickness should be between SCH 5S and XXS. A good manufacturer should be able to do both seamless and soldered production. Ultrasonic testing (UT), eddy current testing, and radiographic testing (RT/X-ray) must all be part of the testing procedures. Acceptance by a third party, like SGS, BV, TUV, DNV, or ABS, shows that the manufacturer is honest and doesn't just rely on internal audits.
Value-Added Services That Reduce On-Site Rework Costs
It's possible to tell the difference between full-service manufacturers and material-only distributors by the processing services they offer:
- Precision beveled ends (BE) machined to ASME B16.25 tolerances, ready for orbital or manual TIG welding without on-site dressing
- Bright Annealed (BA), satin, or mirror-polished interiors (180# through 600# grit) to meet Ra surface roughness specifications for pharmaceutical contact surfaces
- Fixed-length cutting and pipe threading (NPT / BSPT) that eliminate field machining delays
- Passivation treatment to restore the chromium oxide passive layer after fabrication
The insides must be bright annealed (BA), satin, or mirror-polished (180# to 600# grit) to meet the Ra surface roughness requirements for medicinal touch surfaces.
Procurement Best Practices for TP316L Stainless Steel Pipes
Structuring Your Inquiry for Accurate Quotations
If you want to make a good BOM request for TP316L stainless steel pipe, you should include information about the grade (TP316L/UNS S31603), the standard (ASTM A312), the pipe form (seamless or welded), the NPS and schedule, the surface finish, the end type, the necessary length (5.8 m, 6 m, 11.8 m, 12 m, or random), and any certificates that are needed. When you don't give complete information in your inquiry, you might get SCH 40 when you asked for SCH 10S, or pickled finish when you needed BA for sanitary service.
Verifying Batch Consistency Between Pipes and Fittings
One common reason for on-site rework is that the pipe body and parts from different makers don't match up in size. When the pipe and elbow or reducer don't match up in terms of wall thickness limits, it can cause stress concentrations that can't be analyzed using ASME B31.3. The safest way to avoid this is to get all of your pipes, elbows, tees, reducers, and flanges from the same supplier and keep all of your heat lot documentation in one place.
Packaging and Logistics Considerations for International Projects
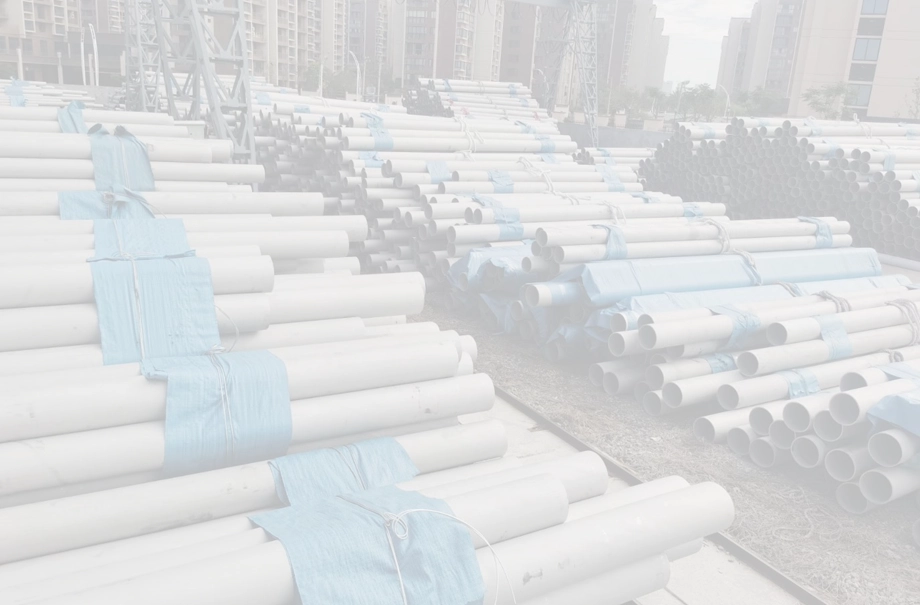
For export, packaging should have plastic end caps to protect the weld bevel surfaces, individual PE sleeves to keep things from getting scratched, and hexagonal steel-strapped bundles or plywood crates that are safe for ocean freight. Make sure the seller works with FOB, CFR, CIF, and DDP terms and can combine different types of products, like pipes, fittings, and flanges, into a single LCL or FCL package.

Case Studies and Applications in Pharmaceutical and Hygienic Systems
Biotech Facility WFI Distribution Loop
A biologics company needed a WFI loop made of internally polished (Ra ≤ 0.38 µm) TP316L seamless pipe in SCH 10S, NPS 1" through 3", with cut ends that were ready to orbitally weld and full EN 10204 3.1 approval. Because it had a low carbon content, it didn't need to be re-specified after the welding process. This cut the qualification time by about three weeks compared to a normal TP316 option.
Chemical Plant CIP Return Line Retrofit
A contract engineering company that was adding a CIP return line to a plant that makes food ingredients asked for welded TP316L pipe with a BA finish on the inside and a full eddy current inspection. The molybdenum content gave it the chloride resistance needed for hot, caustic, and acidic CIP cycles. The BA surface finish met the regulatory requirements for hygienic design set by EHEDG.
Offshore Pharmaceutical Logistics Platform
For its glycol cooling network, a cold-chain logistics platform that works near the water needed TP316L pipes. The high chlorine level in the air meant that molybdenum had to be added. Solution-annealed and pickled (SA&P) pipe in SCH 40S that came with third-party inspection certificates from DNV met both the environmental compliance requirement and the schedule for building work.
Conclusion
Tp316l stainless steel pipe is still the best choice for pharmaceutical, biotech, food processing, and chemical process plumbing because it has a very low carbon content and molybdenum added, which prevents the two most common types of failure: post-weld sensitization and chloride pitting. The grade includes a wide range of sanitary fluid system needs, from NPS 1/8" sanitary tube to large-bore pressure pipe in XXS wall. The best way to make sure that projects stay on schedule and follow the rules is to choose a maker that provides certified, traceable, dimensionally correct pipe with the right surface finishing.
FAQ
What is the carbon limit for TP316L, and why does it matter?
TP316L carries a maximum carbon content of 0.03%. This keeps the alloy below the threshold at which chromium carbides precipitate at grain boundaries during welding, preventing sensitization and maintaining full corrosion resistance without post-weld heat treatment.
Is TP316L approved for pharmaceutical contact surfaces?
Yes. When supplied with appropriate surface finish (typically BA or mirror-polished to ≤ Ra 0.38 µm) and full EN 10204 3.1 traceability, TP316L pipe meets FDA, GMP, and EHEDG material requirements for product-contact pharmaceutical piping.
What certifications should I request from the manufacturer?
Request EN 10204 3.1 MTC, ISO 9001:2015 certificate, PMI report, and intergranular corrosion test results (ASTM A262 Practice E). For pressure systems, PED and CE documentation may also apply.
What is the difference between seamless and welded TP316L pipe?
Seamless pipe contains no weld seam and offers higher structural uniformity for critical-pressure or vibration-intensive service. Welded pipe with 100% eddy current inspection is suitable for lower-pressure sanitary applications at a lower cost per meter.
Can I source pipes, elbows, and flanges from the same manufacturer?
Yes, and doing so is strongly advisable. Matching wall thickness, heat lot, and surface finish across the full fitting assembly prevents dimensional mismatches that cause stress concentration and require costly on-site rework.
Request a Quote from All Trust — Your Certified TP316L Stainless Steel Pipe Supplier
All Trust (Hebei All Trust Steel Co., Ltd.) sells checked Tp316l stainless steel pipe in all sizes. Their products are certified by EN 10204 3.1, have ISO 9001:2015 quality management, and have been inspected by a third party (SGS, TÜV, or BV). We can help with project procurement cycles from BOM inquiry to on-site delivery. Our response time is less than eight business hours, and we keep over 5,000 tons of inventory in stock at all times. To get a detailed quote, send your requirements to info@hballtrust.com.
References
1. ASTM International. ASTM A312/A312M: Standard Specification for Seamless, Welded, and Heavily Cold Worked Austenitic Stainless Steel Pipes. ASTM International, 2022.
2. American Society of Mechanical Engineers. ASME B31.3: Process Piping — Chemical Plant and Petroleum Refinery Piping. ASME, 2022.
3. American Society of Mechanical Engineers. ASME B16.25: Buttwelding Ends. ASME, 2022.
4. European Hygienic Engineering and Design Group. EHEDG Guidelines: Hygienic Design of Closed Processing Systems. EHEDG, 2021.
5. Stainless Steel World Magazine. "Corrosion Performance of 316L in Chloride-Bearing Pharmaceutical Process Streams." Stainless Steel World, 2023.
6. McGuire, Michael F. Stainless Steels for Design Engineers. ASM International, 2008.