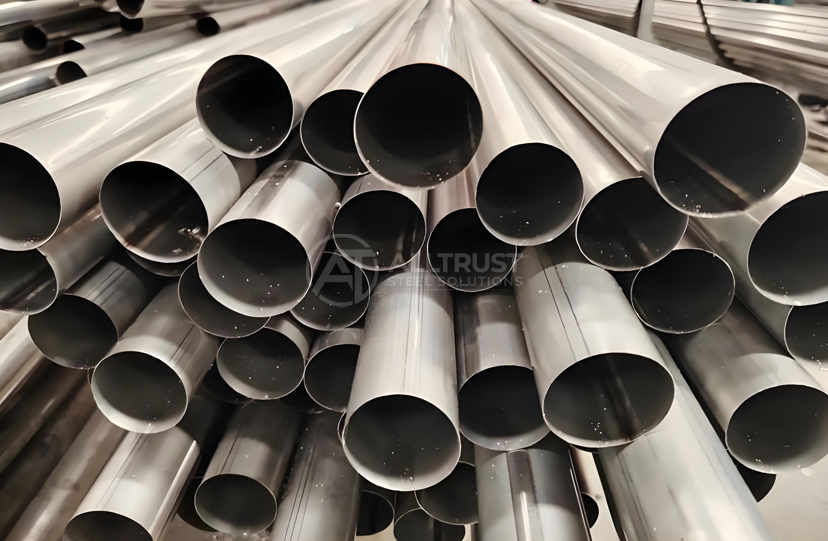
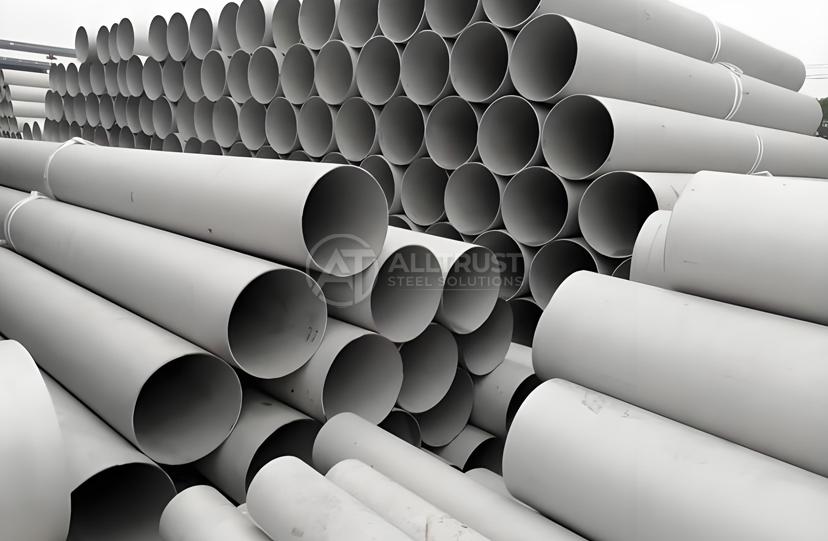
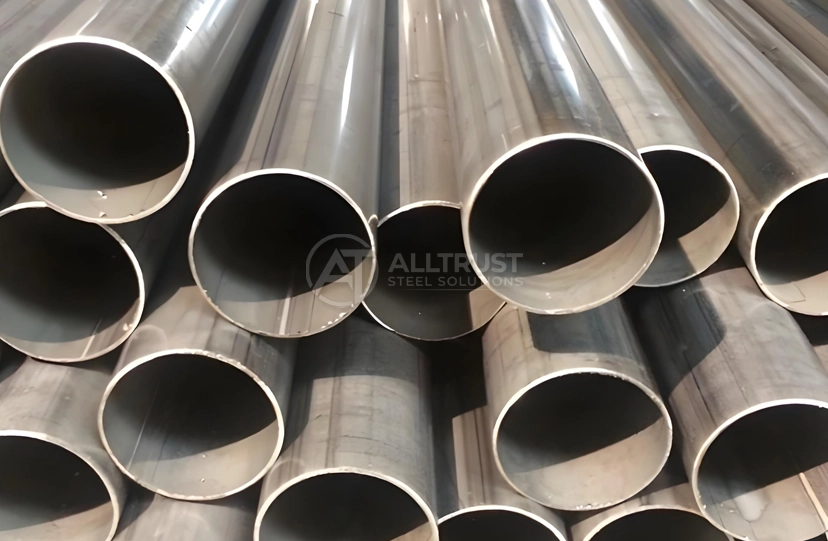
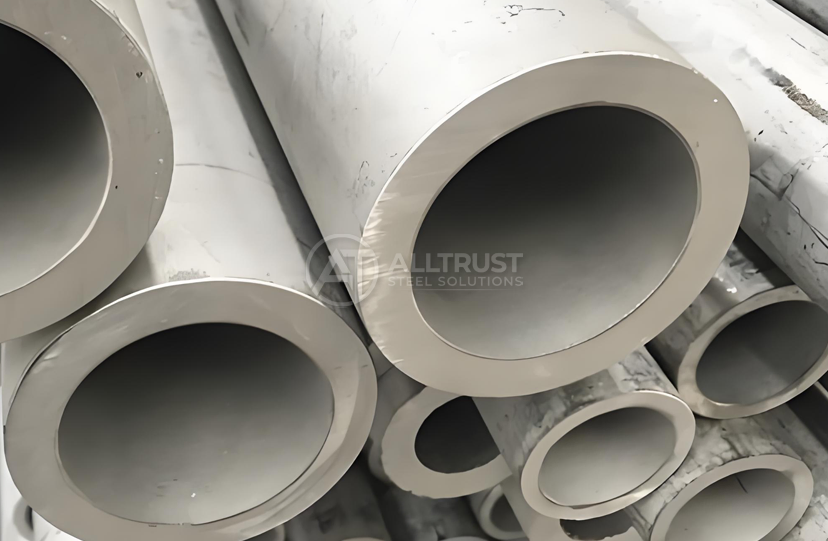
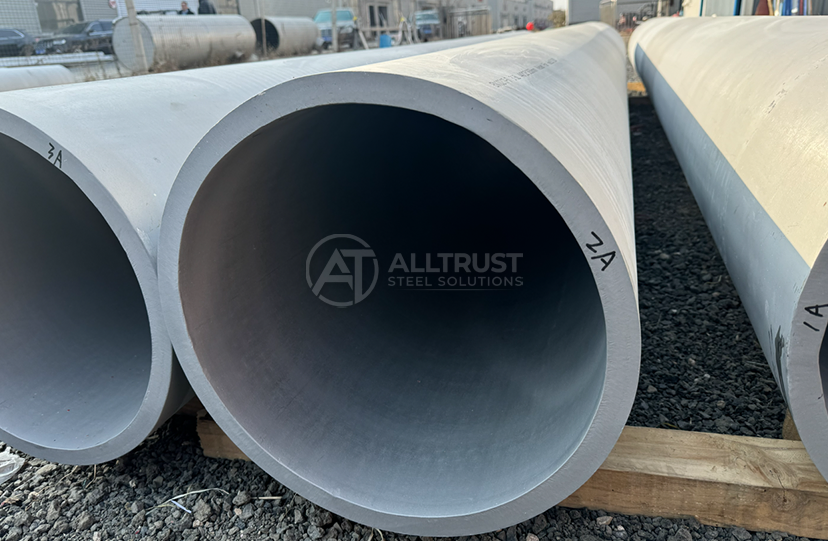
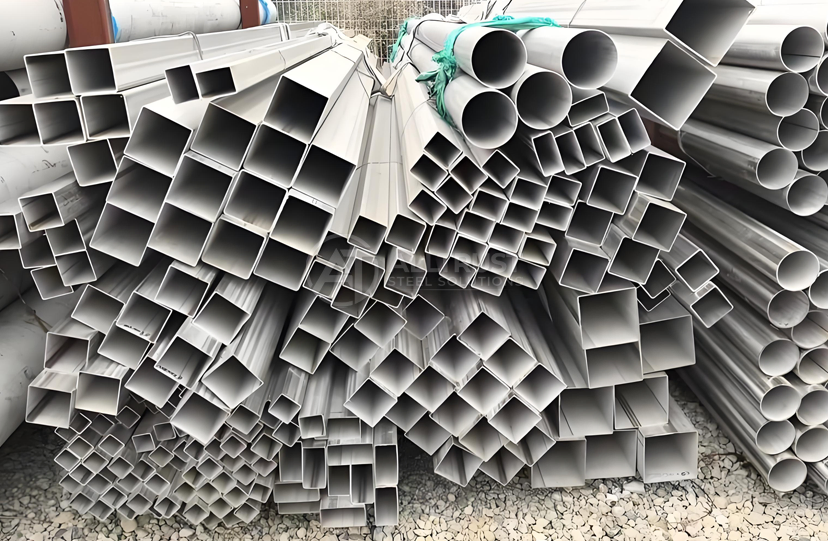
304L welded pipe
2. Standard: ASTM A312, ASTM A358, strictly compliant with international engineering welded pipeline norms
3. Process: Automated continuous straight-seam welding (TIG / Plasma) from precision-rolled steel plates without filler metal
4. Size Range: Outside Diameter from 1/2" up to 60", available in customizable engineering lengths to minimize field joints
5. Heat Treatment: Global post-weld solution annealing to restore full parenthal metal strength and corrosion defense to the weld line
6. Surface Finish: Clean acid-pickled and passivated finish, with internal weld bead removed flush to ensure zero fluid friction
7. Application: Chemical process lines, industrial wastewater drainage, municipal plumbing infrastructure, and paper mills
8. Service Advantage: 100% non-destructive testing (NDT), optional X-ray radiography (RT) on welds, and custom beveling services
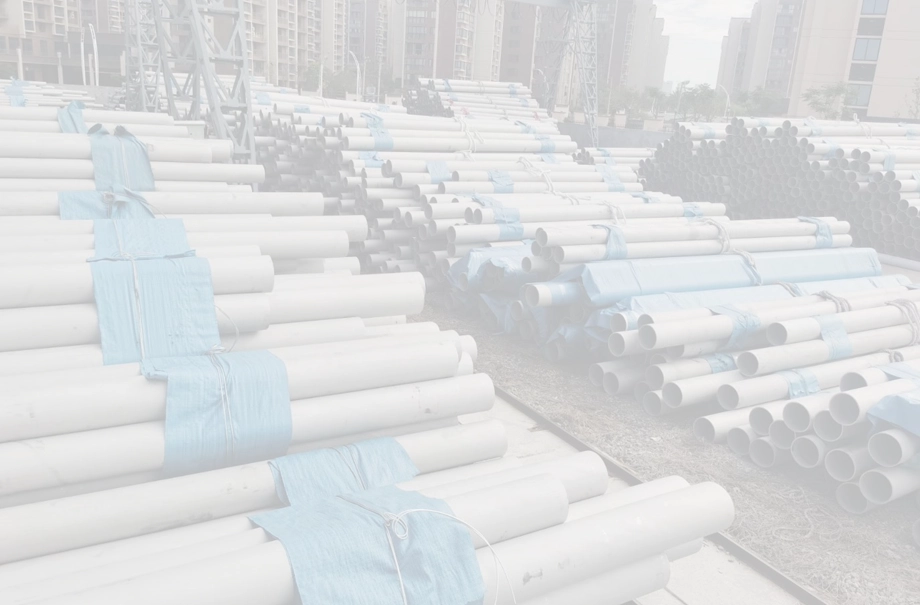
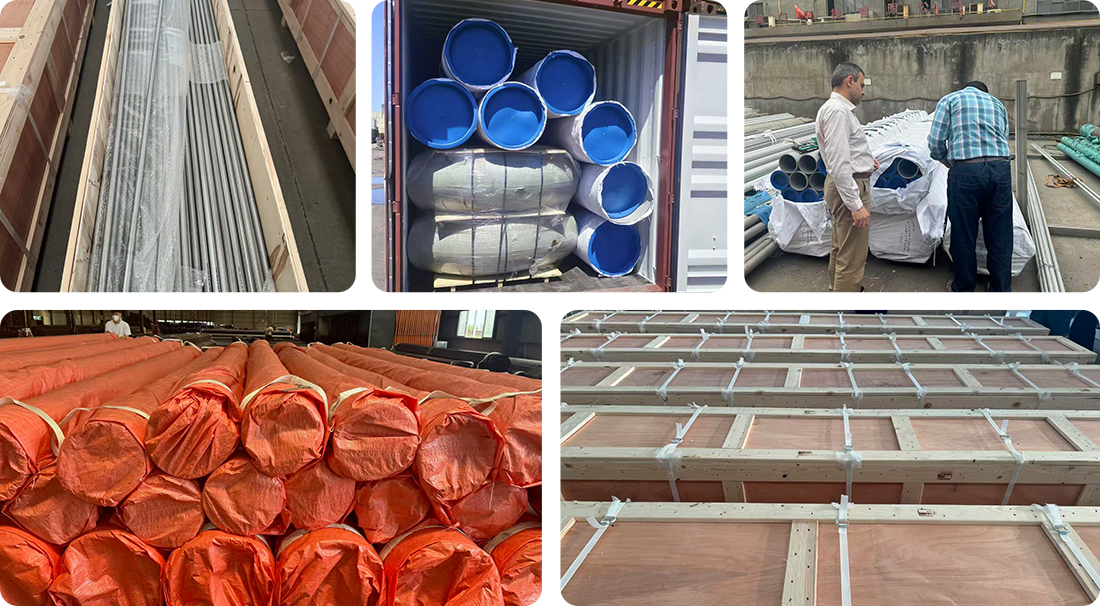
9. Packaging: Secure international bundle packing with protective end caps, or bulk-loaded with heavy-duty nylon lifting slings
10. Key Advantage: Completely eliminates harmful carbide precipitation during welding, ensuring absolute joint integrity without post-weld heat treatment
304L Welded Pipe – Extra-Low Carbon Industrial Piping Solutions for Superior Weld Integrity
HEBEI ALL TRUST STEEL CO., LTD specializes in manufacturing high-integrity 304L welded pipe engineered for critical process applications where weld-zone stability is non-negotiable. We have a yearly capacity of over 15,000 tons. We manufacture outside diameters from 1/2" to 60" using automated TIG/Plasma longitudinal welding technology. All products are 100% hydrostatically tested with optional radiographic weld inspection for no porosity or slag inclusions. Our pipes have a maximum carbon concentration of 0.03%, preventing the formation of chromium carbides during field welding. This means your joints are safe against intergranular corrosion, even in the most demanding chemical processing conditions.
Why Choose 304L Material for Welded Industrial Piping
The standard 304 grades are prone to sensitisation, a metallurgical defect in which chromium carbides precipitate at the grain boundaries during welding, leaving the neighbouring zone chromium-depleted and susceptible to corrosive attack. The extra-low carbon chemistry of 304L grade completely removes this concern.
Carbon is limited to ≤0.03% so you have the full range to multi-pass field weld with no post weld heat treatment. This makes our product ideal for large diameter trunk lines in chemical refineries, municipal water distribution systems and pharmaceutical clean utilities where annealing on site is not possible.
In addition, you get preserved mechanical properties: tensile strength of at least 485 MPa & good ductility with elongation above 40%. This enables your pipe systems to withstand thermal expansion cycles and vibration loads without early breaking.
Technical Specifications of the 304L Welded Pipe
| Parameter | Details |
|---|---|
| Material Grade | 304L (UNS S30403 / 1.4306 / Extra-Low Carbon) |
| Manufacturing Standard | ASTM A312, ASTM A358, ASTM A249, EN 10217-7 |
| Welding Process | Automated Longitudinal TIG / Plasma / Laser Welding |
| Outside Diameter | 13.7 mm – 1219.2 mm (1/2" – 48") |
| Wall Thickness | 0.5 mm – 30 mm (SCH 5S / 10S / 40S / 80S) |
| Standard Length | 5.8 m / 6 m / 11.8 m / 12 m / Custom Cut |
| Surface Finish | Solution Annealed & Acid Pickled / Bright Annealed / Polished (ID Bead Removed) |
| End Configuration | Plain End (PE) / Beveled End (BE) / Threaded (NPT/BSPT) |
| Mechanical Testing | Tensile, Flattening, Hardness, PMI Analysis |
| NDT Verification | 100% Hydrostatic + Eddy Current / Optional RT (X-ray) / UT |
| Corrosion Testing | ASTM A262 Practice E (Intergranular Corrosion Resistance) |
| Quality Certificates | EN 10204 3.1/3.2 MTC, ISO 9001:2015, CE, PED |
| Packaging Method | Hexagonal Bundles, Waterproof Weaving Bags, Plastic End Caps |
Superior Manufacturing Quality You Can Depend On
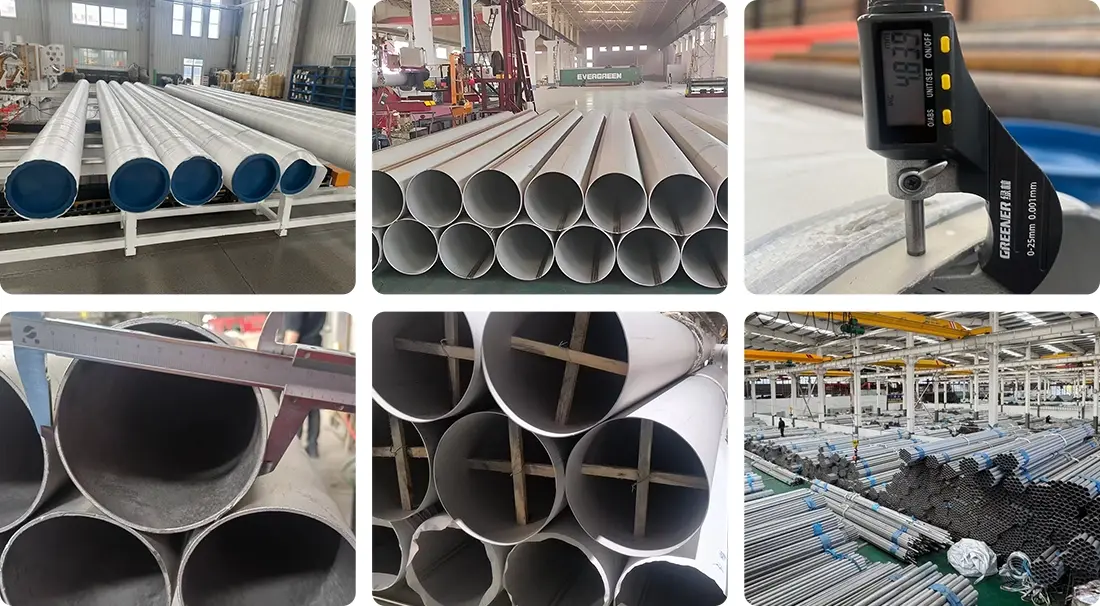
Our automated roll-forming and welding lines ensure exceptional dimensional consistency. Unlike manually fabricated pipes, our systems maintain outer diameter concentricity within ±0.5 mm and wall thickness uniformity across the entire length.
After welding, each pipe passes through a controlled solution annealing furnace at 1040–1120°C, followed by rapid quench cooling. This thermal cycle fully restores the parent metal's corrosion resistance to the weld seam, dissolving any residual carbides that might have formed.
3.2 Full acid pickling and passivation treatment by nitric-hydrofluoric acid baths We then proceed with a full acid pickling and passivation treatment. It takes off heat tint, weld discolouration and surface pollution and gives a durable chromium oxide passive coating that self repairs when scratched.
The internal weld flash is physically reduced to a flush finish, removing turbulence zones that might harbour bacterial growth or promote erosive wear in high velocity fluid streams.
General Applications in Industrial Fields
304L Welded Pipe is perfect for complicated industrial situations requiring chemical resistance and weld dependability.
Our pipes can safely convey organic solvents, weak acids and alkaline reagents in chemical and petrochemical processing facilities. The low carbon weld seams are resistant to intergranular damage when subjected to corrosive process disturbances.
This material is used in wastewater treatment plants for aeration headers, sludge transfer lines and desalination brine discharge systems. It resists chloride pitting and crevice corrosion and will provide decades of maintenance-free performance in high-moisture situations.
Food and beverage industries use our pipes for brewing tanks, dairy CIP systems and fruit juice conveyances. The smooth pickled surface does not permit bacterial adherence and the stable weld zones endure rigorous caustic and acidic cleaning cycles without leaching metallic ions.
These pipes are used in the distribution of purified water and creation of clean steam in pharmaceutical clean utilities, where material purity and surface integrity directly affect product validation.
Rigorous Quality Control Protocol
Every production batch follows our four-stage verification process. Raw material enters only after spectroscopic confirmation of nickel, chromium, and carbon content against mill certificates.
During fabrication, we conduct real-time dimensional monitoring and visual weld inspection. Post-production, 100% of pipes undergo eddy current testing to detect subsurface weld defects, plus hydrostatic pressure testing at 1.5× design pressure.
Random samples from each heat undergo destructive flattening tests and reverse bend tests to verify weld ductility. We also perform mandatory ASTM A262 Practice E intergranular corrosion testing on weld specimens to confirm sensitization immunity.
You will get full EN 10204 3.1 or 3.2 Mill Test Certificates including chemical composition, mechanical characteristics and NDT findings prior to shipping. We welcome third party inspection by SGS, BV or TUV at any point of the process.
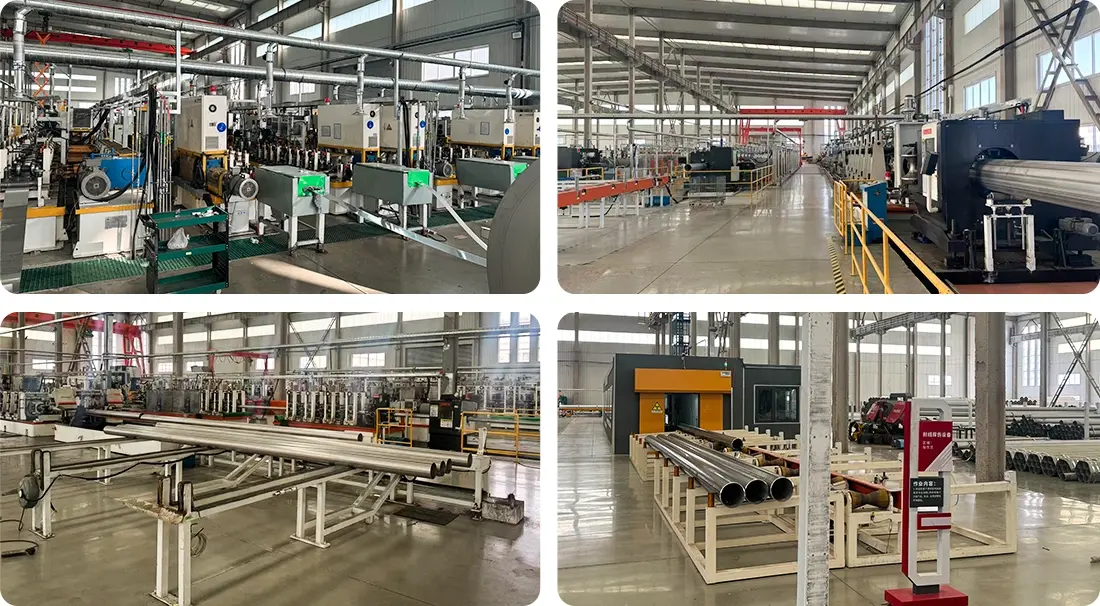
Custom Fabrication Services for Project-Specific Requirements
Beyond standard dimensions, we offer comprehensive value-added processing to reduce your on-site labor. Our CNC cutting systems deliver precise fixed lengths with tolerances of ±1 mm, minimizing material waste.
You can specify beveled ends machined to ASME B16.25 standards for direct butt-welding, or request roll-grooved ends for rapid mechanical coupling installation. We also provide NPT/BSPT taper threading for small-bore instrument connections.
For decorative or hygienic applications, we supply mirror-polished finishes up to 8K grade, plus satin or hairline surface treatments. Laser hole drilling and slot cutting services are available for manifold fabrication.
Reliable Global Delivery and Support
We maintain over 5,000 tons of rolling inventory covering common diameters and schedules, enabling 3–5 day dispatch for stock orders. Custom specifications ship within 15–20 days, with priority scheduling available to reduce lead times by 35%.
Our export packaging protects your investment through fumigation-free wooden cases, individual protective sleeves, and plastic end caps. We ship from Shanghai, Ningbo, Tianjin, Qingdao, and Shenzhen ports with flexible FOB, CFR, CIF, or DDP terms.
Mixed container loading is supported—combine pipes with fittings, flanges, and valves to optimize freight costs. Our engineering team provides material selection guidance, corrosion resistance analysis, and CAD drawing verification throughout your procurement process.
FAQ
Q:How does the extra-low carbon chemistry of this product enhance pipeline safety during field welding?
A: This pipe limits the carbon concentration to 0.03%, thereby avoiding dangerous chromium carbide precipitation at the joint zones during multi-pass welding, thus ensuring the toughness of the joint and avoiding weld-decay concerns.
Q: What are the structural merits of this straight-seam welded pipe for large-capacity plant utilities?
A:This tube is made of high-precision automated roll-forming of homogenous steel plates, providing excellent outer diameter concentricity, accurate wall uniformity, and great cost-effectiveness for large-bore lines.
Q:What strict non-destructive criteria must the longitudinal weld track clear prior to factory dispatch?
A:The entire length of the welded joint seam is subjected to mandatory 100% radiographic examination (RT/X-ray) or automated online eddy current diagnostic scanning to guarantee absolute joint fusion.
Q:Can this low-carbon welded series be configured with specialized end treatments for rapid site coupling?
A:Yes, we provide flexible fabrication selections including ANSI-standard tapered bevels for butt-welding, precision NPT/BSPT taper threading, or roll-grooved structures for mechanical couplings.
Q:What robust packaging protocols protect this welded pipe lot from transit humidity during maritime freight?
A:The pipes are secured into tight hexagonal bundles strapped with high-tensile steel bands, wrapped entirely inside heavy waterproof weaving bags, and fitted with protective end caps.
Contact Us
Request your detailed quotation and technical data package today for 304L welded pipe. Email us at info@hballtrust.com to discuss your specific requirements with our experienced team.