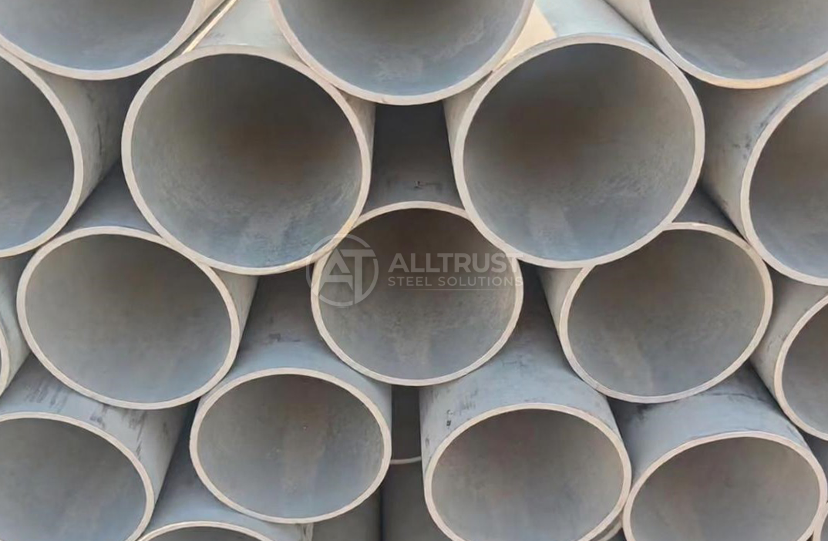
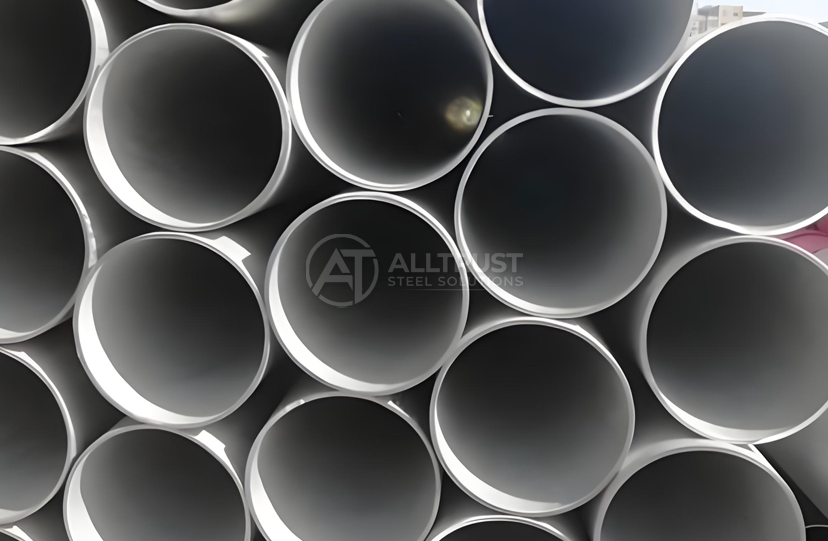
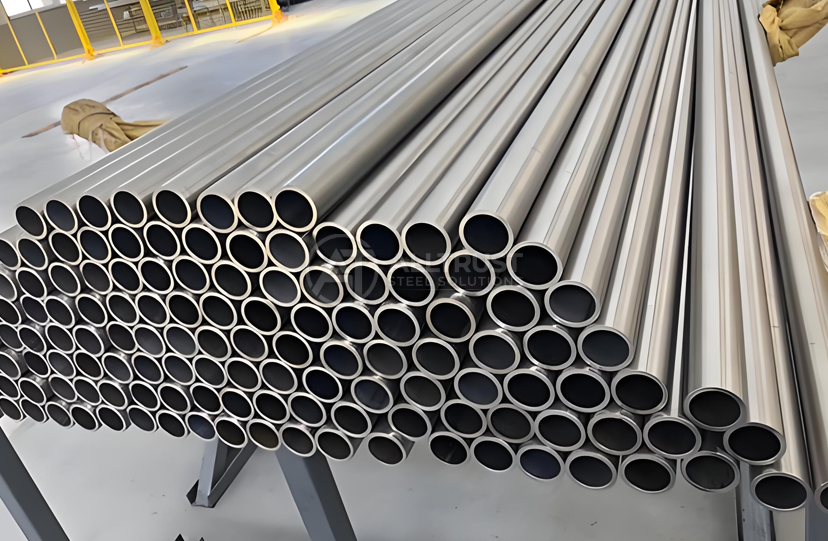
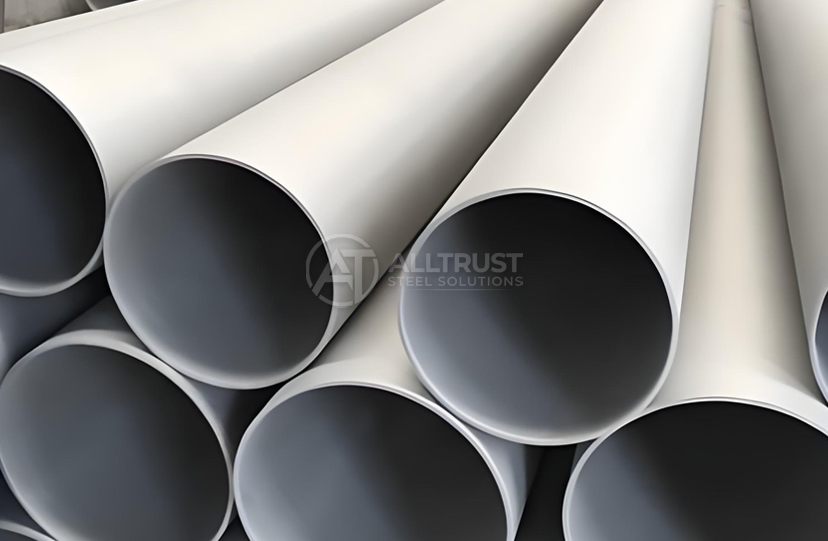
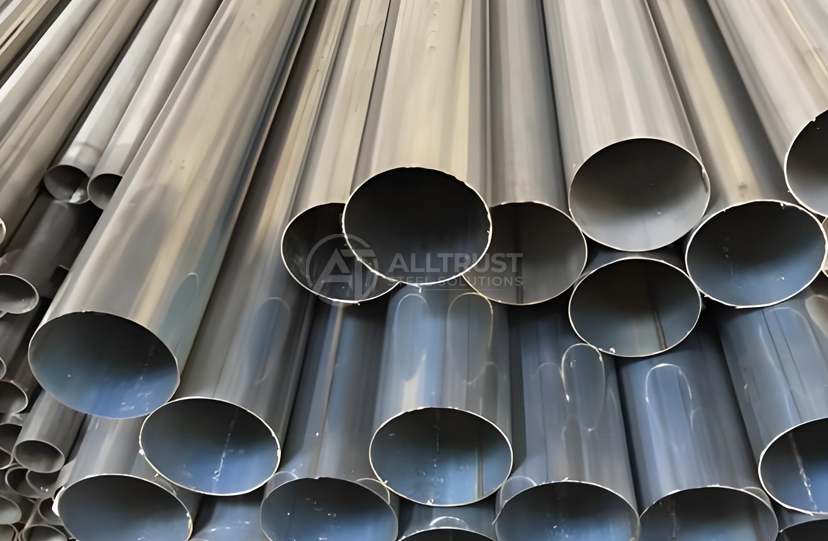
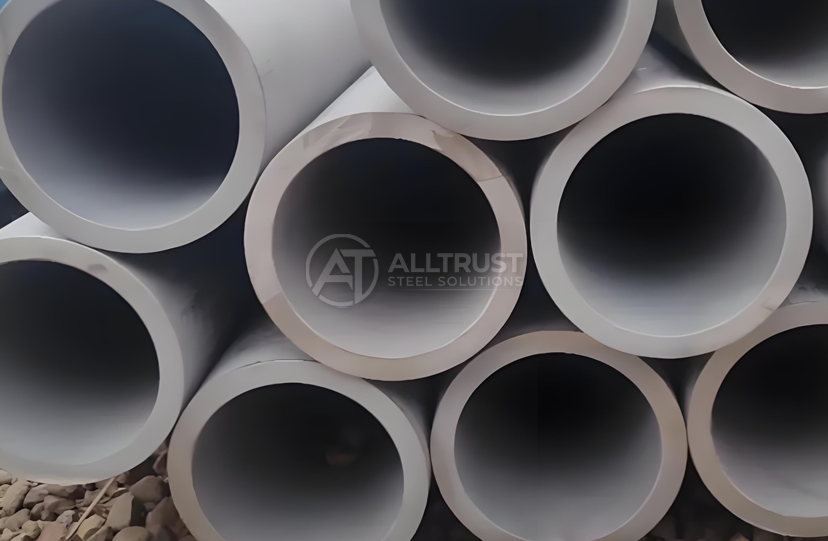
astm a213 tp316l tube
2. Standard: ASTM A213 / ASME SA213, standard specification for seamless boiler, superheater, and heat-exchanger tubes
3. Process: 100% seamless high-precision cold reduction, ensuring an ultra-smooth internal bore to eliminate fluid friction
4. Size Range: Metric and imperial dimensions up to 5" Outside Diameter, with tight wall thickness tolerance control
5. Heat Treatment: Full solution tempering in a controlled-atmosphere or vacuum furnace to secure optimal structural ductility
6. Surface Finish: High-purity bright annealed (BA) mirror finish, electro-polished (EP), or smooth pickled and passivated
7. Application: High-purity pharmaceutical condensers, marine engineering heat exchangers, oil refinery coolers, and chemical boilers
8. Service Advantage: Sourced from premium billets, support 100% Eddy Current and Hydrostatic tests, third-party inspections accepted
9. Packaging: Each tube individually plastic-sleeved and carefully nested in reinforced seaworthy plywood crates for absolute protection
10. Key Advantage: Offers supreme resistance to pitting in chloride media while eliminating intergranular decay risks at tube-to-sheet welds
ASTM A213 TP316L Tube – Ultra-Low Carbon Heat Exchanger Solution for Corrosion-Critical Applications
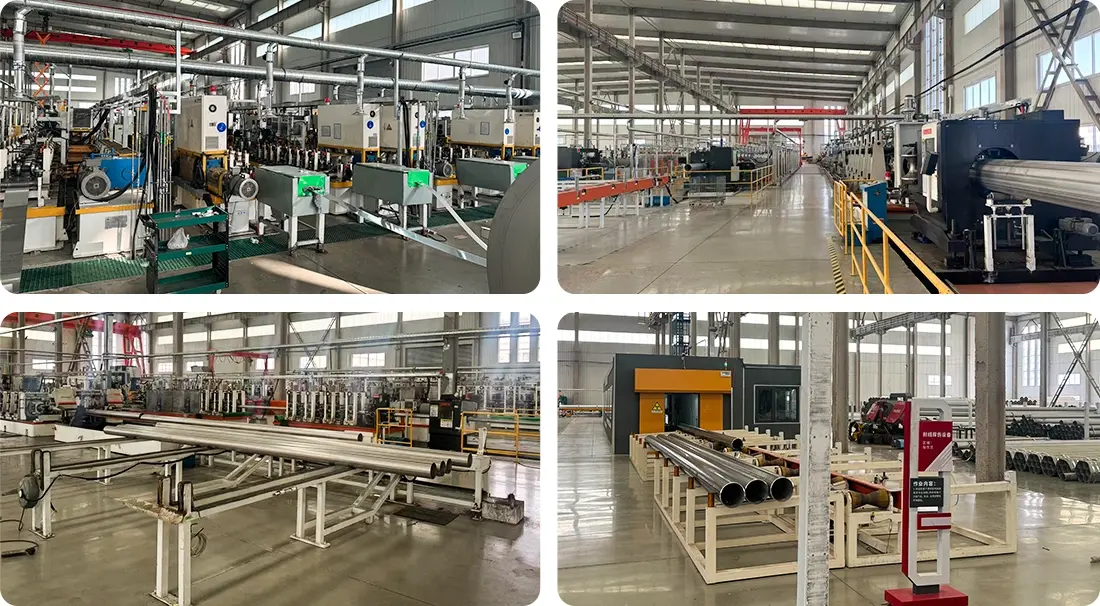
Hebei All Trust Steel Co., Ltd manufactures precision astm a213 tp316l tube engineered specifically for high-integrity boiler, superheater, and heat-exchanger installations. Our seamless tube is made of extra-low carbon molybdenum stabilised austenitic stainless steel (UNS S31603/1.4404) that provides excellent resistance to pitting and crevice corrosion in chloride-rich thermal conditions without weld-decay sensitisation. Every tube manufactured from our 15,000 ton per year capacity fulfils demanding ASTM A213/ASME SA213 criteria via 100% cold reduction processing, controlled-atmosphere solution annealing and eddy current testing. Our manufacturing tolerances are up to ±0.05 mm and are accompanied by full EN 10204 3.1 Mill Test Certificates and third party inspection approval from SGS, BV, TÜV.
Why Premium TP316L Seamless Tube Protects Your High-Temperature Systems
The choice of a suitable heat-exchanger tube is critical to ensuring the operational continuity of naval cooling systems, pharmaceutical condensers and petrochemical sour-service facilities. Intergranular corrosion of standard 316 stainless steel after welding may cause premature failure of boiler heads and tube to tubesheet junctions.
Our product has low carbon content (less than 0.03%) yet strong molybdenum integration (2.0-3.0%). This chemistry entirely avoids the chromium carbide precipitation at the grain boundaries during the thermal cycle.
3 HUGE benefits you get:
Weld-Zone Integrity: Avoids sensitisation in manufactured assemblies without post-weld heat treatment.
Chloride Resistance: Molybdenum concentration offers excellent pitting resistance in seawater, brackish condensate and desalination systems.
Structural Ductility Low carbon gives good formability for bending, flaring and expansion during installation.
All manufacturing lots are solution annealed in a vertical furnace at specified temperatures. This procedure evenly dissolves alloying elements and stabilises the austenitic microstructure to provide consistent mechanical performance in all wall thicknesses.
Technical Specifications & Dimensional Range of ASTM A213 TP316L Tube
| Parameter | Specification |
|---|---|
| Manufacturing Standard | ASTM A213 / ASME SA213 / EN 10216-5 |
| Material Grade | TP316L (UNS S31603 / 1.4404) |
| Process Type | Seamless Cold Drawn / Cold Rolled |
| Outer Diameter | 1/8" – 5" (3.18 mm – 127 mm) |
| Wall Thickness | 0.015" – 0.500" (0.38 mm – 12.7 mm) |
| Standard Length | 5.8 m / 6 m / 11.8 m / 12 m / Custom Cut |
| Surface Finish | Bright Annealed (BA) / Pickled & Passivated / Electropolished (EP) |
| Tensile Strength | ≥ 485 MPa (70 ksi) |
| Yield Strength | ≥ 170 MPa (25 ksi) |
| Hardness | ≤ 192 HBW (90 HRB) |
| NDT Testing | 100% Eddy Current + Hydrostatic Pressure Test |
| Quality Certificate | EN 10204 3.1 / 3.2 MTC with PMI Analysis |
| Third-Party Inspection | SGS / BV / TÜV / DNV / ABS Accepted |
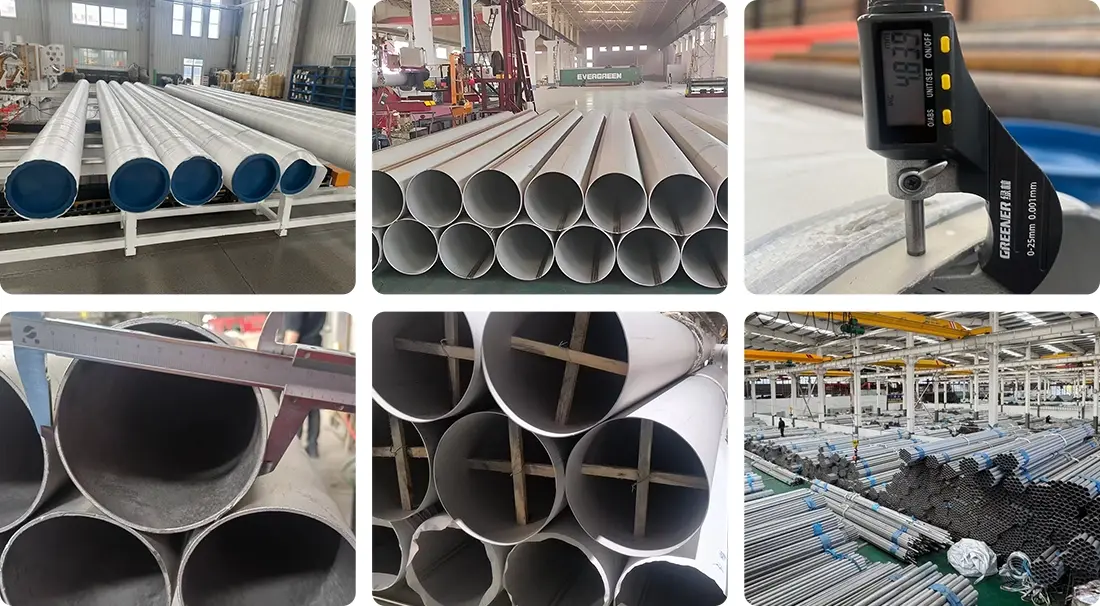
Our dimensional precision reaches industry-leading tolerances. Wall thickness consistency stays within ±5% across the entire length, ensuring predictable thermal conductivity and pressure ratings in your heat-transfer calculations.
Five Performance Advantages That Reduce Your Total Cost of Ownership
1. Zero Sensitization Risk in Welded Assemblies
The extra-low carbon chemistry of our product guarantees that chromium remains in solid solution rather than forming grain-boundary carbides. You can weld tube bundles, headers, and manifolds without requiring costly post-weld annealing cycles. This saves both fabrication time and eliminates potential distortion in pre-assembled units.
2. Superior Pitting Resistance in Chloride Media
2.0–3.0% molybdenum is present which results in the formation of a persistent passive oxide layer that is resistant to localised assault in brackish water, marine settings and chemical processing streams. Field testing indicated equivalent pitting resistance values (PRE) > 24 and this tube is appropriate for sustained exposure at high temperatures to chloride concentrations > 500 ppm.
3. Cold-Drawn Precision Super-Smooth Bore
Our cold reduction method produces an interior surface roughness of less than Ra 0.8 microns. The smooth bore design decreases fluid friction, minimises fouling deposits and enables easy mechanical or chemical cleaning. This increases maintenance intervals and maintains heat-transfer efficiency across the service life of your tube.
4. Full Traceability with Certified Test Reports
Every tube batch ships with EN 10204 3.1 Mill Test Certificates documenting:
- Heat number and melt chemistry
- Tensile, yield, and elongation values
- Grain size measurement (ASTM E112)
- Intergranular corrosion test results (ASTM A262 Practice E)
- Eddy current and hydrostatic test records
This documentation supports your quality audits, project specifications, and compliance verification for international codes including ASME Boiler & Pressure Vessel Code Section I and II.
5. Flexible Customization for Complex Projects
We accommodate your unique installation requirements through precision services:
- Custom cut lengths with deburred square ends
- Metric wall thickness matching European blueprints
- U-bend and hairpin configurations for compact exchanger designs
- Electropolished finishes meeting pharmaceutical 3-A Sanitary Standards
Mixed container loading combines tubes, fittings, and flanges to optimize your logistics costs.
Industrial Applications Where TP316L Delivers Critical Performance
Marine Heat Exchangers & Condensers
The chloride-induced stress corrosion cracking resistance of materials for seawater cooling systems is required. Our astm a213 tp316l tube is used in main engine jacket water coolers, HVAC seawater condensers and desalination pre-heaters when 316 grade metals fail prematurely.
Biotech & Pharmaceutical Clean Rooms
High-purity water-for-injection (WFI) loops and clean-in-place (CIP) circuits need tubes that can withstand severe sanitising chemicals and resist microbial colonisation. Smooth electropolished surface and corrosion resistance meets FDA, ASME BPE and EU GMP criteria for sterile fluid handling.
Sour Service Petrochemical
Sulphide stress cracking is seen in carbon steels in hydrogen sulphide (H₂S) service in refinery hydrotreaters and gas processing units. The structure, with the seamless construction and the nickel stabilised austenitic matrix, guaranties the immunity to H2S embrittlement at temperatures to 400°C.
Industrial Boiler Superheaters Sections
Low-carbon chemistry is used to avoid weld degradation in drum-to-header connections and tube-to-tubesheet joints that are subjected to cyclic thermal stress. The material can survive thousands of start-up and shut-down cycles without cracking or grain-boundary assault while retaining its mechanical strength.
Full Quality Control Protocol
Our four step inspection procedure guaranties zero fault delivery.
Stage 1: Raw Material Inspection
Spectrographic examination reveals chromium, nickel, molybdenum and carbon concentrations are consistent with TP316L chemistry. We only begin manufacturing with certified virgin stainless steel from ISO 9001 manufacturers.
Stage 2: Monitoring in the process
During cold drawing laser micrometres monitor the outside diameter and wall thickness in real time. Reject gates automatically eliminate any tube that is out of dimensional limits before annealing.
Stage 3: Compulsory Non-Destructive Testing
100% eddy current scanning reveals internal and surface faults to 0.5 mm. Hydrostatic pressure test for leak-free integrity at 1.5x rated operating pressure.
Stage 4: Final Inspection & Documentation
Visual examination confirms surface finish quality. PMI (Positive Material Identification) using XRF spectroscopy verifies alloy composition. Each bundle receives serialized MTC and packing list for complete traceability.
Third-party witness inspection available at any stage to meet your project quality plan requirements.
Secure Global Delivery & Professional Support
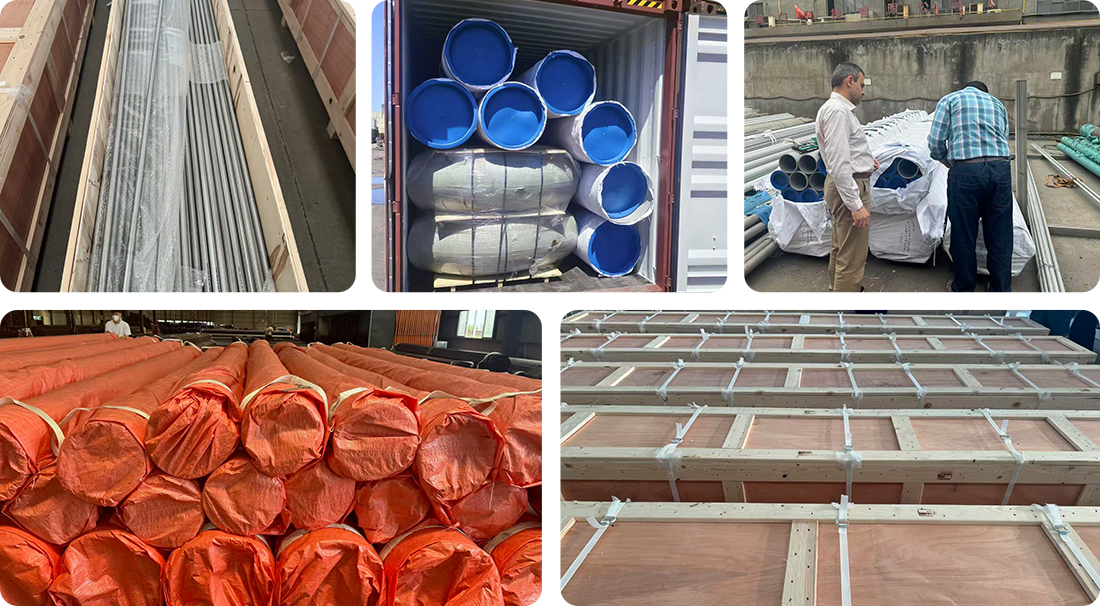
Your tubes arrive protected through multi-layer export packaging:
- Individual plastic sleeves preventing surface scratches
- Hexagonal bundles with heavy-duty steel strapping
- Fumigation-free plywood cases meeting ISPM 15 standards
- Waterproof wrapping protecting against humidity and salt spray
We ship from Shanghai, Ningbo, Tianjin, Qingdao, and Shenzhen ports with FOB, CFR, CIF, and DDP terms. Standard delivery schedules: 3–5 days for stock items, 15–20 days for custom orders.
Our engineering team provides technical support including material selection guidance, corrosion resistance analysis, and stress calculation verification. One-year product warranty covers manufacturing defects with fast replacement solutions.
FAQ
Q:Why should an engineer select this product over a traditional tp316 layout for boiler infrastructure?
A:The TP316L chemistry restricts carbon metrics below 0.03% while retaining heavy molybdenum integration, completely eliminating weld-decay sensitization and protecting critical high-temperature boiler loops from severe crevice corrosion.
Q:What advanced manufacturing loops secure the microstructural parameters of this low-carbon tube batch?
A:Every production lot is precision cold-drawn or rolled under rigid specifications, followed by vertical controlled-atmosphere solution annealing to dissolve alloy elements uniformly and achieve complete microstructural uniformity.
Q:What precision non-destructive testing (NDT) matrix is enforced to validate the physical safety of these tubes?
A:Every single piece must clear continuous automated internal eddy current scanning lines combined with high-pressure hydrostatic leakage pressure validation or comprehensive volumetric ultrasonic scanning.
Q:Can the dimensional profiles of this low-carbon series be customized to fit high-purity or compact blueprints?
A:Yes, we offer extensive manufacturing flexibility, supporting precise metric thickness configurations, deburred square-cut plain ends, and customized batch packing wrapped with waterproof fiber liners.
Q:What precise material documentation is dispatched with this low-carbon pressure series to guarantee compliance?
A:All shipments include a fully transparent Mill Test Certificate (MTC) conforming strictly to EN 10204 3.1 criteria, documenting exact chemical heat numbers, grain size configurations, and physical load values.
Contact Us
Get precise pricing, dimensional specifications, and delivery schedules tailored to your project requirements for the astm a213 tp316l tube. Contact our technical sales team at info@hballtrust.com with your tube specifications and quantity.