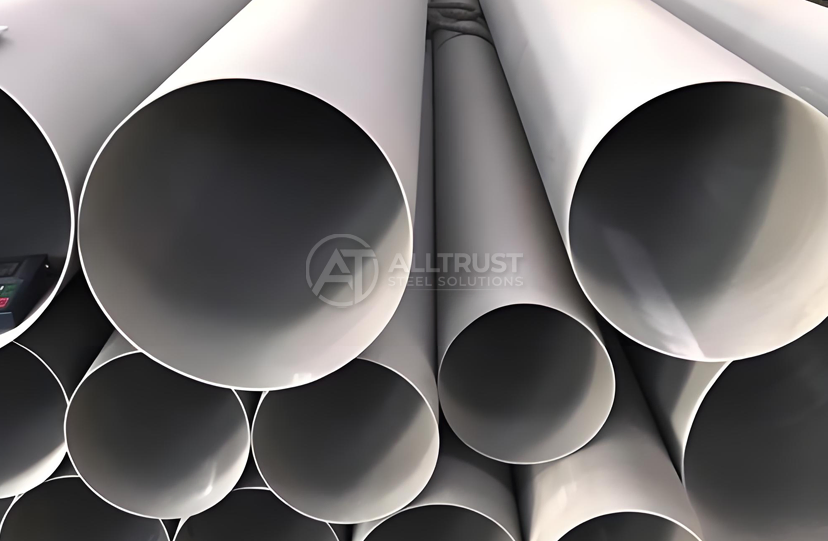
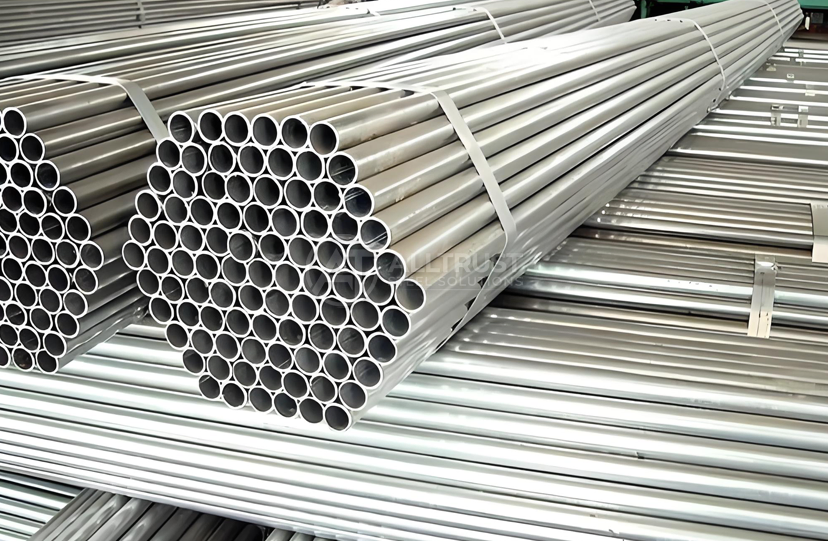
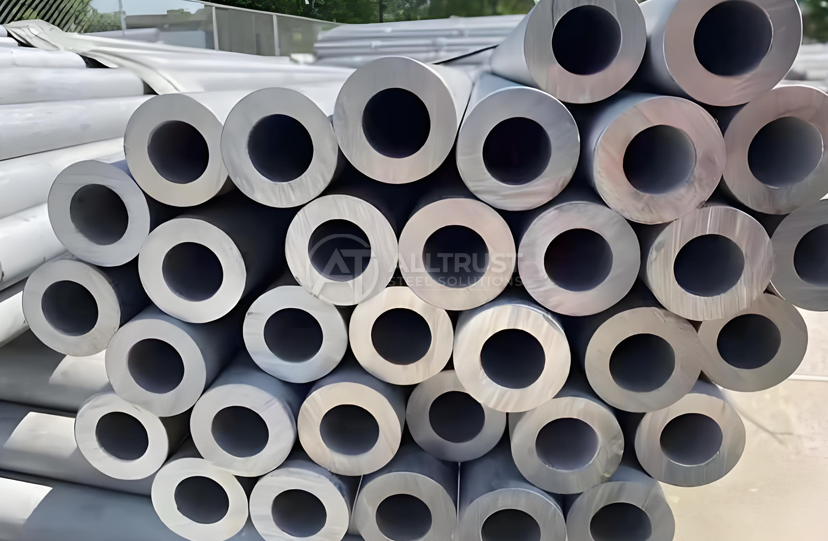
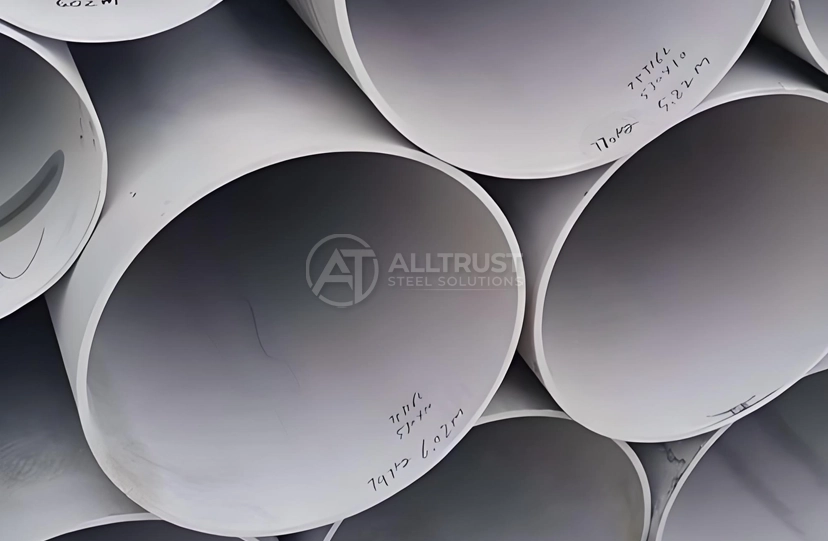
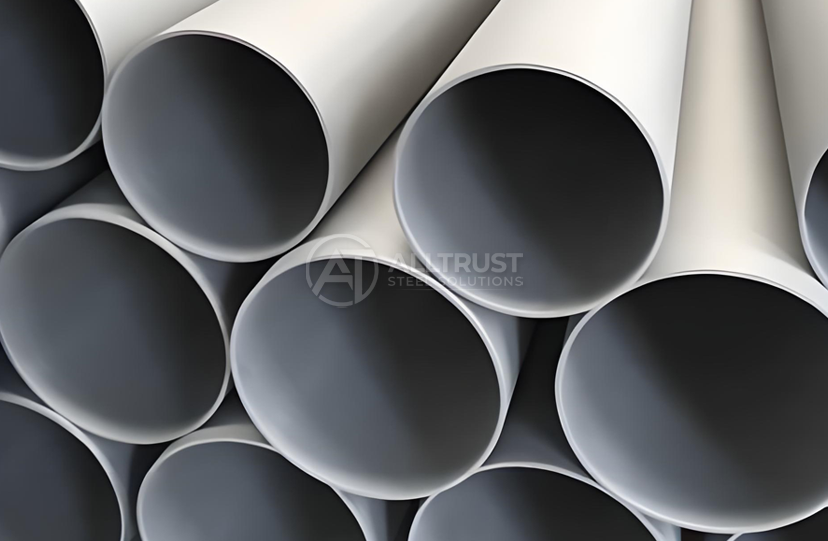
astm a376 seamless pipe
2. Standard: ASTM A376 / ASME SA376, the definitive standard for critical central-station piping
3. Process: 100% seamless hot-finished or cold-drawn, ensuring no potential weld failure zones
4. Size Range: DN15 to DN600 (NPS 1/2" to 24"), standard and non-standard schedules available
5. Heat Treatment: Mandatory solution annealing to fully restore mechanical properties and corrosion defense
6. Surface Finish: Solution annealed and pickled (SA&P) for ultimate structural reliability
7. Application: High-pressure power plant steam headers, heavy industry boilers, and refineries
8. Service Advantage: Comprehensive non-destructive testing (NDT) reports included in shipping documents
9. Packaging: Secure international sea-freight packaging with heavy-duty end protectors and marks
10. Key Advantage: Certified to withstand massive internal pressure and thermal cycling without fatigue
ASTM A376 Seamless Pipe for High-Temperature Central-Station Service | Superior Pressure Integrity Solutions
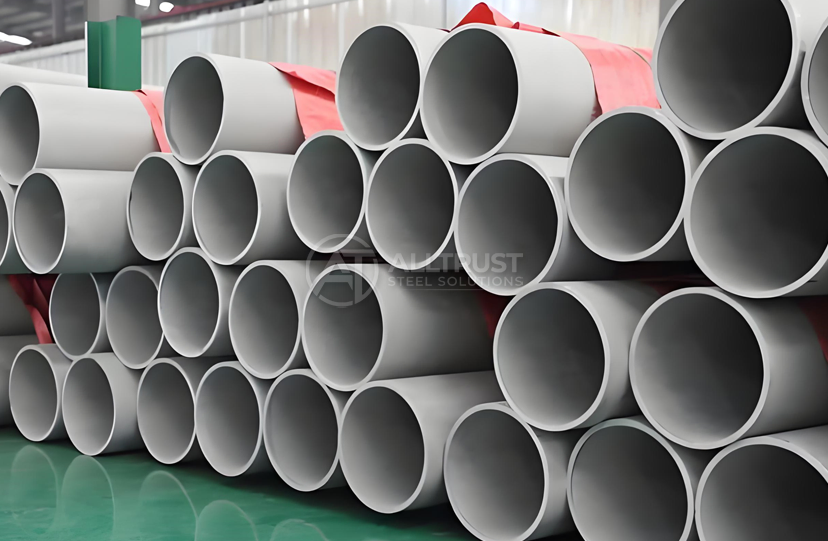
ASTM A376 seamless pipe manufactured by Hebei All Trust Steel Co., Ltd represents a specialized austenitic steel piping solution engineered exclusively for high-temperature central-station applications.
Our products range offers excellent pressure-bearing integrity for important power generating infrastructure, with a manufacturing capacity of more than 15,000 tonnes per year and 100% hydraulic testing coverage. The seamless pipe has no weld-joint weak points and may be used for outer diameters up to 1016 mm with operating temperatures always exceeding 538°C (1,000°F). All manufacturing lots are fully non-destructively tested and manufactured in strict conformity with ASTM/ASME, with obligatory solution annealing heat treatment to ensure perfect operation in superheater headers, thermal recovery units and main cooling loops.
What Makes ASTM A376 Seamless Pipe Essential for Critical Infrastructure
The Products Standard solves unique industrial difficulties that common purpose stainless pipes cannot meet. Unlike welded alternatives, this standard reduces the hazards of longitudinal seam failure in high pressure steam situations.
Your power plant systems go through significant heat cycling. Standard plumbing solutions often fail at weld joints when subjected to prolonged temperatures beyond 1,000°F. The continuous build-up therefore produces a homogeneous grain structure across the wall of the pipe.
The standard requires coarse grain size (ASTM No. 7 or coarser) for H-grade materials. This metallurgical requirement immediately improves creep-rupture strength in long term high temperature service. You get a longer working life without sacrificing structural integrity.
Three major industries rely on this technology:
Central Station Power Plants: Main steam lines with superheated steam experience thermal expansion stress, thus materials must be selected appropriately. Seamless structure avoids catastrophic collapse of reheat pipe systems.
Petrochemical Refineries: pipework exposed to catalytic cracking units is subject to high-velocity corrosive gases. This homogeneous distribution of wall thicknesses results in uniform pressure containment throughout the heat gradients.
Nuclear Power Generation. Primary cooling loops have to be absolutely reliable. The seamless body removes possible leak pathways, while preserving durability in radiation intense settings.
Technical Specifications & Available Configurations
| Parameter | Specification Details |
|---|---|
| Standard Compliance | ASTM A376 / ASME SA376 / ASTM A312 / EN 10216-5 |
| Material Grades | TP304H / TP316H / TP321H / TP347H |
| Manufacturing Process | Hot Finished Seamless / Cold Drawn Seamless |
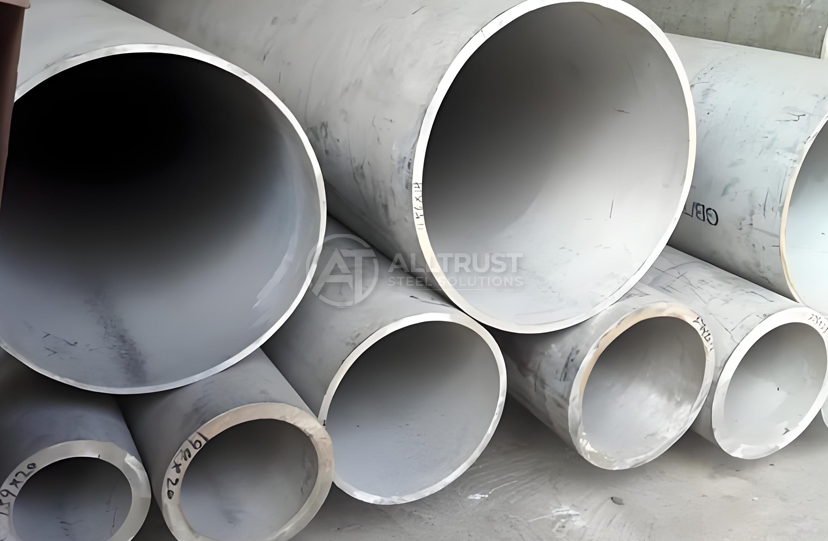
| Outer Diameter Range | 1/2" – 24" (21.3 mm – 609.6 mm) |
| Wall Thickness Options | SCH 10S / SCH 40S / SCH 80S / SCH 160 / SCH XXS (2.0 mm – 50.0 mm) |
| Standard Lengths | 5.8 m / 6 m / 11.8 m / 12 m / Custom Cut Length |
| Heat Treatment | Solution Annealed at Controlled Temperature |
| Surface Finish | Solution Annealed & Pickled (SA&P) / Shot Blasted / Passivated |
| End Configurations | Plain End (PE) / Beveled End (BE) |
| Testing Requirements | 100% Hydrostatic Test / Ultrasonic Test (UT) / Eddy Current Test |
| Mechanical Testing | High-Temperature Tensile Test / Creep Rupture Test / Grain Size Verification |
| Quality Certificates | EN 10204 3.1 & 3.2 Mill Test Certificate (MTC) / ISO 9001:2015 |
| Third-Party Inspection | SGS / BV / TUV / DNV / ABS Supported |
Manufacturing Excellence That Defines Reliability
Your infrastructure projects require absolute dimensional precision. Our advanced hot-piercing technique transforms solid billets into flawless cylindrical structures without introducing weld seams. This process maintains consistent wall thickness distribution even in heavy-duty Schedule 160 and XXS configurations.
Cold reduction loops follow initial hot-finishing operations. Micro-calibrated precision drawing ensures outer diameter tolerances within ±0.05 mm. This level of accuracy prevents installation complications in complex piping assemblies.
Every manufacturing lot passes through automated eddy current monitoring systems. These non-destructive evaluation protocols detect subsurface micro-voids before material enters heat treatment cycles. You receive guaranteed structural soundness in every shipment.
Solution annealing is necessary, and it is carried out at tightly regulated temperatures over 1,900 °F (1,038 °C). Then it is rapidly quenched to fix the best austenitic grain structure. The heat treatment restores the mechanical qualities to the original level and at the same time provide the highest possible corrosion resistance.
Superior Material Properties for Extreme Conditions
The H-grade designations in astm a376 seamless pipe products incorporate controlled carbon content between 0.04-0.10%. This specific carbon range provides exceptional creep-rupture strength during sustained high-temperature exposure.
Your steam header systems experience continuous thermal stress. Standard austenitic grades lose tensile strength above 800°F. The coarse grain structure in H-grades maintains minimum tensile strength of 75 ksi (515 MPa) and yield strength of 30 ksi (205 MPa) throughout service life.
Chemical composition verification occurs through spectrographic analysis of every heat number. We guarantee precise chromium, nickel, and molybdenum content according to ASTM specifications. This traceability prevents material substitution risks common in international supply chains.
Intergranular corrosion testing per ASTM A262 confirms that manufacturing processes haven't sensitized the material. You avoid premature failure from grain boundary deterioration in corrosive operating environments.
Comprehensive Quality Assurance Protocol
Our four-stage quality management system protects your investment from raw material selection through final shipment inspection.
Stage One – Material Verification: Only ISO-certified steel mills supply virgin stainless steel billets. Complete chemical composition analysis occurs before production authorization.
Stage Two – Process Monitoring: Real-time dimensional inspection tracks outer diameter and wall thickness during manufacturing operations. Thermal process supervision ensures proper heat treatment parameters.
Stage Three – Non-Destructive Testing: One hundred percent volumetric ultrasonic examination detects internal discontinuities. High-pressure hydrostatic testing validates leak-proof integrity under simulated operating conditions.
Stage Four – Documentation Preparation: Every order receives Mill Test Certificates complying with EN 10204 3.1 standards. These documents detail exact chemical heat numbers, grain size measurements, and mechanical property test results.
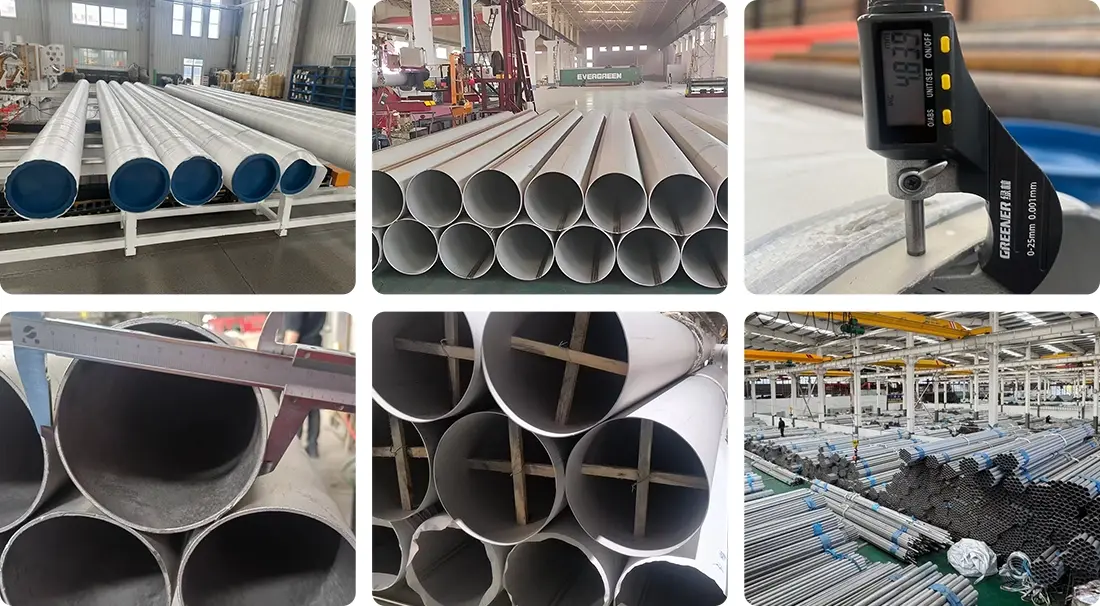
Customization Capabilities for Specialized Requirements
Your technical specs typically call for non-standard configurations. Custom sizes in outer diameter, wall thickness and length are available with no minimum order quantities.
Precision laser cutting provides precise dimensional tolerances for pre-fabricated systems. Bevel ends are prepared according to ASME B16.25 specifications to accommodate field welding techniques.
Heavy duty schedules such as SCH 160 and XXS variations are recommended for ultra-high-pressure applications. The smoothness of the interior surface can be maintained during cold drawing to a wall thickness of up to 50.0 mm.
Special surface treatments enhance corrosion resistance in aggressive chemical environments. Shot blasting and passivation services create protective oxide layers that extend service intervals between maintenance shutdowns.
Rigorous Testing Documentation You Can Trust
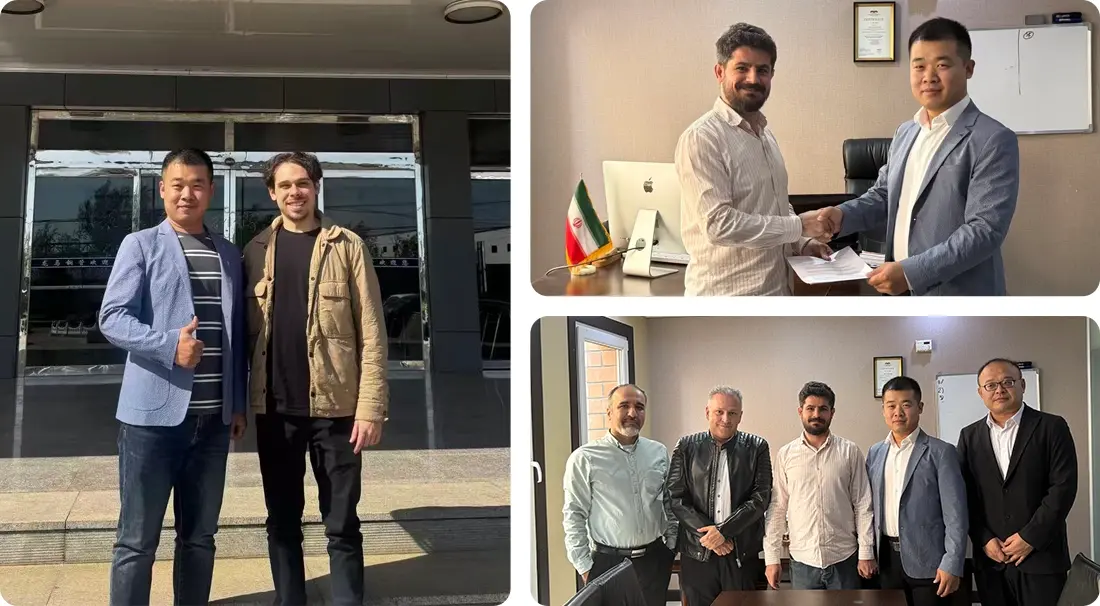
Independent verification of material conformity supported by third-party Inspection services of SGS, BV, TUV, DNV and ABS. These agencies are globally recognised and observe testing methods and evaluate the correctness of certification.
Positive Material Identification (PMI) reports accompany every shipment. Handheld X-ray fluorescence analysis confirms that delivered materials match specified grades without substitution.
Grain size examination results demonstrate compliance with ASTM E112 standards. For H-grade products, we document coarse grain structure requirements essential for high-temperature creep resistance.
Mechanical testing certificates include high-temperature tensile results, flattening test outcomes, and flaring test data. These destructive tests prove material ductility and fabrication suitability.
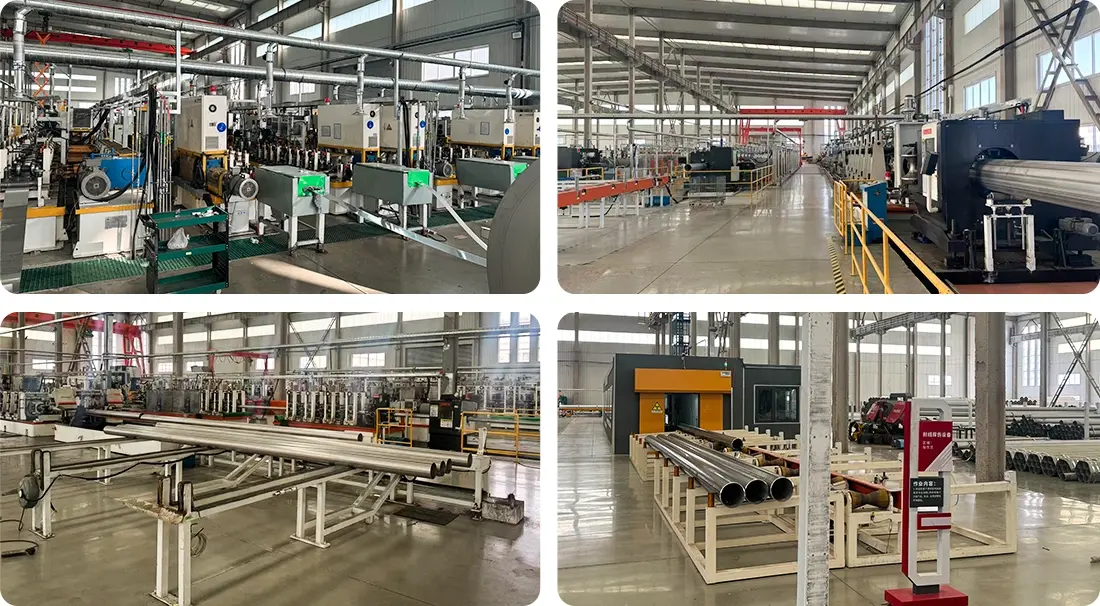
Strategic Inventory & Rapid Delivery Performance
Over 5,000 tons of rolling inventory covers frequently specified grades including TP304H, TP316H, TP321H, and TP347H. This stock availability reduces project lead times significantly.
Standard dimension orders ship within 3-5 business days from our warehouse facilities. Custom specifications typically require 15-20 days for production and quality verification.
Large-scale engineering projects receive priority production scheduling. Our 15+ strategic mill partnerships provide backup manufacturing capacity during peak demand periods. You avoid costly project delays caused by material shortages.
Secure Export Packaging for Global Shipments
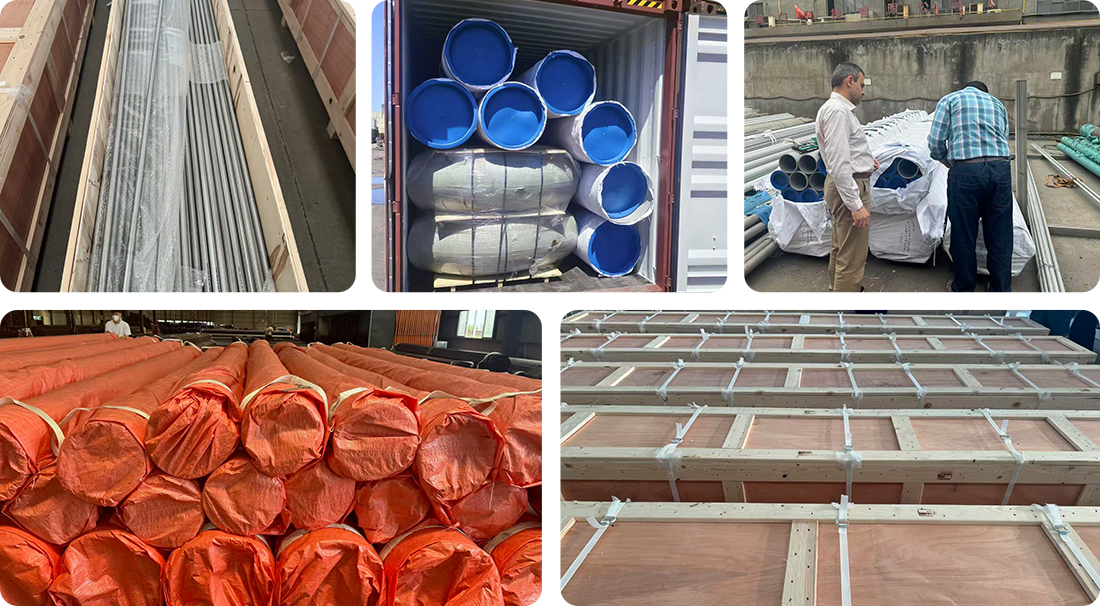
International sea freight demands robust protective packaging. Each pipe receives individual plastic end caps preventing moisture ingress and contamination. Heavy-duty woven bundles with steel strapping secure multiple pieces during container loading.
Fumigation-free wooden cases comply with ISPM-15 international phytosanitary standards. This packaging eliminates customs delays in Australia, European Union, and North American destinations.
Hexagonal bundle configurations optimize container space utilization. We calculate precise loading plans that maximize your freight investment while preventing transportation damage.
Waterproof wrapping protects pickled surfaces from salt corrosion during ocean transit. Your material arrives in ready-to-install condition without requiring additional surface preparation.
FAQ
Q:What core architectural feature maximizes the pressure containment capability of this product?
A:This pipe is manufactured via solid billet hot-piercing and precision cold reduction to produce a flawless, joint-free cylindrical wall that provides exceptional mechanical burst safety margins under extreme operating stresses.
Q:Under what operating thresholds is it contractually critical to select this seamless pressure pipe framework?
A:It is highly recommended for central-station power generation, volatile high-pressure steam headers, and severe thermal cycles where longitudinal weld line vulnerabilities must be entirely engineered out of the layout.
Q:What specific volumetric testing protocols verify that the seamless body is completely secure?
A:Every single lot passes through mandatory 100% volumetric ultrasonic testing (UT) paired with high-pressure hydrostatic leakage pressure validation to rule out microscopic internal flaws and sub-surface micro-voids.
Q:Can this high-pressure seamless series be tailored with customized thickness scales for specialized industrial grids?
A:We support extensive manufacturing configurations, accommodating standard nominal dimensions up to 24 inches across heavy-duty parameters including Schedule 160, SCH XXS, or bespoke high-thickness profiles.
Q:What precise mill traceability documentation is dispatched with this astm a376 seamless product?
A:We supply transparent Mill Test Certificates (MTC) in strict compliance with EN 10204 3.1 criteria, detailing exact chemical heat numbers, grain size numbers, and physical tensile load values.
Contact Us
Ready to specify the right astm a376 seamless pipe solution for your critical infrastructure project? Our engineering team provides material selection guidance and comprehensive technical documentation. Contact us at info@hballtrust.com today.