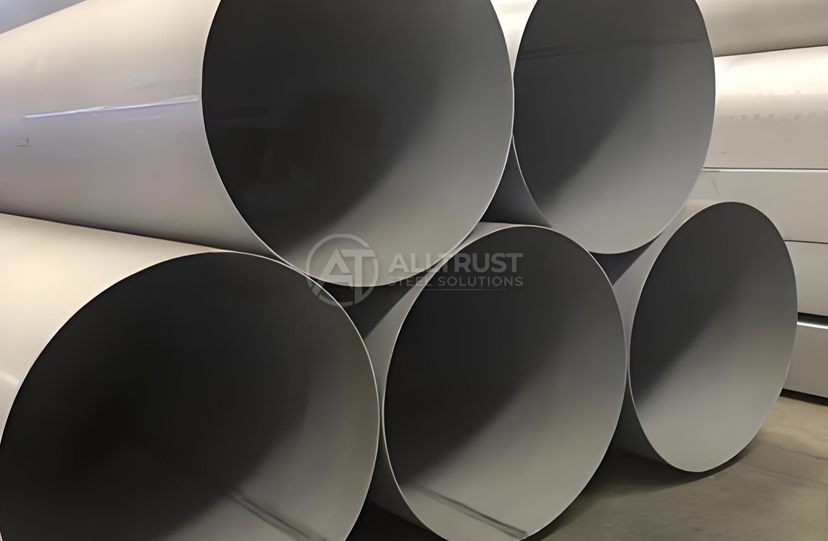
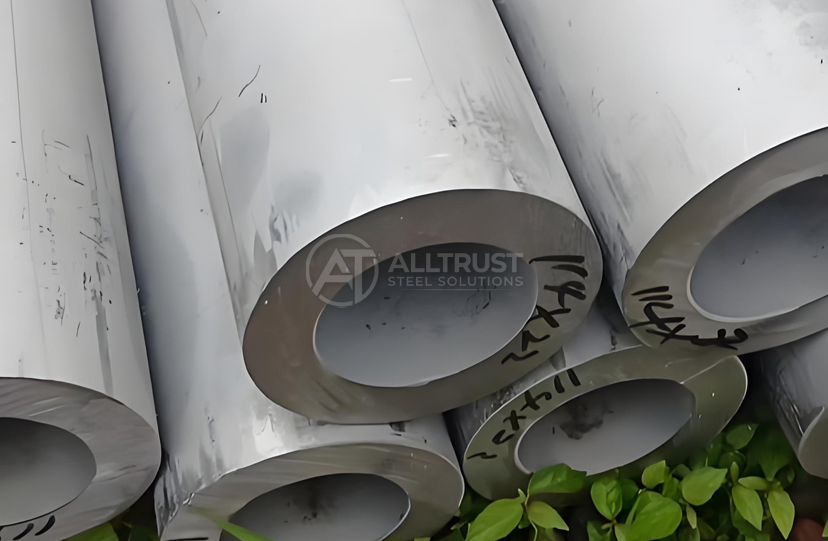
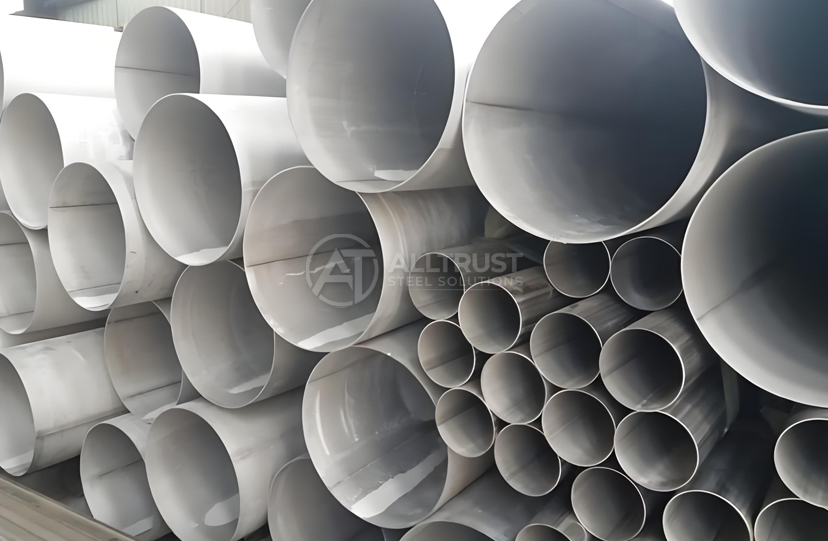
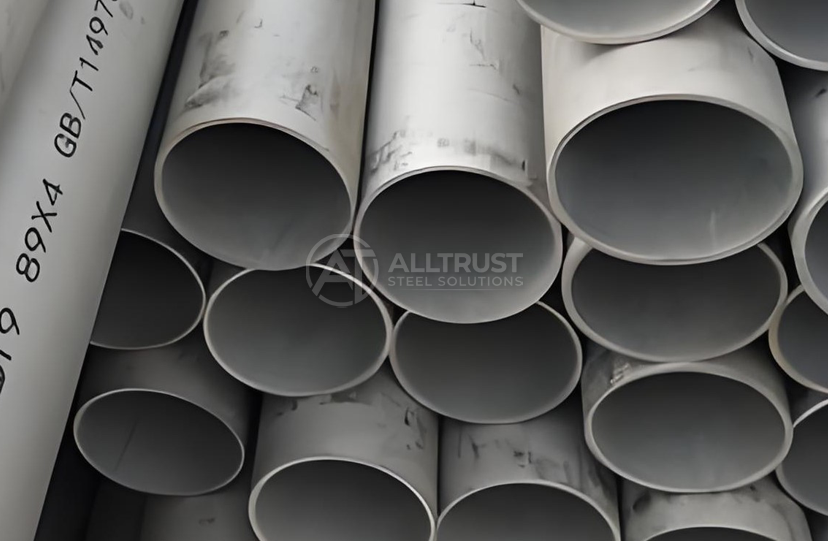
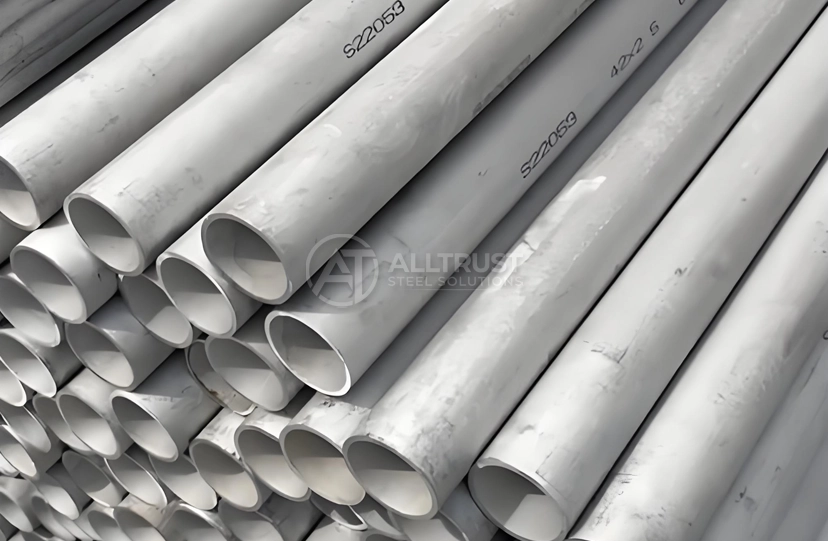
astm a358 tp316l pipe
2. Standard: ASTM A358 / ASME SA358, the premier specification for electric-fusion-welded heavy-duty corrosive pipelines
3. Process: Electric Fusion Welded (EFW) utilizing premium heavy plates and automated multi-pass double-sided joints with filler metal
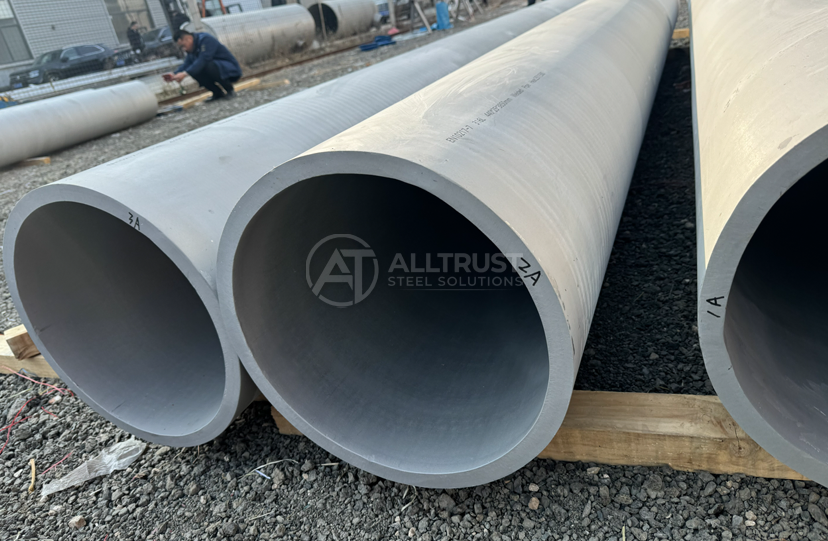
4. Size Range: Large diameters from 8" up to 60" (DN200 - DN1500), wall thicknesses precisely calibrated to engineering schedules
5. Heat Treatment: Post-weld global solution annealing followed by rapid uniform quenching to fully homogenize alloy and weld line distribution
6. Surface Finish: Thoroughly clean acid-pickled and passivated, with inside weld reinforcement strictly level to prevent fluid turbulence
7. Application: Coastal desalination plants, marine offshore platforms, sewage disposal networks, and heavy chemical reactors
8. Service Advantage: 100% X-ray radiographic inspection (RT) on welds per ASME Section VIII Class 1/Class 2, TUV/SGS/BV audits accepted
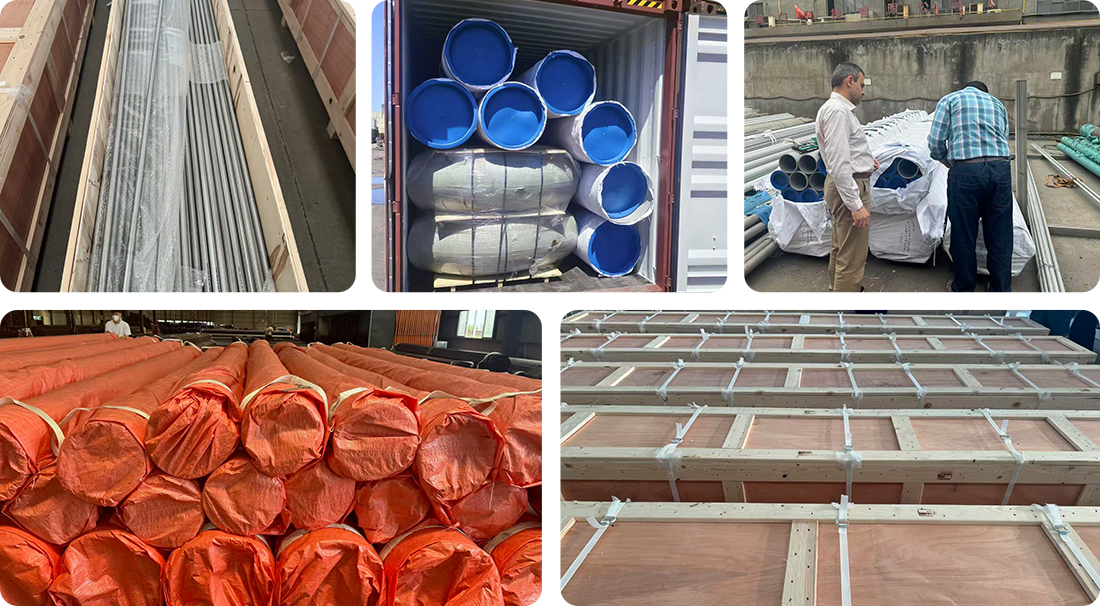
9. Packaging: Secure sea-freight packing with heavy plastic end-caps, bundled or loaded with reinforced steel cradles and lifting slings
10. Key Advantage: Offers absolute defense against chloride pitting while entirely preventing intergranular decay across massive welded seams
ASTM A358 TP316L Pipe - Large Diameter Corrosion-Resistant Solutions for Marine & Chemical Industries
Hebei All Trust Steel Co., Ltd manufactures premium astm a358 tp316l pipe with an annual production capacity exceeding 15,000 tons, featuring diameters up to 1016 mm and 100% radiographic testing compliance. Our electric-fusion-welded pipe uses extra-low carbon chemistry (≤0.03% C) and 2-3% molybdenum integration to eliminate weld-decay sensitisation in heavy-duty seam joints. Each batch undergoes post-weld solution annealing at regulated temperatures with fast quenching in water to ensure total microstructural uniformity. With more than 5,000 tons of rolling inventory, we can supply stock orders in 3-5 days, with EN 10204 3.1/3.2 Mill Test Certificates and third party SGS/TUV witness inspection assistance.
What Makes ASTM A358 TP316L Pipe Essential for Corrosive Environments?
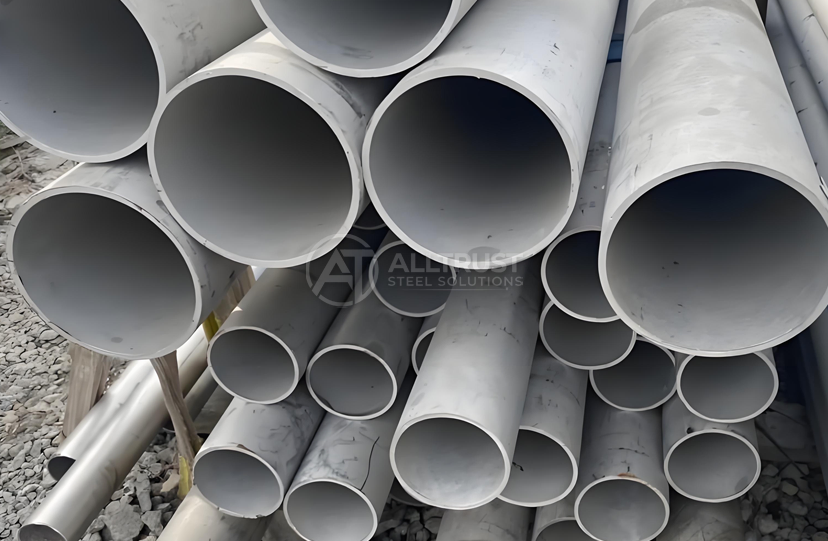
The product is austenitic stainless steel pipe, electric-fusion-welded, designed especially for high-pressure corrosive duty. The designation TP316L means that the material is a standard 316 alloy with an extra-low carbon content of a maximum of 0.03%. This regulated chemistry avoids carbide precipitation during thermal cycling.
Offers essential protection against intergranular corrosion in the heat-affected zones of welds. The inclusion of molybdenum (2-3%) gives excellent resistance to chloride pitting and crevice corrosion. This makes the material suitable for maritime conditions and for chemical processing systems.
The welded architecture is plate formed so that large diameters may be economically manufactured, rather than small-bore seamless alternatives. Pipes with the precision calibrated wall thicknesses from 8 inches to 60 inches (DN200-DN1500) may be specified. The electric fusion welding technology provides better dimensional precision and homogeneity of wall thickness.
There are five grades of ASTM A358 depending on radiographic inspection levels and welding methods. Class 1 must be doubly welded and 100% radiographed, while Class 5 may be single welded with spot inspection. This gives you the ability to choose the level of inspection according to your pressure and safety needs.
Technical Specifications & Standards
| Parameter | Specification |
|---|---|
| Standard | ASTM A358 / ASME SA358 / ASTM A312 / EN 10217-7 |
| Product Type | Electric-Fusion-Welded (EFW) Stainless Steel Pipe |
| Material Grade | TP316L (UNS S31603 / 1.4404 / Extra Low Carbon) |
| Manufacturing Process | Electric-Fusion Welding / Double-Welded Longitudinal Seam |
| Outer Diameter | 8" - 100" (219.1 mm - 2540 mm) |
| Wall Thickness | SCH 5S / SCH 10S / SCH 40S / SCH 80S (2.0 mm - 50 mm) |
| Length | 5.8 m / 6 m / 11.8 m / 12 m / Custom Cut |
| Surface Finish | Solution Annealed & Pickled / X-Ray Cleaned / Polished |
| End Type | Plain End (PE) / Beveled End (BE) / Flanged End |
| Tensile Strength | ≥ 485 MPa (70 ksi) |
| Yield Strength | ≥ 170 MPa (25 ksi) |
| Elongation | ≥ 35% |
| Chemical Composition | Cr: 16-18% / Ni: 10-14% / Mo: 2-3% / C: ≤ 0.03% |
| NDT | 100% Radiographic Test (RT) / Hydrostatic Test / UT / PT |
| Quality Certificates | EN 10204 3.1 & 3.2 MTC / ISO 9001:2015 / CE / PED |
| Third-Party Inspection | SGS / BV / TUV / DNV / ABS Accepted |
Core Advantages of Our Manufacturing Process
Material Excellence & Corrosion Defense
Our product utilizes 100% virgin stainless steel plate with guaranteed molybdenum content. The extra-low carbon chemistry (maximum 0.03%) completely prevents sensitization during welding operations. You receive absolute defense against chloride pitting in seawater applications and intergranular attack in thermal cycling conditions.
The regulated nickel-chromium-molybdenum balance gives excellent resistance to sulfuric acid, acetic acid, phosphoric acid and organic solvents. Your pipe system stays structurally sound even in high temperature and severe chemical environments.
Advanced EFW Production Technology
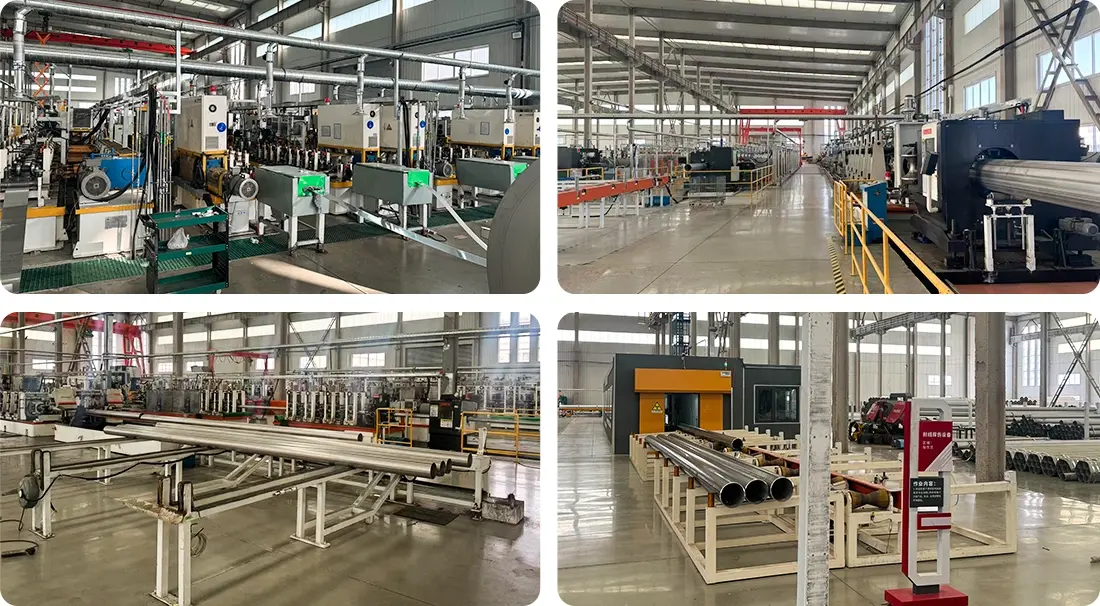
We employ computerized multi-pass welding systems with automated filler metal control. The double-sided longitudinal seam creates fusion quality equivalent to base metal properties. Post-weld solution annealing at 1040-1120°C followed by rapid water quenching ensures complete carbide dissolution.
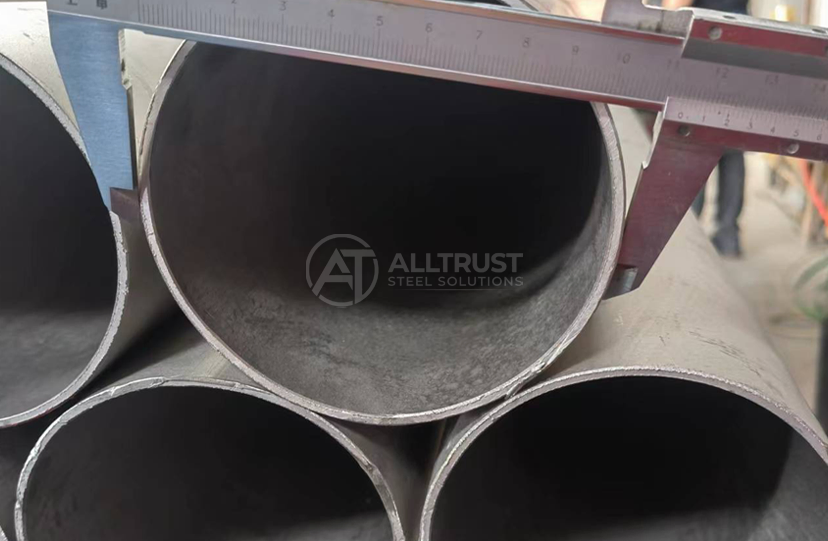
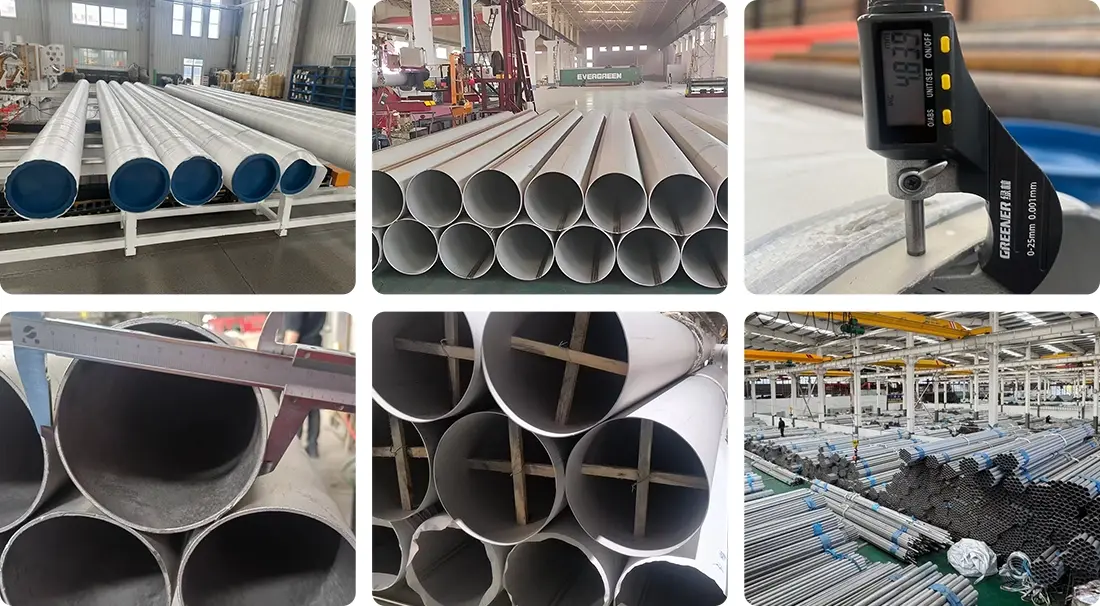
Our laser micrometre dimensional tracking devices are accurate to +/-0.05mm in wall thickness. You have better roundness and concentricity across the whole length of the pipe, which makes field installation easier, and there are fewer fitting difficulties.
Comprehensive Quality Verification
Every production batch undergoes 100% radiographic examination per ASME Section V standards. We perform continuous automated eddy current scanning to detect surface discontinuities. High-pressure hydrostatic testing validates structural integrity at 1.5 times design pressure.
Intergranular corrosion testing per ASTM A262 Practice E confirms weld zone resistance. Transverse tension tests and guided-bend weld tests verify mechanical properties meet or exceed base metal specifications. You receive complete material traceability with heat number documentation.
Industrial Applications & Performance Scenarios
Seawater Desalination & Marine Engineering
Your coastal desalination facilities need plumbing that can handle high concentrations of chloride brine. Our astm a358 tp316l pipe is proven in reverse osmosis feed systems, brine discharge lines and seawater cooling networks. Molybdenum presence reduces localised corrosion in oxygen rich marine conditions.
The material has an advantage for marine atmospheric corrosion on offshore oil and gas sites. You specify big diameter risers and process pipework that take corrosion in stride, even with constant exposure to seawater spray.
Chemical Processing & Pharmaceutical Manufacturing
Your reactor vessels and transfer lines for sulfuric acid, nitric acid and organic solvents and the like need materials that will not contaminate the product. This low-carbon chemistry prevents carbide precipitation that might trap microorganisms or jeopardise product quality.
Pulp and paper bleaching systems utilize this pipe for chlorine dioxide and sodium hypochlorite transport. You achieve long service life even with highly oxidizing bleaching agents at elevated temperatures.
Oil & Gas Refining Infrastructure
Hydrocracking units and catalytic reformers operate under extreme pressure and temperature conditions. Our EFW pipe construction provides the dimensional stability and weld integrity required for these critical applications. You gain confidence from 100% radiographic verification of every longitudinal seam.
Customization Capabilities & Value-Added Services
We provide specialized edge preparations including beveled ends for butt welding, roll-grooved ends for mechanical coupling systems, and flanged ends matching ASME B16.5 specifications. Fixed-length cutting eliminates field waste and reduces installation time.
Our advanced processing capabilities include laser hole drilling for branch connections, slot cutting for instrumentation ports, and precision pipe bending to match your isometric drawings. You receive ready-to-install components that accelerate project completion.
Custom surface finishes are available, including electropolished interiors for pharmaceutical applications and color PVD coatings for identification purposes. We support mixed container loading with coordinating pipe fittings, flanges, and valves to optimize logistics costs.
Quality Documentation & Compliance Support
Every shipment includes EN 10204 3.1 or 3.2 Mill Test Certificates documenting chemical composition and mechanical properties. PMI reports verify alloy composition at multiple pipe locations. We provide radiographic film records or digital RT images for your permanent quality files.
Our manufacturing facilities welcome third-party witness inspections from SGS, TUV, DNV, ABS, or Lloyd's Register. You can schedule hold points for dimensional verification, NDT observation, and hydrostatic testing witnessing.
We supply complete customs documentation including Certificates of Origin, commercial invoices, packing lists, and shipping instructions. Our team assists with technical data sheets, material safety data sheets, and compliance declarations for project-specific requirements.
FAQ
Q:Why does this heavy-duty marine-grade product deliver elite protection inside coastal networks?
A:This pipe combines an extra-low carbon chemistry with heavy molybdenum integration to completely eliminate weld-decay sensitization. You receive definitive defense against localized crevice corrosion in deep-sea offshore operations and chloride-rich environments.
Q:What advanced manufacturing loops secure the microstructural parameters of this large-bore pipe batch?
A:Every production batch is plate-form rolled and welded via high-precision multi-pass automated lines. Post-weld processing includes full solution annealing at controlled temperatures followed by rapid uniform water-quenching treatments. This ensures complete carbide dissolution and microstructural homogeneity.
Q:What strict leak-detection testing matrix is enforced to validate the structural safety of this large-diameter lot?
A:Every production batch undergoes continuous automated internal eddy current scanning loops and laser-micrometer dimensional tracking. High-pressure hydrostatic leakage pressure validation confirms structural integrity before shipment.
Q:Can this low-carbon molybdenum pipe line be customized with standard configurations for mechanical coupling systems?
A:Yes, we provide specialized edge configurations including roll-grooved end preparations for mechanical coupling rings and flanged end adjustments matching your blueprints. Custom beveling angles accommodate specific welding procedures.
Q:What leading international auditing bodies certify the manufacturing parameters of this low-carbon EFW line?
A:Our advanced EFW mills maintain ISO 9001:2015 quality management certification and fully welcome independent witness inspections from third-party firms like SGS, TUV, DNV, ABS, or Lloyd's Register.
Contact Us
Ready to secure corrosion-resistant piping for your next project with the astm a358 tp316l pipe? Contact our technical team at info@hballtrust.com for material selection guidance, CAD drawing verification, and competitive quotations.