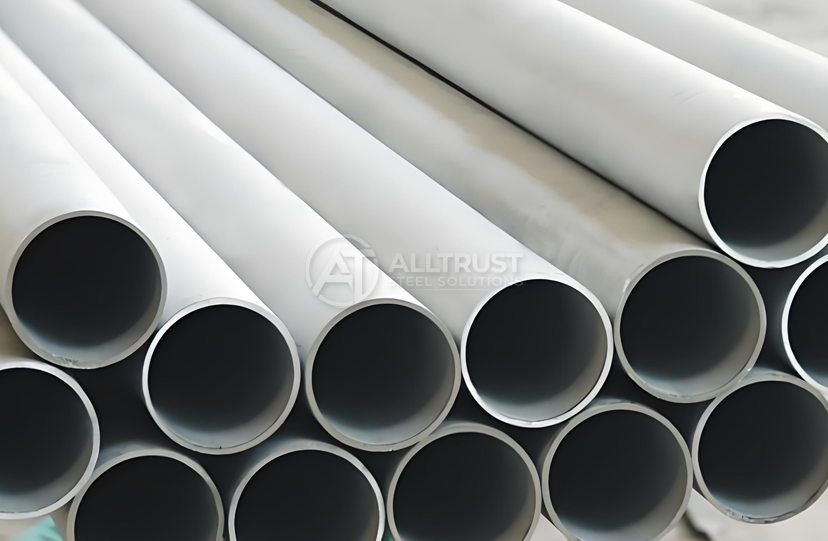
astm a376 boiler pipe
2. Standard: ASTM A376 / ASME SA376, the standard specification for heavy-duty boiler systems
3. Process: 100% seamless heavy-wall construction, designed to withstand continuous internal steam pressure
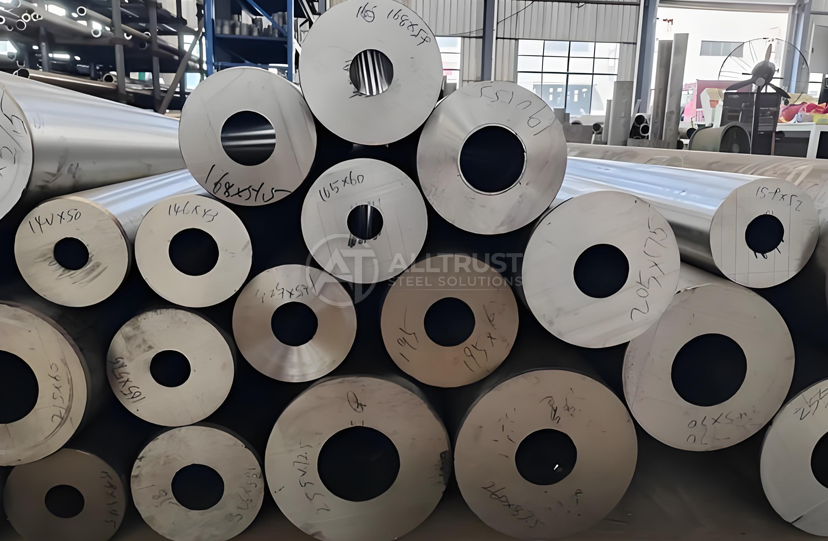
4. Size Range: Tailored for boiler tubes, available in diverse outside diameters and heavy wall thicknesses
5. Heat Treatment: Precise high-temperature solution annealing to secure excellent grain size refinement
6. Surface Finish: Thoroughly descaled and acid-passivated to maintain maximum heat transfer efficiency
7. Application: Power plant boilers, superheaters, reheater tubes, and high-temperature steam loops
8. Service Advantage: 100% Hydrostatic and Eddy Current tested, third-party inspection (SGS/BV) welcome
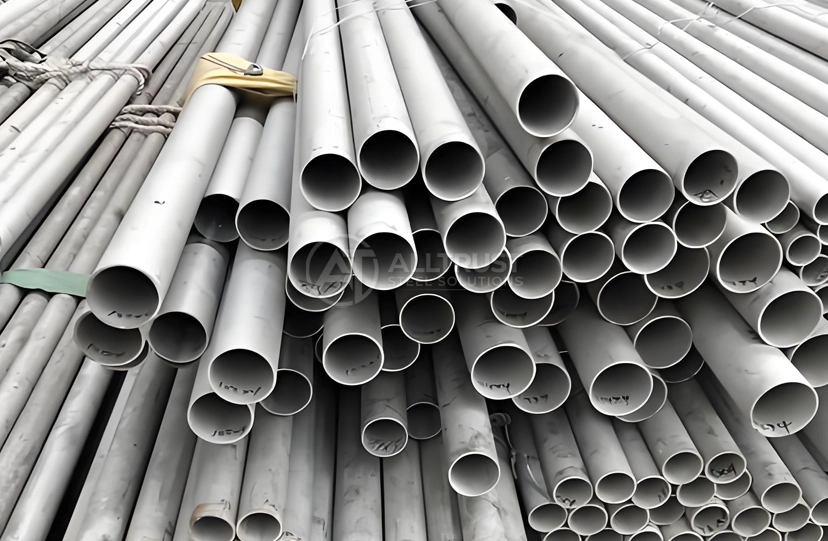
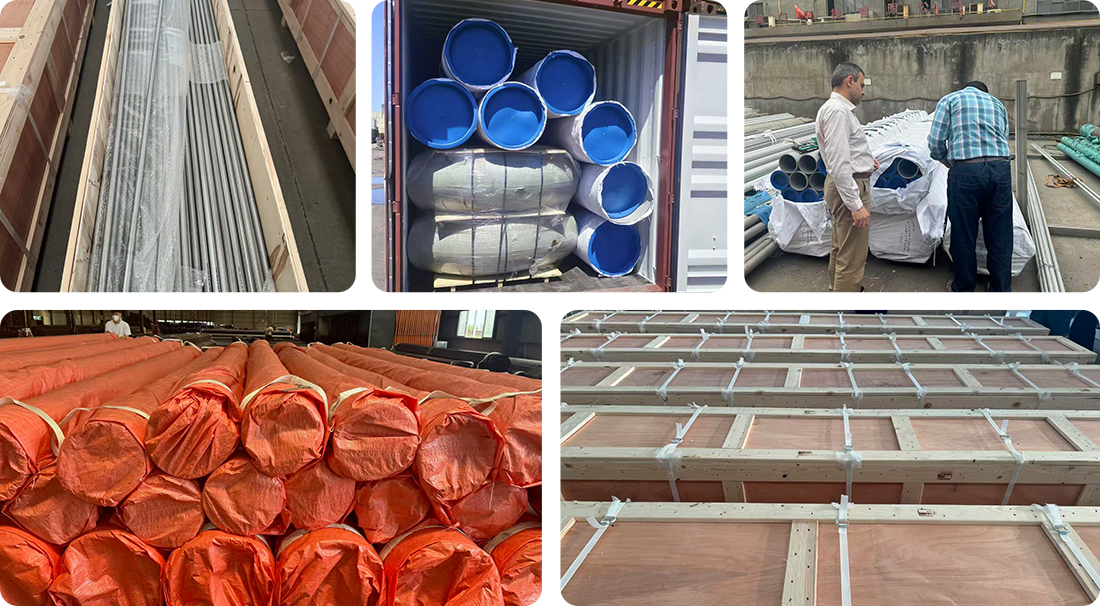
9. Packaging: Packed in fumigated wooden boxes or steel frames to prevent bending during long shipping
10. Key Advantage: Exceptional creep-rupture strength and anti-oxidation performance under prolonged heating
ASTM A376 Boiler Pipe for High-Temperature Power Plant Systems – Premium Seamless Austenitic Solutions
The industrial power generation sector demands extraordinary materials. ASTM A376 boiler pipe represents the pinnacle of seamless austenitic steel engineering for high-temperature central-station service. Hebei All Trust Steel Co., Ltd manufactures precision-grade boiler pipes meeting ASTM A376/ASME SA376 specifications, has a yearly capacity of over 15,000 tonnes and 100% of hydraulic testing. Our specialised high carbon grades TP304H, TP316H, TP321H and TP347H provide and enjoy remarkable creep-rupture strength at temperatures above 538°C (1000°F) for ultra-supercritical power plants, petrochemical reheaters and steam production facilities globally. All pipe is subjected to strict grain size verification, eddy current testing and solution annealing, to provide maximum thermal durability under continuous steam pressure circumstances.
Why ASTM A376 Boiler Pipe Stands Apart in Power Generation
This specific standard aims to overcome crucial problems that cannot be solved by stainless pipes for ordinary use. In power plants working at extraordinary pressures ( 30 MPa ) and temperatures ( over 600°C ) , conventional materials fail via creep deformation . Creep is the gradual disintegration of a structure under continuous heat stress .
It overcomes this challenge via controlled metallurgy. The high carbon 'H' grades have 0.04-0.10% carbon which considerably improves long term strength. Niobium and titanium elements stabilise it therefore preventing intergranular corrosion in the key regions of the welds.
The structure is seamless, eliminating the risk of weld seam weaknesses altogether. The homogeneous cylinder construction results in uniform thermal expansion of the pipe body. Your facility prevents catastrophic failures that may cost millions in lost time.
Unlike general-purpose ASTM A312 pipes, our A376 series requires grain size testing and must be tested under ASTM E112. The coarser grain structure (ASTM No. 7 or bigger) gives better resistance to thermal creep over decades of operation.
Technical Specifications & Available Grades
| Parameter | Specification |
|---|---|
| Standard | ASTM A376 / ASME SA376 / EN 10216-5 |
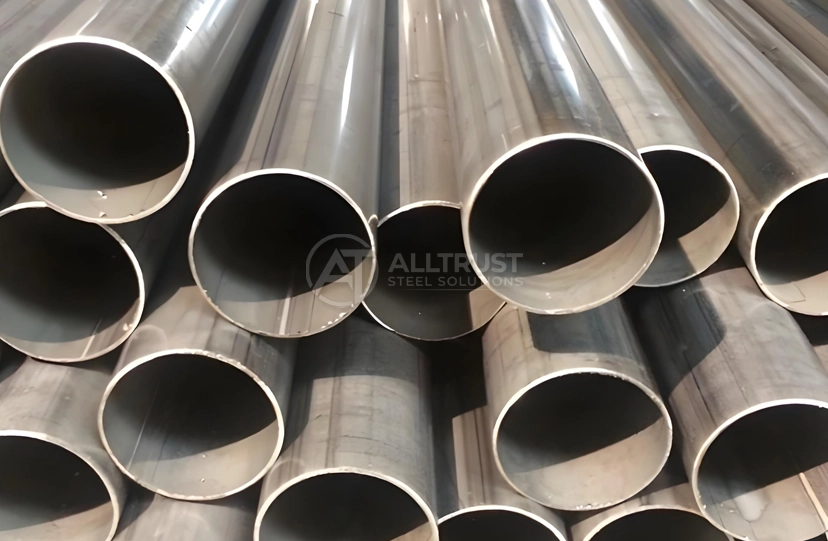
| Product Type | Seamless Austenitic Boiler Pipe |
| Material Grades | TP304H, TP316H, TP321H, TP347H |
| Manufacturing Process | Hot Finished / Cold Drawn Seamless |
| Outer Diameter | 21.3 mm – 609.6 mm (1/2" – 24") |
| Wall Thickness | SCH 10S to SCH XXS (2.0 mm – 50.0 mm) |
| Standard Length | 5.8 m / 6 m / 11.8 m / 12 m / Custom |
| Heat Treatment | Solution Annealed & Pickled |
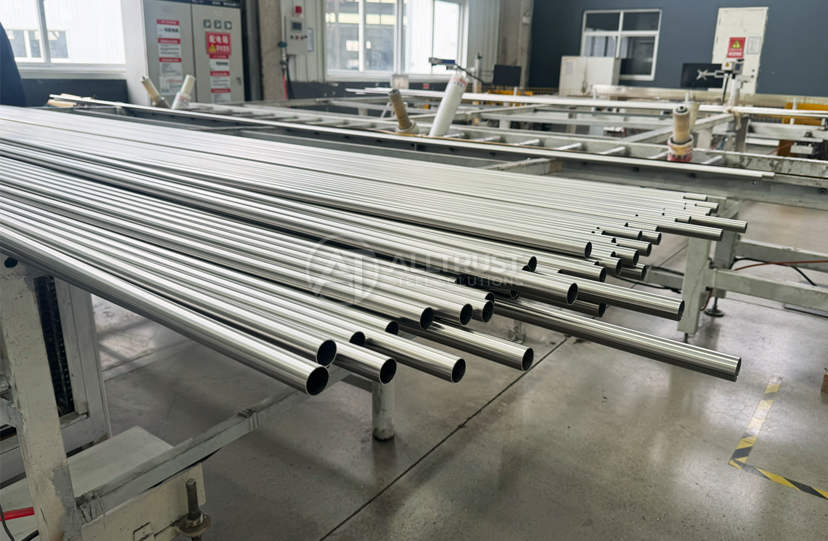
| Surface Finish | Descaled, Acid-Passivated, Shot Blasted |
| End Type | Plain End (PE) / Beveled End (BE) |
| Testing | 100% Hydrostatic, Ultrasonic, Eddy Current |
| Certifications | EN 10204 3.1/3.2 MTC, ISO 9001:2015, PED |
Critical Applications Requiring ASTM A376 Performance
Ultra-Supercritical Power Plants
Modern USC facilities need materials that preserve integrity under high conditions. Our product is used for major steam headers where pressure is 30 MPa and temperature is 600°C. The austenitic structure can withstand high-pressure rupture and temperature cycling during start-up and shut-down operations.
Superheater and Reheater Assembly
In the case of central-station boilers, dry steam flows through the superheater tubes at speeds in excess of 30 m/sec. These circumstances lead to erosion problems paired with exterior corrosion due to exhaust gases. Our pipes have a chromium-rich oxide layer, which defends against both attack modalities and yet allows effective heat transmission.
Heat Recovery Steam Generator (HRSG)
HRSG systems are used in combined-cycle plants where steam is produced from the exhaust gases of the combustion turbine. The fast temperature changes need good thermal fatigue resistance. This makes the grain boundaries weaker. We have stabilised grades like TP321H and TP347H which avoid carbide precipitation.
Chemical Composition Advantages Material Excellence & Manufacturing Precision
Your power generating equipment demands certified metallurgy. Each batch comprises 17-20% chromium for resistance to oxidation and 8-13% nickel for austenitic stability. The regulated carbon level of the"H" grades provides creep strength with no loss of weldability.
Stabilisation with niobium (TP347H) or titanium (TP321H) inhibits sensitisation, a problematic situation when chromium carbides develop at grain boundaries during heating. This protection is vital when your pipes are subjected to temperatures ranging from 800°F to 1500°F over extended periods of time.
Mechanical Properties at Elevated Temperature
At room temperature, these pipes exhibit minimum tensile strength of 515 MPa (75 ksi). But the true test comes at operating temperature. Our astm a376 boiler pipe maintains sufficient yield strength at 600°C to resist pressure-induced expansion.
The ASTM A376 specification of coarse grain structure directly improves creep-rupture performance. Fine-grained materials tend to break down quicker under prolonged high-temperature stress. Controlled grain size offers the structural integrity your facility needs for 200,000+ working hours.
Smooth Manufacturing Process:
Depending on your size needs we use hot finished or cold drawn processes. Hot finished pipes are good for bigger diameters and heaver walls. Cold-drawn manufacturing offers the tightest tolerances (±0.05 mm) for precision boiler tube applications.
Each pipe is solution annealed at prescribed temperatures, typically 1040-1150C depending upon the grade. This heat treatment dissolves the carbide and homogenises the microstructure. The rapid cooling retains the austenitic phase but eliminates the residual stresses from the forming procedures.
Comprehensive Quality Control & Testing
Non-Destructive Examination
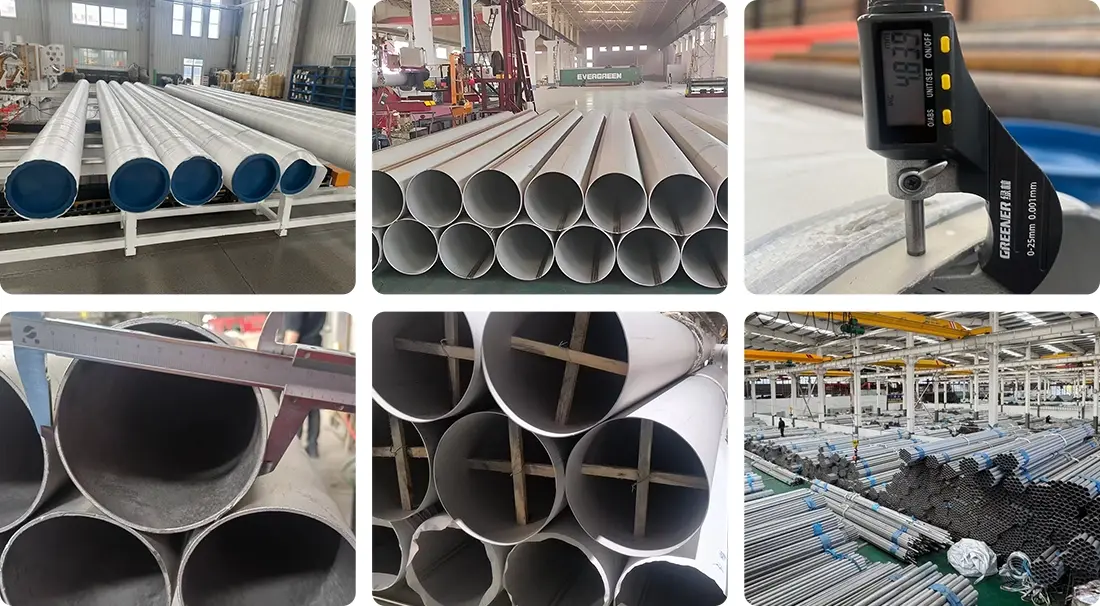
We use 100% eddy current inspection to find surface and near surface faults. This electromagnetic approach may detect fractures, pits or inclusions which are not detectable by optical examination. Ultrasonic testing detects internal soundness across the whole wall thickness.
Hydrostatic testing subjects each pipe to pressures exceeding service conditions. This pneumatic proof load confirms pressure-containing integrity before shipment to your facility.
Mechanical Qualification Tests
Representative samples undergo destructive testing to verify mechanical properties. Flattening tests assess ductility—pipes must withstand compression between parallel plates without cracking. Flaring tests expand pipe ends to verify formability for field installation.
High temperature tensile tests at service temperature indicate that the yield and ultimate strengths fulfil specification criteria. Creep tests consist on applying a constant force to a sample at high temperature and measuring the deformation over a few thousand hours .
Grain Size Check
This important parameter influences creep resistance directly. Metallographic inspection is performed in accordance with ASTM E112 and average grain size is shown on mill test certificates. For high-temperature service grades, your quality team may check that the grain structure is ASTM No. 7 or coarser.
Chemical Analysis & PMI
X-ray fluorescence Positive Material Identification (PMI) validates alloy composition is as specified. We provide detailed ladle chemistry for chromium, nickel, molybdenum, carbon, nitrogen and stabilising elements. This traceability guaranties you obtain the correct grade that you need for your application.
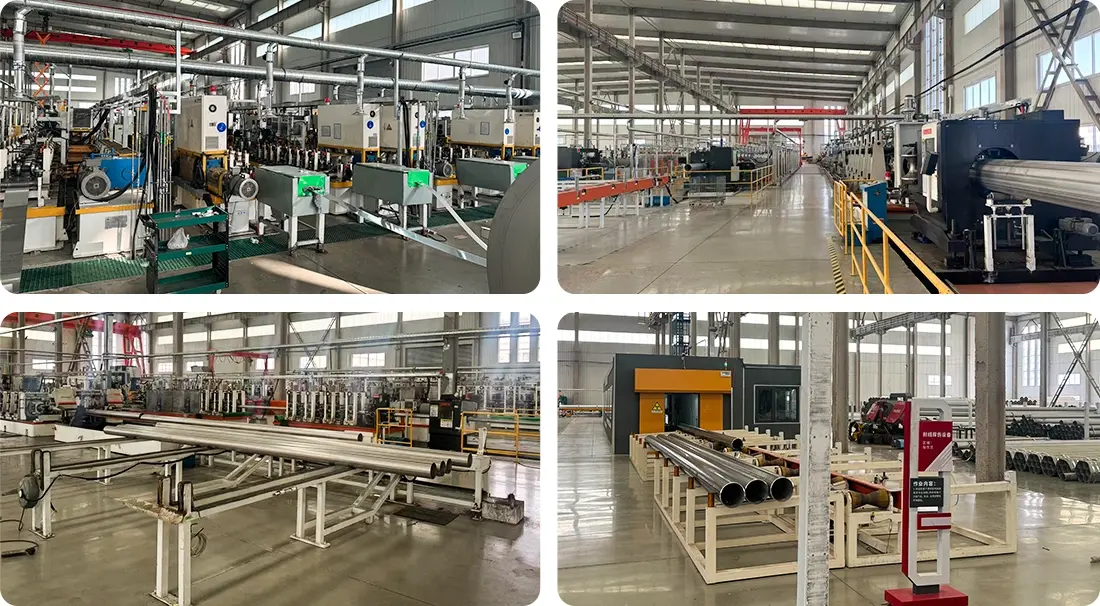
Customization Capabilities for Complex Projects
Your boiler systems have unique configuration requirements. We provide custom length cutting from 500 mm to 12 meters, eliminating field waste. Beveled ends machined to ASME B16.25 specifications simplify welding preparation on site.
For specialized heat exchanger applications, we offer precision cold-drawn tubes with outer diameter tolerances of ±0.05 mm. Wall thickness consistency ensures uniform heat transfer across your entire tube bundle.
Shot blasting provides a uniformly roughened surface that enhances adhesion for thermal spray coatings or improves heat transfer characteristics. This surface preparation also removes any residual scale missed during pickling operations.
Threading services add NPT or other connection types directly at our facility. Pre-threading reduces installation time and ensures consistent thread quality across large pipe orders.
Packaging & Global Logistics Solutions
Power plant projects operate on strict timelines. We maintain over 5,000 tons of rolling inventory covering common grades and sizes. Stock items ship within 3-5 days of order confirmation.
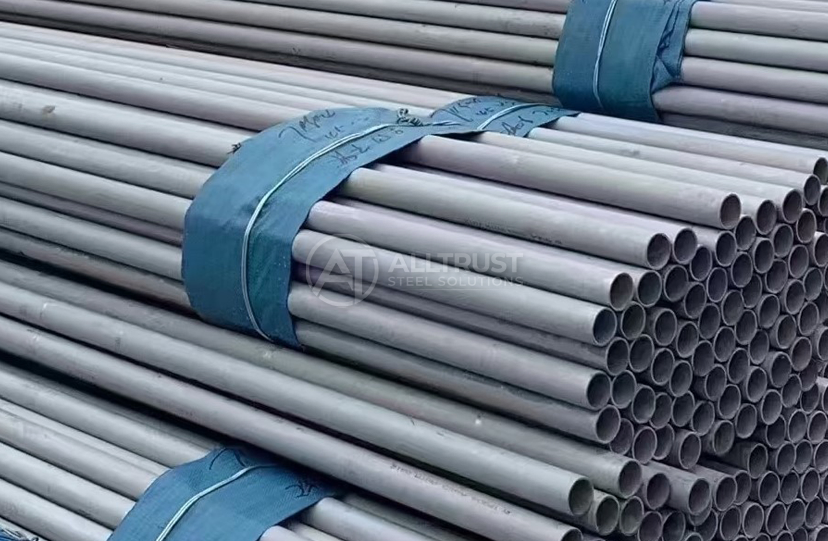
Your investment is safe with our export packing for international transportation. Each plastic cap individually seals the end of the pipe to avoid contamination. Heavy durable plywood carton prevents bending damage when handled. Hexagonal bundles are wrapped in waterproof material to protect them from moisture and salt spray during maritime shipment.
We ship from main ports in China, such as Shanghai, Ningbo, Tianjin, Qingdao. The mixed container loading mixes pipes with fittings, flanges and valves to optimise your shipping expenses. Trade terms available include FOB, CFR, CIF, DDP as per your purchase option.
Every shipment is accompanied by full paperwork including EN 10204 3.1 Mill Test Certificates, Certificates of Origin, Commercial Invoices and Packing Lists. This paper work will help you clear at the port of your destination.
FAQ
Q:What core thermal capabilities make this product critical for steam generation infrastructure?
A:This specialized pipe delivers outstanding creep-rupture strength and reliable thermal stress absorption in extreme subcritical and supercritical boiler environments. The high-carbon 'H' grade chemistry provides mechanical stability at temperatures exceeding 538°C where general-purpose stainless steel would fail through creep deformation.
Q:Why is seamless structure mandated for this severe utility pressure line?
A:The seamless piercing process creates a completely uniform cylinder cross-section free of weld vulnerabilities. This eliminates the weakest point in welded pipes where heat-affected zones are prone to failure. Seamless construction ensures uniform thermal expansion and prevents sudden mechanical rupture under intensive heat loops.
Q:What destructive quality verification benchmarks must this boiler pipe batch successfully pass?
A:Representative production samples undergo severe mechanical flattening trials testing ductility, cross-sectional flare expansion tests verifying formability, and precise Positive Material Identification (PMI) confirming chemical grade accuracy. High-temperature tensile testing and creep-rupture analysis validate long-term strength at service temperature.
Q:Can this boiler pipe series be customized with specialized edge configurations for multi-pass joints?
A:Absolutely. We support extensive custom fabrication including precision compound beveled angles per ASME B16.25 codes. Fixed or random length structures extend up to 12 meters. Threading, laser hole drilling, and slot cutting accommodate complex header configurations in your boiler design.
Q:What material documentation is provided to verify precise material traceability?
A:Each batch includes EN 10204 3.1 Mill Test Certificates (MTC) detailing exact chemical ladle heat numbers, grain size measurements, mechanical property test results, and heat treatment records. This comprehensive documentation supports your quality management system and regulatory compliance requirements.
Contact Us
Ready to secure premium astm a376 boiler pipe for your next project? Contact our engineering team at info@hballtrust.com for technical specifications, pricing, and delivery schedules tailored to your requirements.