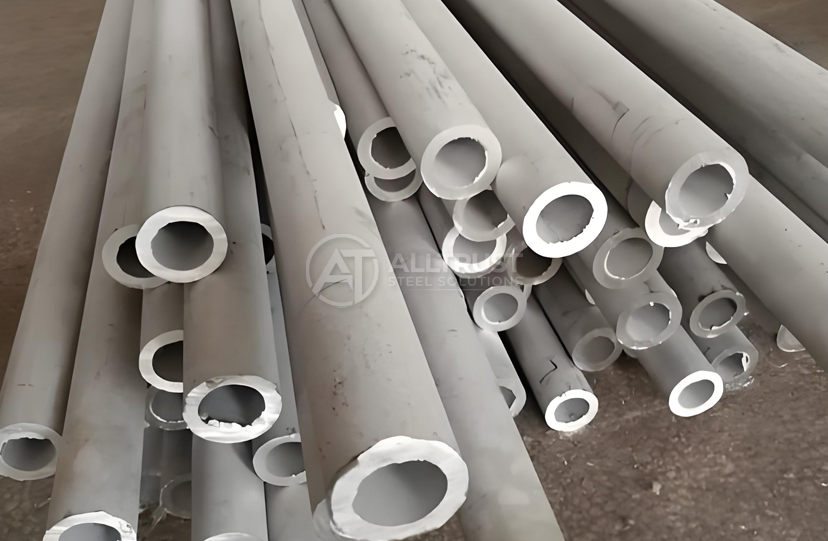
astm a376 tp347h pipe
2. Standard: ASTM A376, the premium choice for extreme stress-rupture thermal service
3. Process: Seamless cold finishing with advanced internal boring to guarantee smooth fluid flow
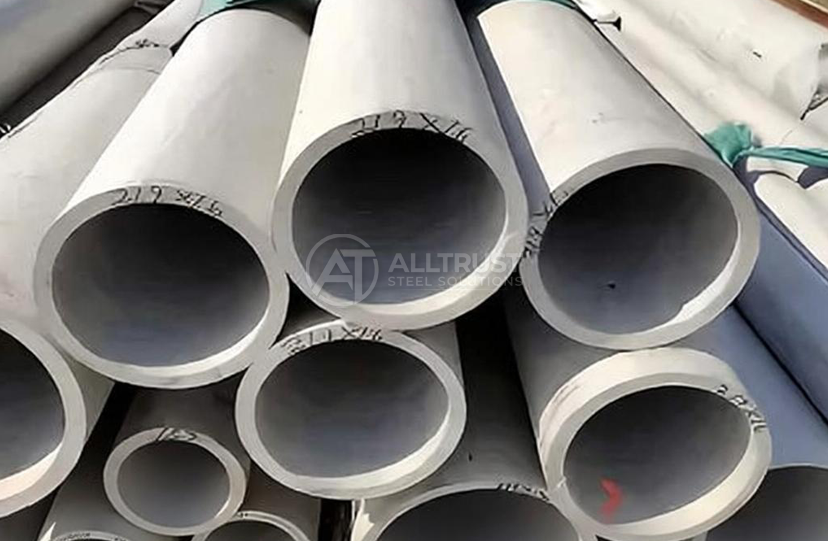
4. Size Range: Standard schedules per ASME B36.19M, available in heavy-wall specifications
5. Heat Treatment: High-temperature solution annealing to optimize grain size and creep behavior
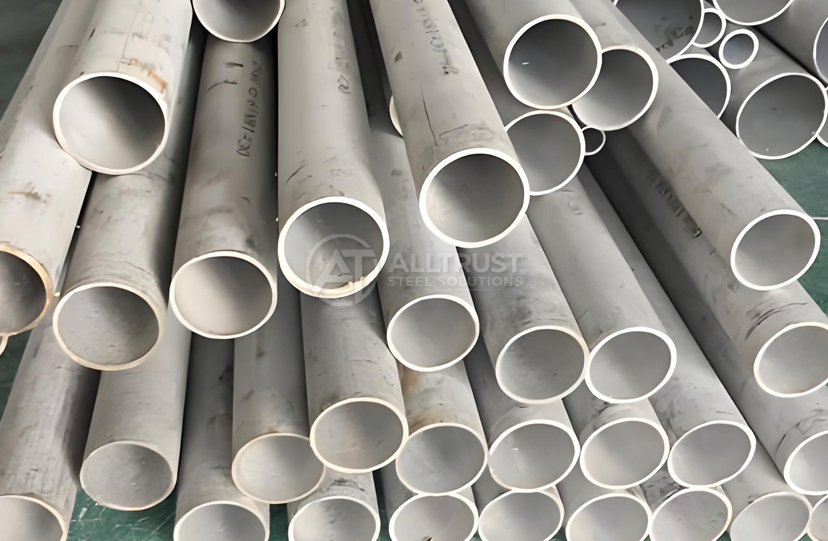
6. Surface Finish: Thoroughly descaled and passivated, free from iron contamination and oxide scale
7. Application: Ultra-supercritical boiler tubes, chemical reactors, and high-heat power piping
8. Service Advantage: Sourced from top-tier raw materials, TUV and SGS testing fully supported
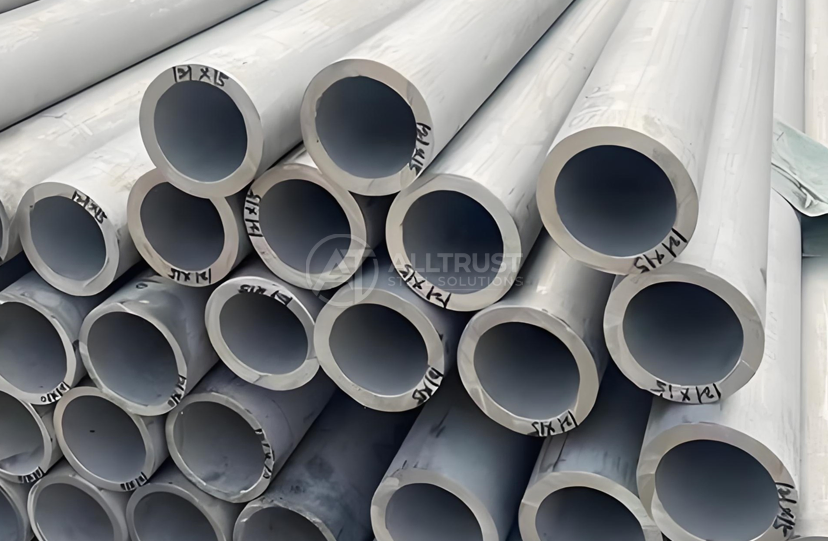
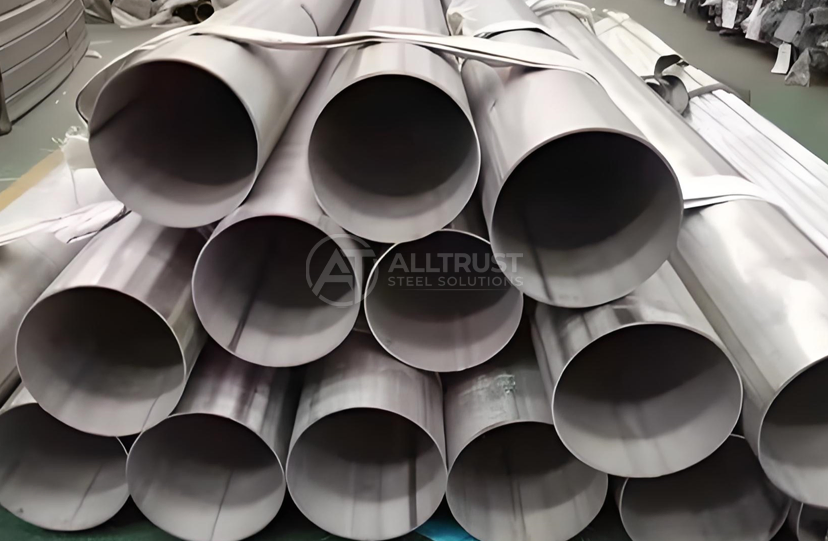
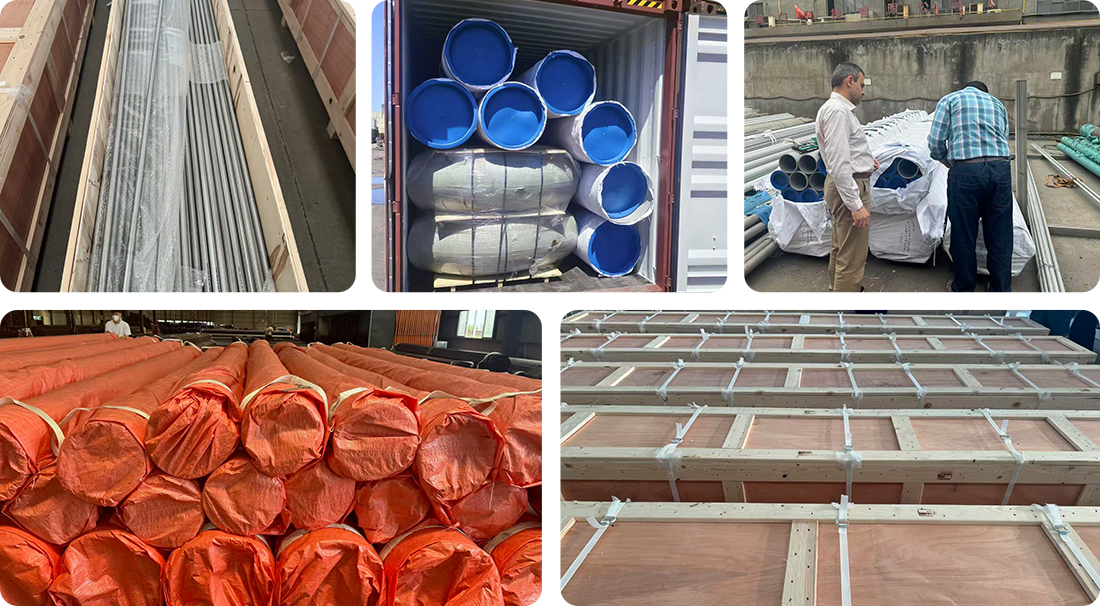
9. Packaging: Bound in seaworthy bundles with steel rings and protective lifting slings attached
10. Key Advantage: Exceptional structural stability and maximum resistance to polythionic acid cracking
ASTM A376 TP347H Pipe – Premium Niobium-Stabilized Stainless Steel Pipe for Ultra-High-Temperature Central Station Service
HEBEI ALL TRUST STEEL CO., LTD manufactures industrial-grade astm a376 tp347h pipe engineered for extreme thermal power applications. Our seamless TP347H pipes are niobium-stabilized austenitic steel tubes that deliver exceptional creep resistance and structural stability in temperatures up to 815°C. With an annual production capacity exceeding 15,000 tons and 100% hydraulic testing coverage, we supply heavy-wall specifications ranging from 21.3 mm to 609.6 mm outer diameter. Every batch undergoes mandatory solution annealing above 1050°C, full-length ultrasonic testing, and grain size verification to guarantee zero sensitization risk in high-stress power generation environments.
What Makes TP347H the Superior Choice for High-Temperature Boiler Applications?
The product addresses critical failure modes in ultra-supercritical boiler systems through advanced metallurgical stabilization. Standard austenitic grades suffer grain boundary carbide precipitation during prolonged exposure to 425–815°C service ranges. This sensitization causes catastrophic intergranular corrosion and polythionic acid stress cracking.
TP347H solves this through controlled niobium addition. The columbium element forms stable NbC carbides that prevent chromium depletion along grain boundaries. Combined with elevated carbon content (0.04–0.10%), this grade maintains structural cohesion under continuous thermal cycling.
Your power plant benefits from three decisive advantages. First, extended service life in superheater and reheater zones where metal temperatures exceed 650°C. Second, reliable performance in post-weld conditions without supplementary heat treatment. Third, proven resistance to polythionic acid cracking during shutdown maintenance cycles when sulfur-bearing deposits encounter moisture.
Technical Specifications of ASTM A376 TP347H Pipe
| Parameter | Specification |
|---|---|
| Material Grade | TP347H (UNS S34709) |
| Manufacturing Standard | ASTM A376 / ASME SA376 / EN 10216-5 |
| Process Type | Hot Finished Seamless / Cold Drawn Seamless |
| Outer Diameter Range | 21.3 mm – 609.6 mm (1/2" – 24") |
| Wall Thickness | SCH 10S to SCH XXS (2.0 mm – 50.0 mm) |
| Standard Lengths | 5.8 m / 6 m / 11.8 m / 12 m / Custom Cut |
| Heat Treatment | Solution Annealed (Min. 1050°C) + Rapid Cooling |
| Surface Finish | Pickled & Passivated / Shot Blasted |
| End Configuration | Plain End (PE) / Beveled End (BE) |
| NDT Coverage | 100% Hydrostatic + Ultrasonic / Eddy Current |
| Quality Certificates | EN 10204 3.1/3.2 MTC + ISO 9001:2015 |
| Third-Party Inspection | SGS / TÜV / DNV / BV Accepted |
Why HEBEI ALL TRUST STEEL Delivers Unmatched Reliability
Metallurgical Excellence Through Controlled Manufacturing
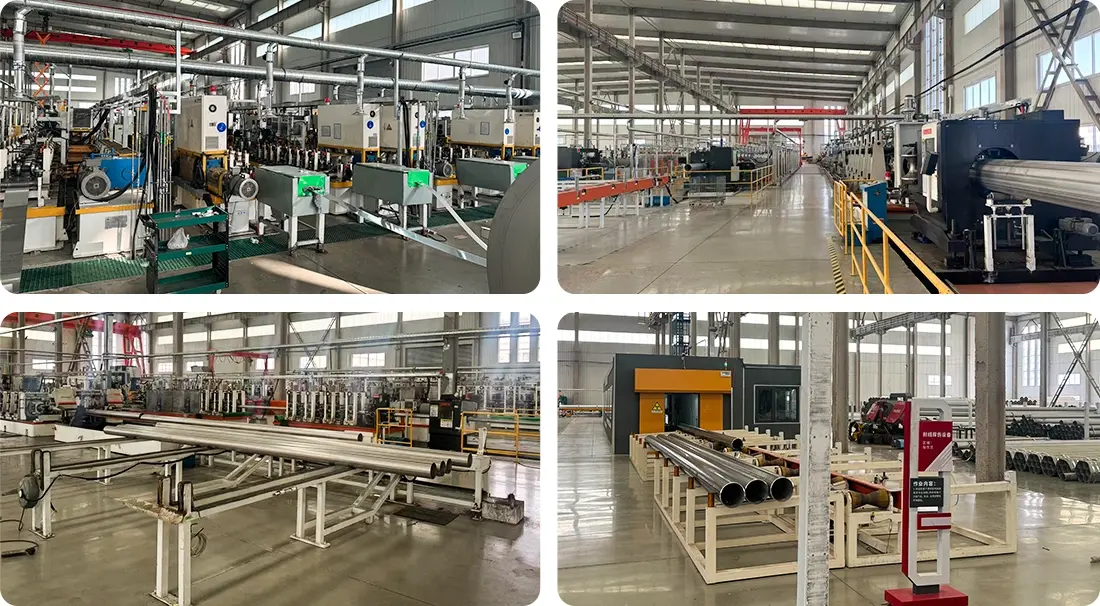
We source virgin stainless steel from 15+ ISO-certified mills with complete heat number traceability. Raw material undergoes spectrographic verification to confirm niobium content between 8x to 10x the carbon percentage—the critical ratio for optimal stabilization.
Our seamless piercing process uses advanced rotary mandrel mills. This eliminates centerline porosity common in welded alternatives. Each pipe receives high-temperature solution annealing with precise soak time control. Rapid water quenching locks the stabilized microstructure before carbide precipitation begins.
Four-Stage Quality Assurance Protocol
Stage 1: Material Verification – PMI analysis confirms chromium (17.0–19.0%), nickel (9.0–13.0%), and niobium compliance before processing.
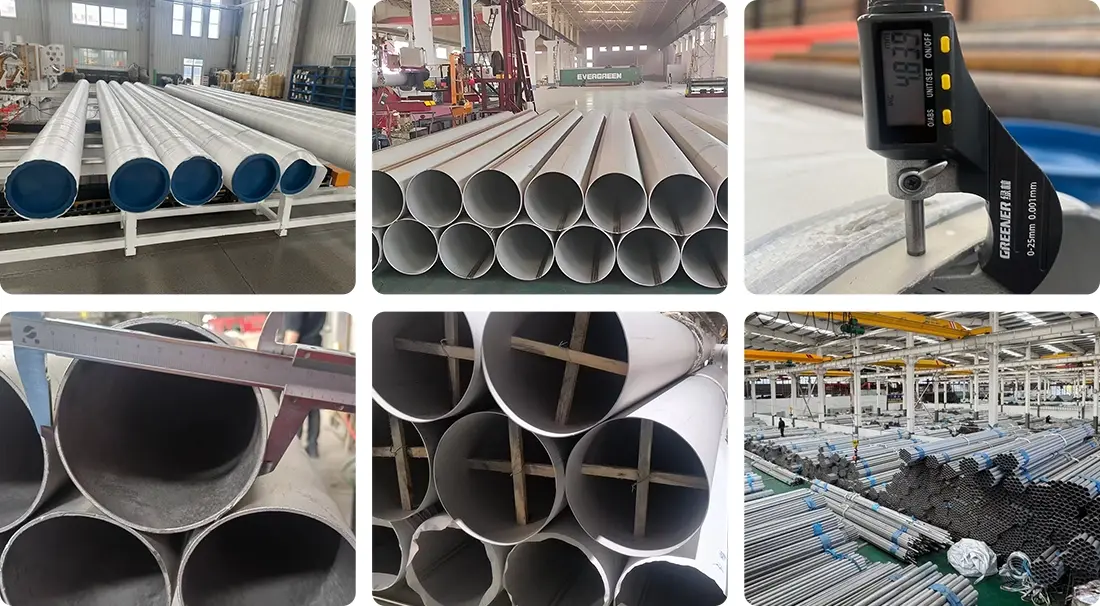
Stage 2: Production Monitoring – Real-time dimensional scanning tracks wall thickness uniformity within ±0.05 mm tolerance. Grain size testing per ASTM E112 ensures No. 7 or coarser structure.
Stage 3: Non-Destructive Examination – Full-length ultrasonic mapping detects subsurface discontinuities above 5% wall threshold. Automated eddy current systems identify surface defects exceeding 0.25 mm depth.
Stage 4: Performance Testing – Every batch undergoes elevated-temperature tensile testing, flattening verification, and intergranular corrosion resistance evaluation per ASTM A262 Practice E.
Custom Engineering for Mission-Critical Projects
Your specifications receive dedicated production scheduling. We provide precision NPT/BSPT threading, ANSI-standard weld beveling, and roll-grooving for mechanical coupling systems. Custom length cutting with ±1 mm accuracy eliminates field modification waste.
Heavy-wall pipes up to 50 mm thickness support extreme pressure ratings in primary steam headers. Our laser marking system applies heat number, grade, and dimensional data per your tracking requirements.
Industrial Applications Where TP347H Delivers Maximum Value
Ultra-Supercritical Power Generation
Central station boilers operating above 580°C steam temperature demand astm a376 tp347h pipe in superheater pendant sections and final reheater stages. The niobium-stabilized structure resists creep deformation during 100,000+ hour service intervals.
Primary reheat piping transports 25 MPa steam through severe thermal gradients. TP347H maintains pressure boundary integrity where standard TP304H grades experience accelerated oxidation and stress rupture.
Petrochemical High-Temperature Processing
Hydrocracking reactor effluent lines handle hydrogen-rich streams at 450–550°C with cyclic pressure fluctuations. The stabilized grain structure prevents hydrogen-induced cracking and maintains ductility through repeated thermal cycles.
Catalytic reformer transfer piping operates in oxidizing atmospheres with sulfur-bearing compounds. TP347H resists external scaling while preventing internal carburization that degrades mechanical properties.
Chemical Reactor Systems
Organic acid production units utilize product in high-temperature heat recovery networks. The material withstands corrosive condensates during shutdown cycles without developing sensitization cracks near weld heat-affected zones.
Pressure vessels operating between 500–800°C benefit from the coarse grain structure's superior creep-rupture strength. This eliminates premature replacement costs associated with fine-grained alternatives.
Comprehensive Support from Inquiry to Commissioning
Our engineering team provides material selection guidance based on your specific operating parameters. We analyze pressure-temperature relationships, corrosive media exposure, and thermal cycling frequency to confirm TP347H suitability.
Technical documentation includes certified MTC with actual chemical analysis, mechanical test results, and heat treatment records. CAD drawing verification ensures dimensional compatibility with your piping layout before fabrication begins.
Container loading optimization reduces shipping costs through strategic bundling. Mixed shipments with matching flanges, fittings, and valves streamline your procurement process.
FAQ
Q:What distinct chemical stabilization prevents this product from grain boundary sensitization at high heats?
A:This pipe incorporates a specialized niobium (columbium) stabilization element paired with an optimized high carbon content, which aggressively thwarts cracks and resists intergranular corrosion up to 815°C thermal extremes.
Q:What advanced manufacturing loops secure the microstructural parameters of this high-carbon seamless line?
A:Extruded and hot-finished through advanced heavy seamless piercing mills under stringent metallurgical parameters, followed by mandatory high-temperature solution treated annealing and rapid uniform cooling.
Q:What precise volumetric inspection diagnostics are carried out on this specific pressure pipe batch?
A:The entire length of the pipe undergoes mandatory 100% volumetric ultrasonic thickness scanning (UT) combined with automated online eddy current diagnostic mapping to eliminate subterranean internal micro-voids.
Q:Can this niobium-stabilized heavy-duty pipe be customized with standard threading configurations for rapid field installation?
A:Yes, we provide flexible machining selections including precision NPT or BSPT taper threading, roll-grooved end preparations for mechanical couplings, and ANSI-standard beveled endings.
Q:In what specific high-stress energy infrastructures is this astm a376 tp347h seamless pipe universally deployed?
A:It is optimized for central station thermal power plants, main steam superheater headers, chemical process cracking units, and high-temperature radiant heater networks.
Contact Us
Contact our technical specialists at info@hballtrust.com for material certification, custom specifications, and competitive pricing. Let us engineer your next critical piping project with proven reliability using the astm a376 tp347h pipe.