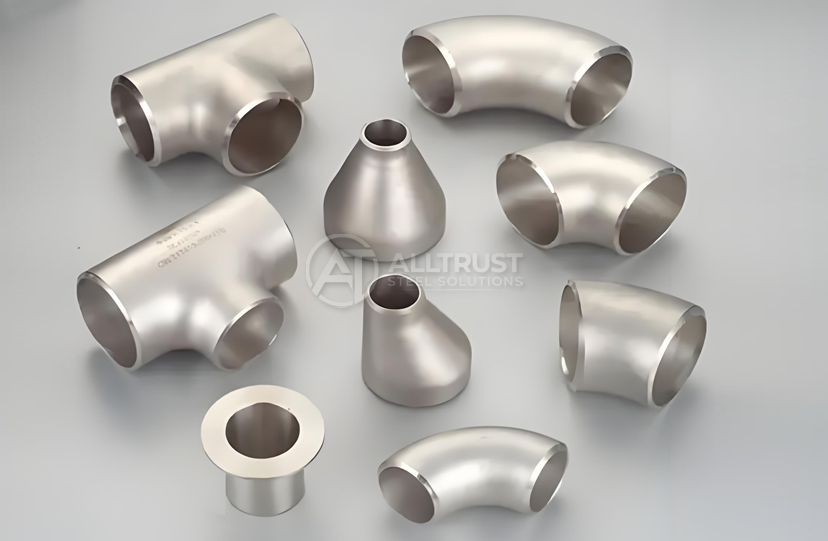
ASTM A403 WP316 WP316L Eccentric Reducer
2. Standard: ASTM A403 / ASME SA403, specific code governing premium wrought stainless steel piping fittings
3. Process: Advanced asymmetric eccentric die pressing, aligning one side completely flat to balance horizontal phase flow
4. Size Range: Calibrated step-down dimensions matching Nominal Pipe Sizes from 1/2" up to major industrial sizes
5. Heat Treatment: Full-body furnace solution annealing to completely eliminate microstructural residual forming stresses
6. Surface Finish: Clean uniform solution annealed and pickled (SA&P), descaled matte, or passivated clean profile
7. Application: Horizontal pump suction intake grids, chemical piping drainage layouts, and marine offshore networks
8. Service Advantage: Sourced from tier-one steel pipes, 100% PMI verified, and full technical MTC 3.1 reports provided
9. Packaging: Secure international crate packing with protective thick dividers to prevent mechanical impact scratches
10. Key Advantage: Flat-bottom configuration perfectly prevents liquid or gas pocket accumulation at horizontal pump inlets
ASTM A403 WP316 WP316L Eccentric Reducer – Premium Marine-Grade Piping Fittings for Corrosive Horizontal Flow Systems
HEBEI ALL TRUST STEEL CO., LTD manufactures premium ASTM A403 WP316 WP316L Eccentric Reducer solutions engineered specifically for horizontal pump suction lines and corrosive marine applications. Our dual-certified fittings feature extra-low carbon molybdenum-bearing austenitic steel with asymmetric flat-side geometry to eliminate vapor lock formation. With an annual production capacity exceeding 15,000 tons and 100% hydraulic testing compliance, we deliver solution-annealed reducers ranging from 1/2" to 48" with complete EN 10204 3.1 MTC documentation. Each product undergoes mandatory PMI verification and radiographic testing to ensure elite crevice corrosion defense in offshore platform seawater systems and pharmaceutical WFI circuits.
Understanding ASTM A403 WP316 WP316L Eccentric Reducer Construction
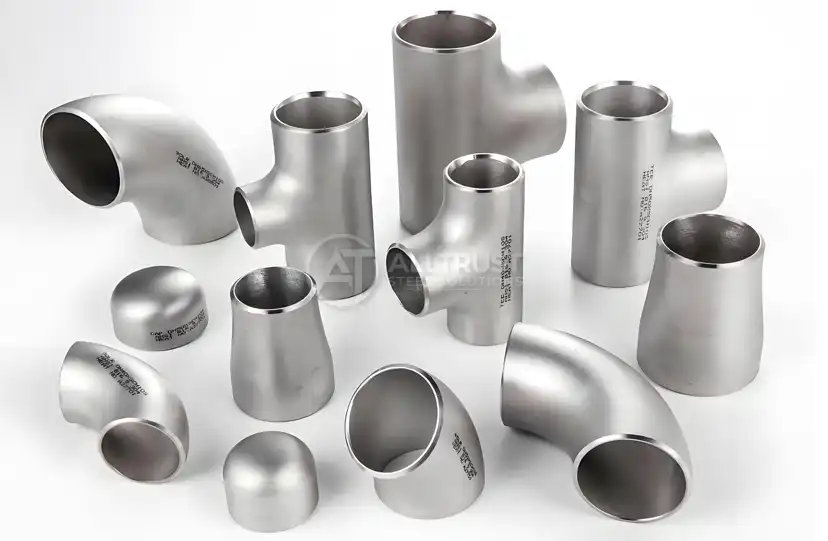
The product represents a specialized wrought austenitic stainless steel fitting designed to connect pipes of differing diameters while maintaining one perfectly flat side. This novel design solves serious hydraulic problems in horizontal pipe systems.
In the concentric reducers the pipe gradually tapers down in the middle, but the eccentric design maintains the top or bottom edge in line. Installed flat-side-up, it eliminates gas pocket build-up which causes fatal pump cavitation. Bottom flat installations are condensate return systems with full liquid drainage guaranteed.
Our production method combines precise cold rolling and innovative asymmetric die pressing technology. The method generates the needed offset geometry for effective flow control while producing a uniform wall thickness distribution.
Each fitting undergoes whole body solution annealing at regulated temperatures of 1040°C to 1150°C. The rapid water quenching leaves the austenitic microstructure in place, removing any residual forming stresses that might adversely affect long-term structural integrity.
Material composition and resistance to corrosion
The dual-certified WP316/WP316L grade provides excellent performance due to its precisely adjusted chemical makeup. The protective oxide layer is formed by the chromium level of 16-18%. The austenitic structure is stabilised by 10-14% Ni contents across broad temperature range.
Most importantly, the 2-3% molybdenum concentration gives excellent resistance to pitting and crevice corrosion in chloride rich conditions. The “L” mark guaranties maximum carbon content <0.030% which totally precludes the formation of hazardous carbide precipitation during welding operations.
This extra-low carbon profile ensures your product remains fully corrosion resistant even in heat-affected weld zones. You get the mechanical strength of standard 316 and the weldability of 316L in a single certified component.
Our rigorous PMI testing verifies that every batch meets these precise chemistry requirements. You receive complete material traceability from certified steel mills through final fitting production.
Technical Specifications and Dimensional Standards
| Specification Item | Details |
|---|---|
| Manufacturing Standard | ASTM A403 / ASME SA403 / ASME B16.9 / EN 10253-4 |
| Material Grade | WP316 / WP316L (UNS S31600 / S31603) Dual Certified |
| Construction Type | Seamless (WP-S) / Welded (WP-W) with 100% RT |
| Size Range | 1/2" to 48" (Big End to Small End Reduction) |
| Wall Thickness | SCH 5S / 10S / 40S / 80S / 160 / XXS |
| End Preparation | Beveled Ends (BE) per ASME B16.25 |
| Heat Treatment | Solution Annealed and Rapid Water Quenched |
| Surface Finish | Pickled & Passivated / Shot Blasted / Satin / Mirror |
| Testing Protocol | PMI / UT / RT / PT / IGC (ASTM A262 Practice E) |
| Quality Certification | EN 10204 3.1 & 3.2 MTC / ISO 9001:2015 / PED |
| Inspection Support | SGS / BV / TUV / DNV / ABS Third-Party Available |
Precision Manufacturing Process
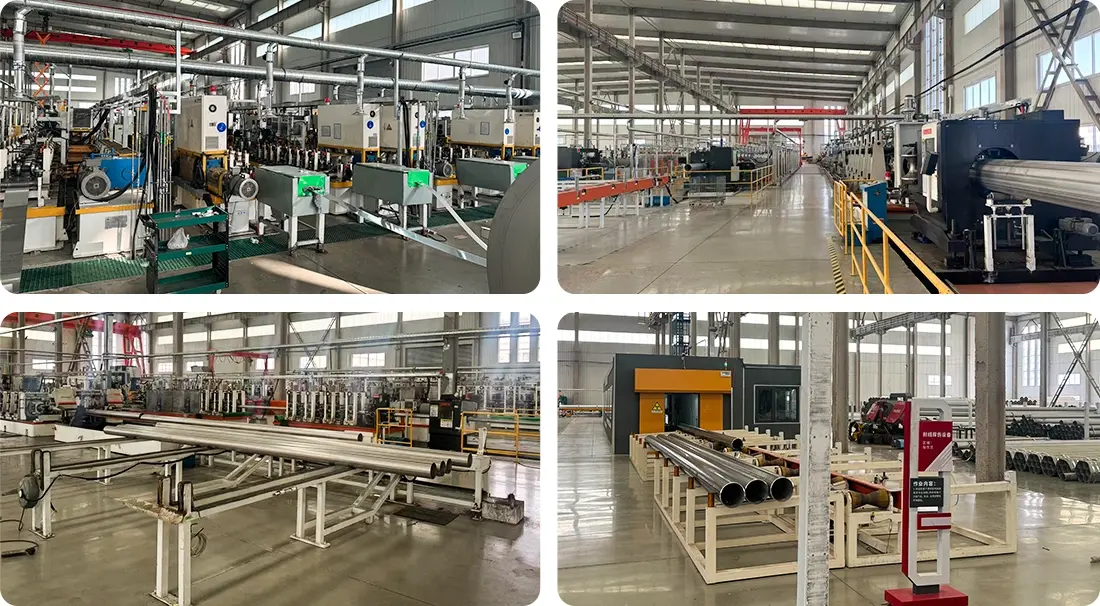
Our production facility employs a four-stage manufacturing protocol to ensure dimensional accuracy and metallurgical consistency. Raw material selection begins with spectrographic verification of chromium, nickel, and molybdenum content from ISO-certified steel mills.
Advanced eccentric die pressing creates the asymmetric profile while maintaining precise wall thickness control. Computer-guided cold rolling achieves the exact dimensional tolerances required for seamless field installation.
High-precision end face machining prepares weld bevels to exacting angles. This preparation ensures complete penetration when you join the product to your piping system using standard GTAW or SMAW procedures.
All surface oxides generated after heat treatment are removed using chemical descaling pickle baths. A final passivation treatment optimises the protective chromium oxide layer to maximise the corrosion resistance from the time your fitting is installed.
Comprehensive Quality Control Protocol
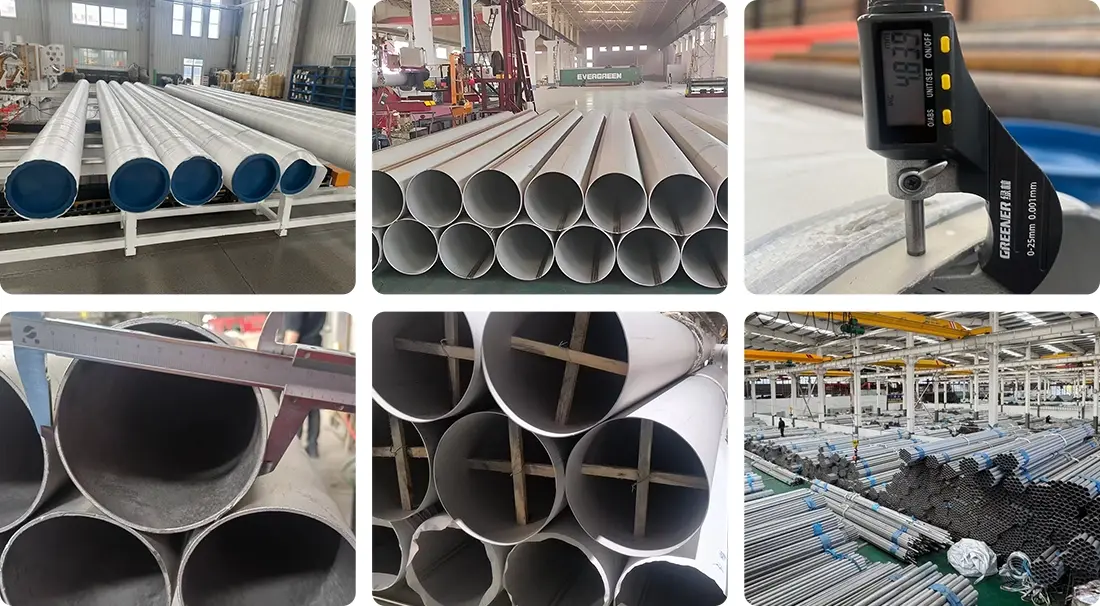
All products sent from our facilities are subject to required multi-stage inspection processes. Dimensional verification ensures compliance with ASME B16.9 tolerances for end-to-end length, outer diameter and wall thickness measurements.
We examine longitudinal seams of welded structure (WP-W grade) using 100% radiography. The X-ray inspection is used to find any internal discontinuities for total weld integrity before the fitting is in service.
Ultrasonic thickness measuring confirms that the minimum wall requirements are not violated by the forming activities. The liquid penetrant testing method is able to detect any surface breaking faults which might induce stress corrosion cracking.
Intergranular corrosion testing under ASTM A262 Practice E is a validation of our solution annealing method. This destructive test on sample pieces of each manufacturing lot verifies resistance to sensitisation that might be incurred during field welding.
Critical Application Scenarios
Chemical Processing and Fertiliser Production Your demanding process settings need materials that can endure intense sulfuric acid, phosphoric acid and acetic acid. The ASTM A403 WP316 WP316L Eccentric Reducer provides long lasting structural integrity in applications where ordinary 304 fittings are subject to fast pitting failure.
Offshore Oil and Gas Platforms Marine spray and saline immersion relentlessly assault seawater cooling systems and firewater distribution networks with chlorides. In these harsh offshore environments, our molybdenum-enhanced fittings resist crevice corrosion.
Pharmaceutical and Biotech Manufacturing Water-for-Injection (WFI) systems need to be completely drainable to avoid microbial development in stagnant areas. The unique design prevents"dead legs"while providing seamless flow transitions over complicated modular process skids.
Installation Best Practices
Proper orientation maximizes the hydraulic advantages of your eccentric reducer. For horizontal pump suction lines handling liquids, install with the flat side positioned at the top. This configuration prevents air accumulation that causes impeller cavitation damage.
In gravity drainage applications or condensate return systems, position the flat side at the bottom. This orientation ensures complete liquid evacuation, preventing corrosion from stagnant pooling.
Maintain adequate support on both sides of the reducer to prevent stress concentration. The offset geometry creates asymmetric weight distribution that requires consideration during pipe hanger placement.
Use compatible filler metals when welding. ER316L electrodes or wire provide matching corrosion resistance without requiring post-weld heat treatment. Our beveled ends facilitate complete penetration using standard GTAW root passes followed by SMAW fill and cap layers.
Packaging and Global Logistics
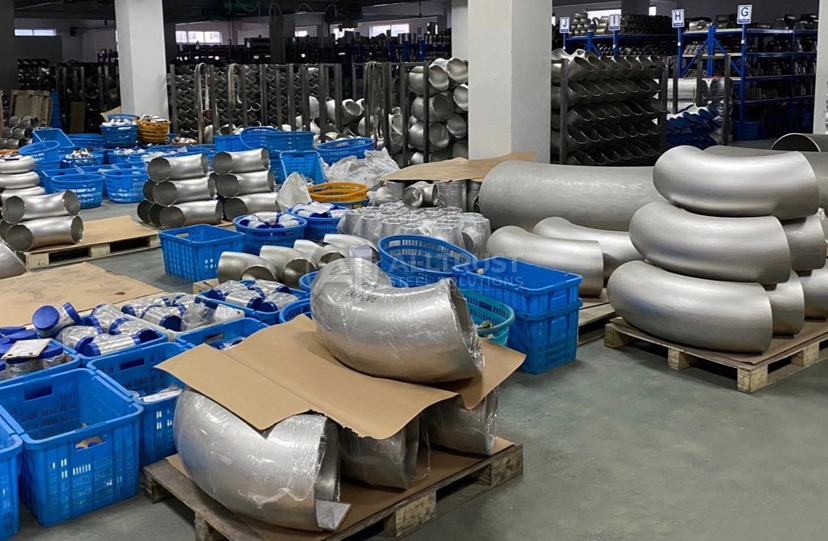
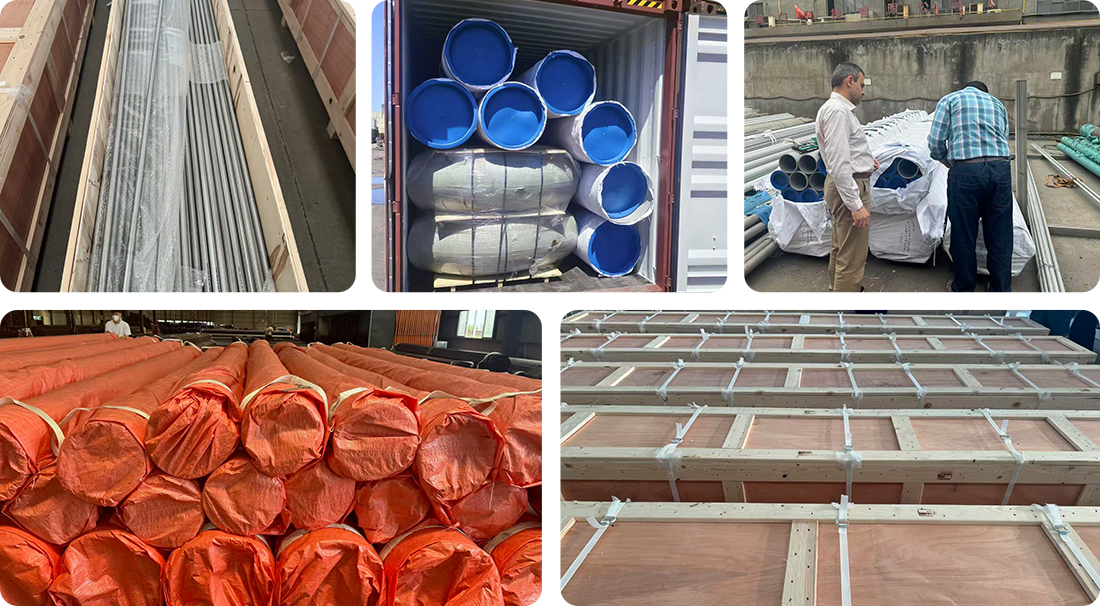
We protect your investment through comprehensive export packaging protocols. Each fitting receives individual cellophane wrapping to prevent surface scratches during handling and transportation.
Expanded foam spacers separate individual pieces within sturdy plywood crates. Moisture-proof linings guard against humidity exposure during ocean freight. Hard plastic face protectors shield the precisely machined weld bevels from mechanical impact.
Our strategic position near the ports of Shanghai, Tianjin and Qingdao allows us to load containers efficiently and at affordable freight costs. We support FOB, CFR, CIF, DDP trading term to meet your purchase needs.
You may combine product orders with related pipe fittings, flanges and valves with mixed loading options. It minimises your transport expenses and guaranties 100% compatibility of materials.
FAQ
Q:Why does this dual-certified product deliver elite crevice corrosion defense inside horizontal lines?
A:Featuring an extra-low carbon profile combined with robust molybdenum integration, this eccentric reducer completely eliminates weld area sensitization while ensuring elite corrosion defense along severe marine horizontal flow layouts.
Q:How does the eccentric flat-side geometry of this grade respond under severe mechanical operating stress variables?
A:The press forged asymmetric wall structure provides robust load-bearing safety parameters and excellent structural ductility, preventing structural center deflection or pipeline sagging under heavy chemical fluid volume loads.
Q:What strict non-destructive criteria must the eccentric reducer body successfully clear before clearing factory bounds?
A:The entire batch undergoes 100% mandatory non-destructive testing, passing through automated internal eddy current diagnostic mapping, liquid penetrant checks (PT), and precise volumetric thickness scans.
Q:What massive dimensional customization limits can be achieved for large-bore chemical plant transitions?
A:We can manufacture custom horizontal configurations matching big-end dimensions up to 48 inches with customized reducing small-end steps, and customized exterior mechanical polishing profiles (satin or mirror).
Q:How are these eccentric reducers packaged to ensure scratch-free and rust-free arrival at the project site?
A:Each component is enveloped within protective plastic wraps, cushioned with expanded foam spacers, and safely enclosed inside robust, stackable seaworthy plywood crates fitted with moisture-proof linings and hard plastic face protectors.
Contact Us
Secure your critical piping projects with factory-direct ASTM A403 WP316 WP316L Eccentric Reducer solutions backed by complete material traceability and technical support. Contact our engineering team at info@hballtrust.com for specifications, pricing, and delivery schedules.